800T Bearing Case & Titanium Fasteners Press press view 1
Bearing Case & Titanium Alloy Fasteners · Hydraulic Press Machine

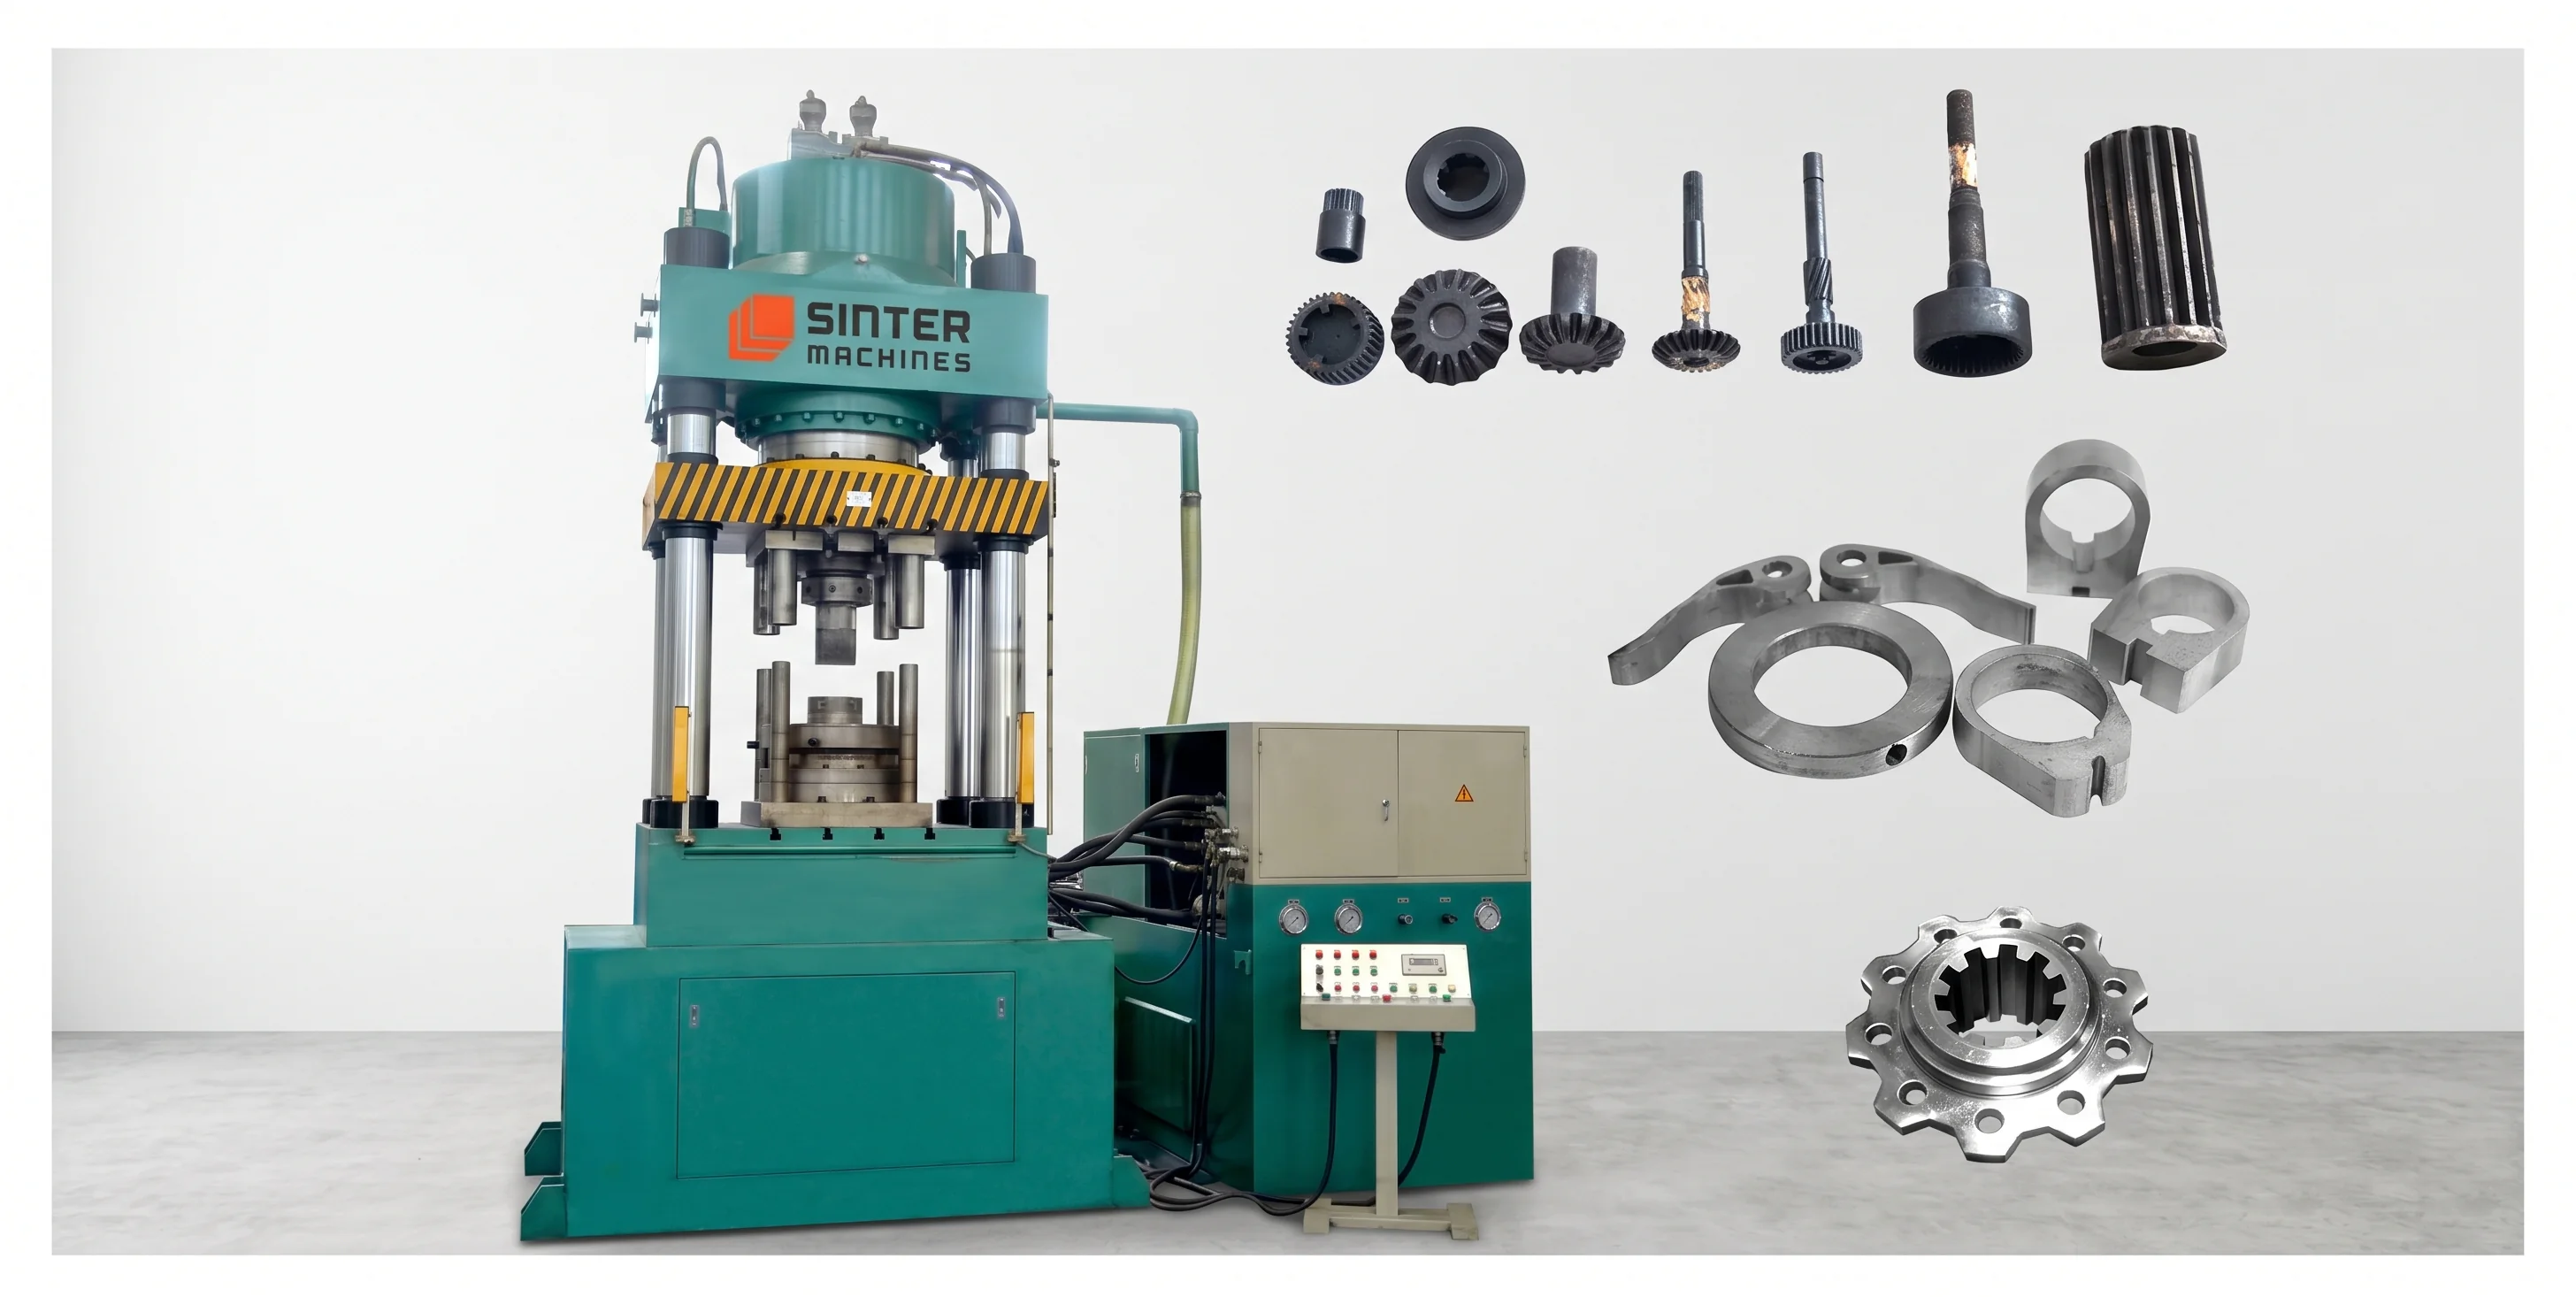
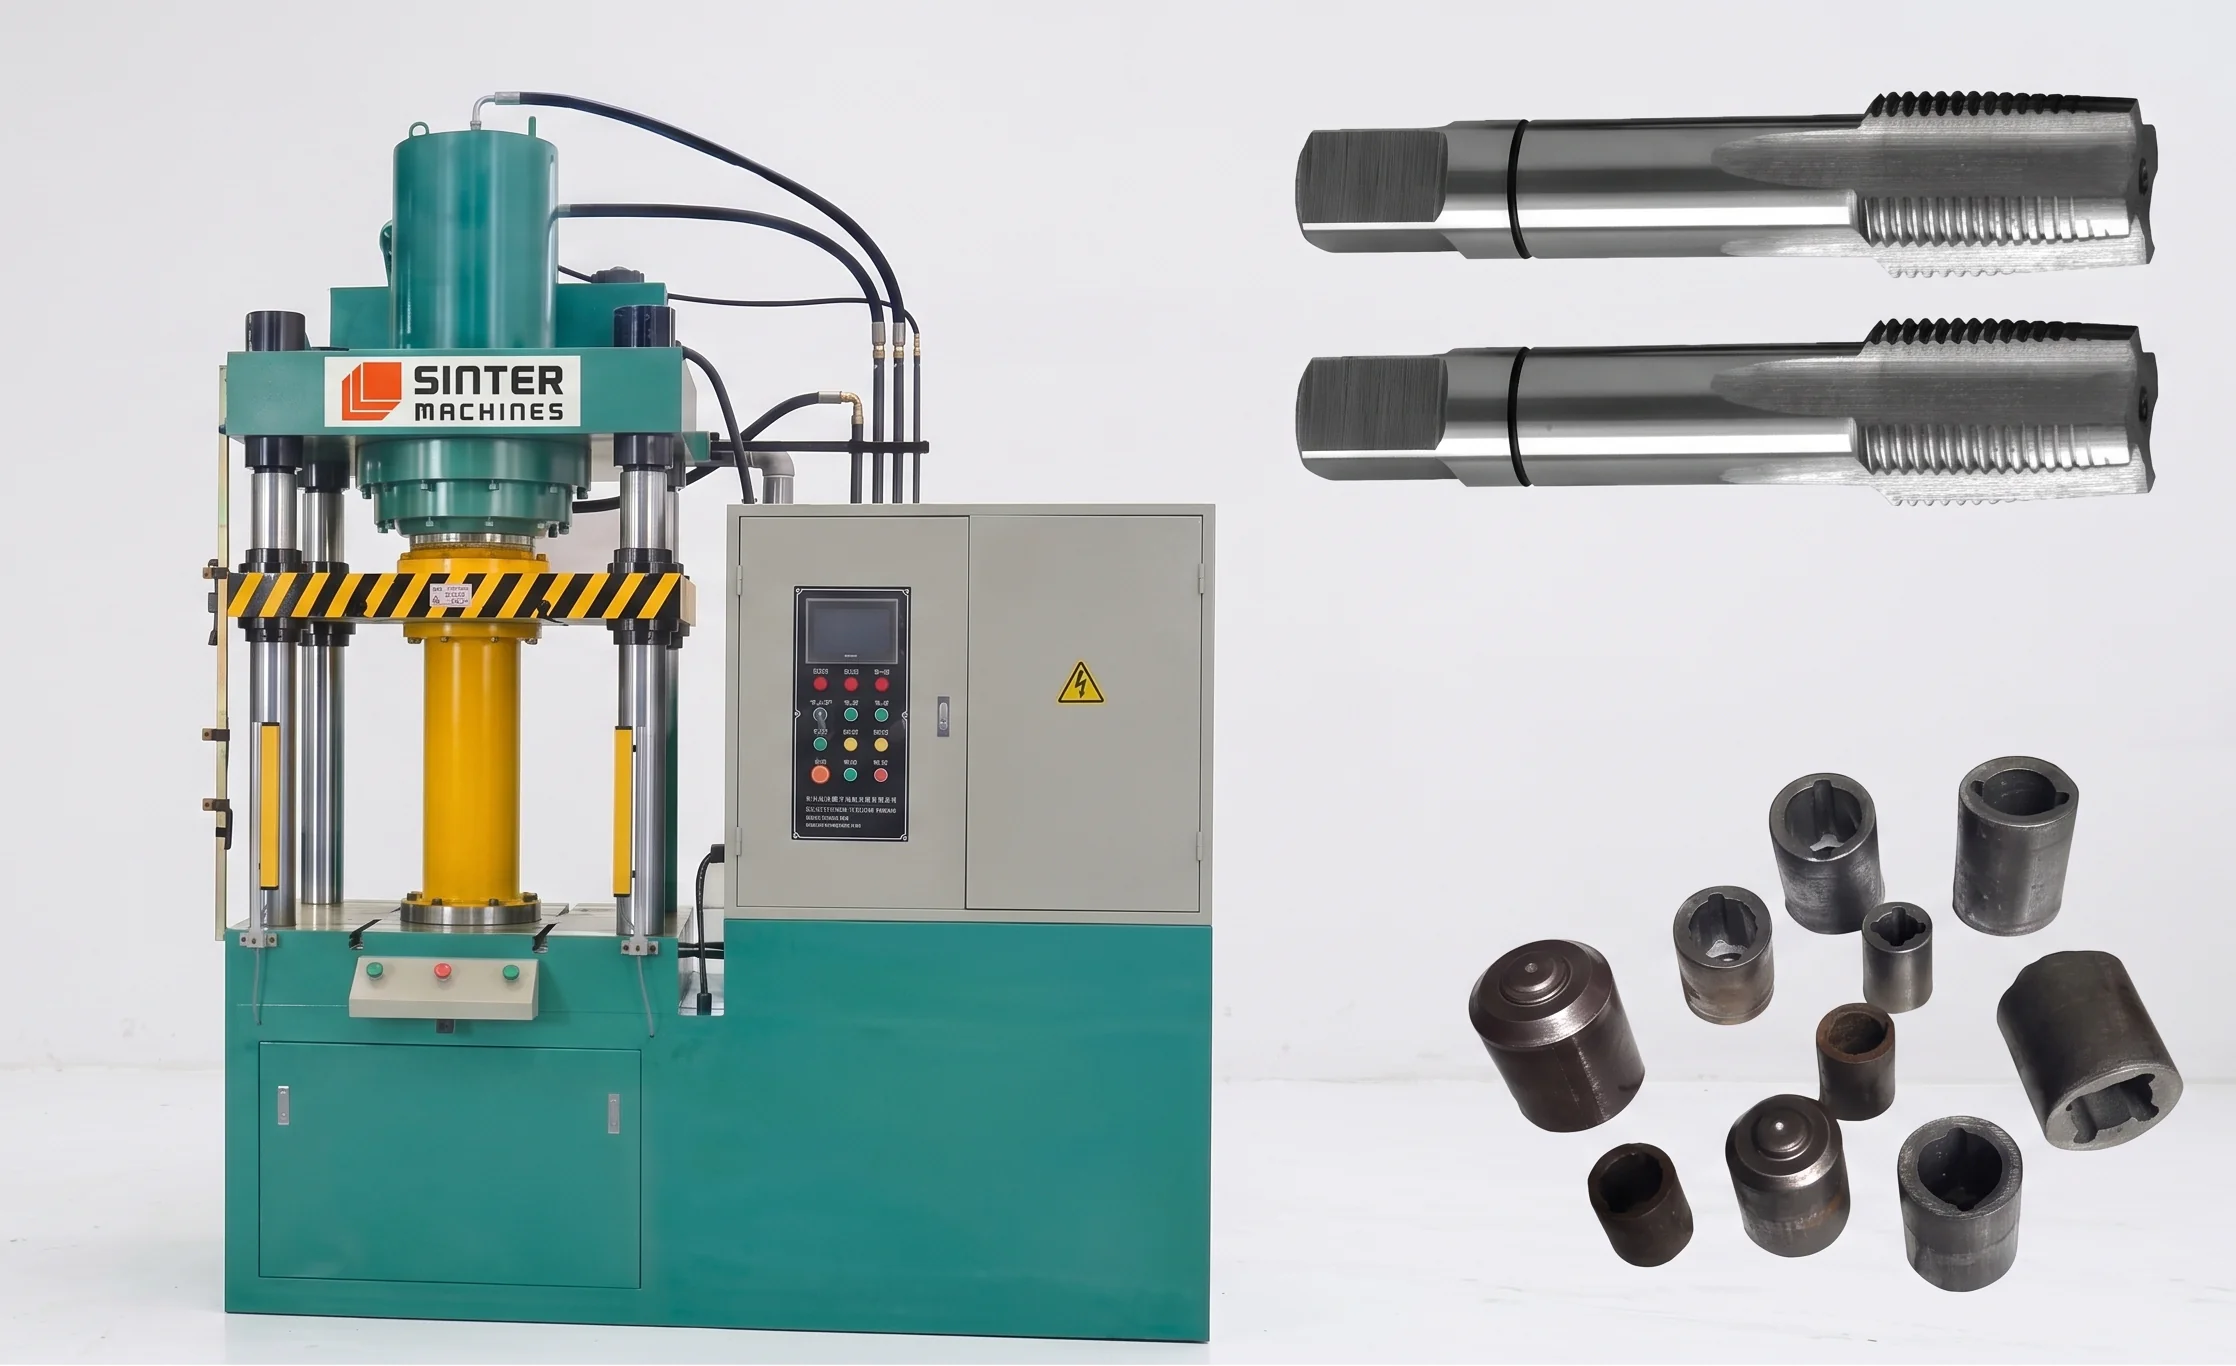
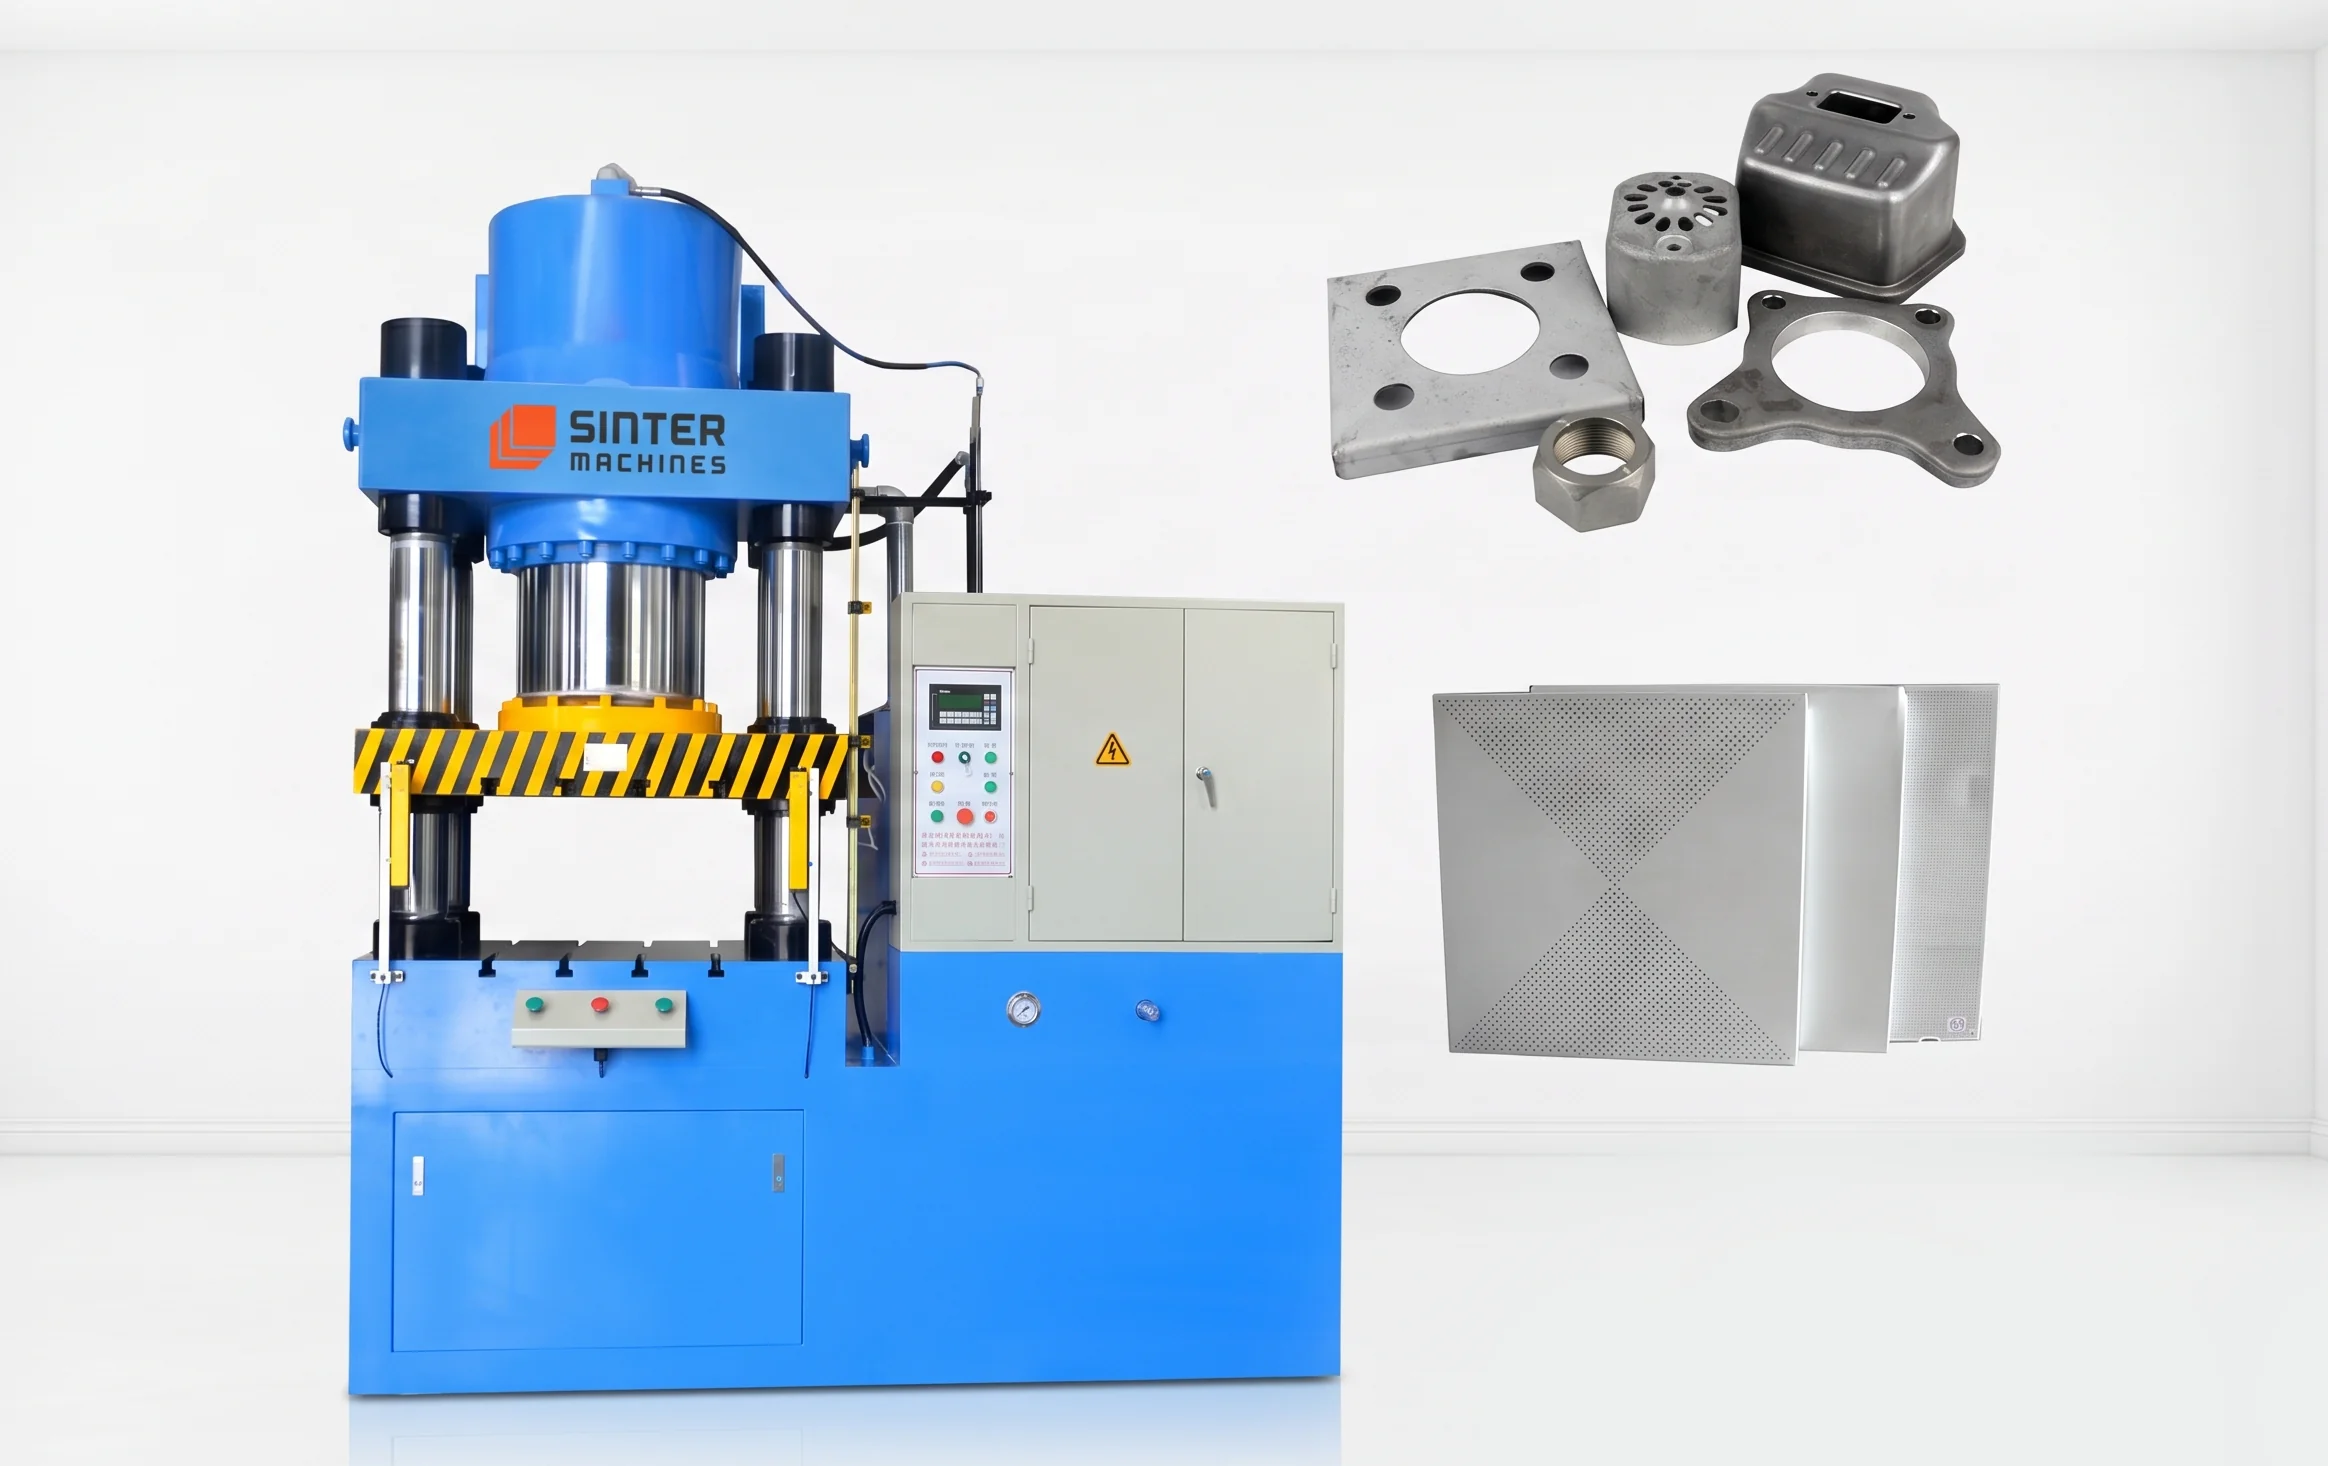
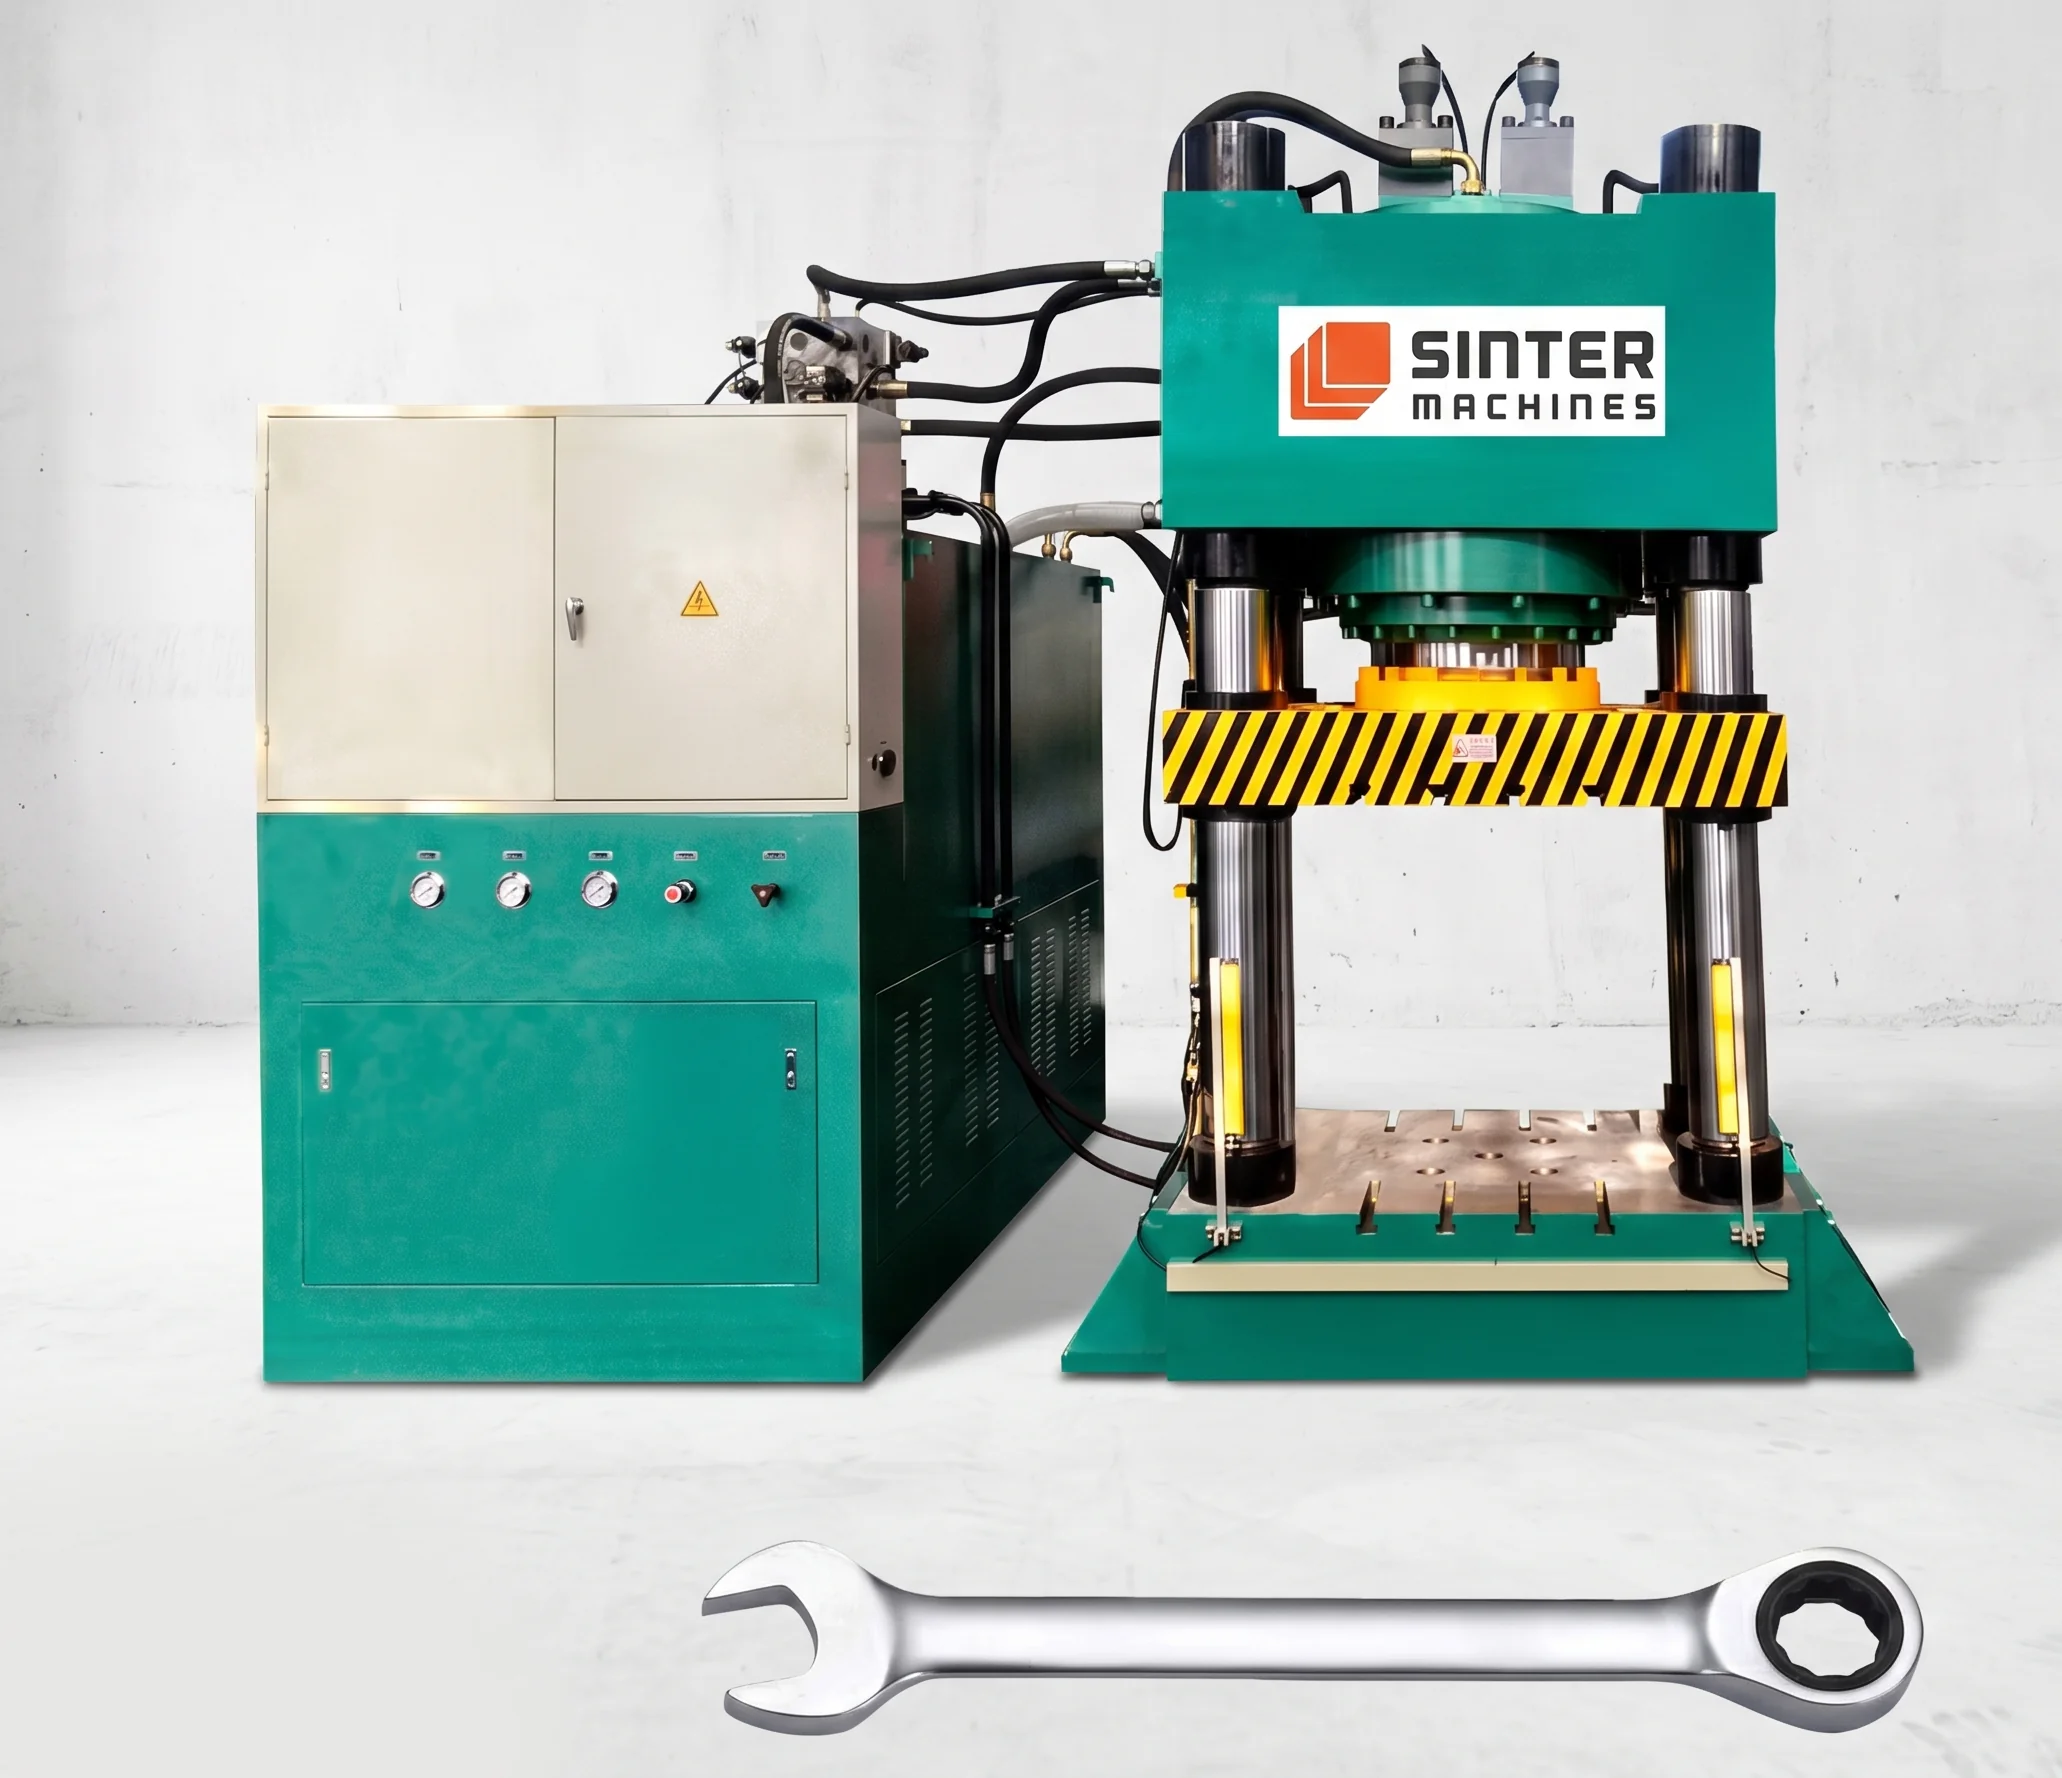
800T Four Column Hydraulic Press for Bearing Case & Titanium Alloy Fasteners

800T Rated Capacity
180 mm/s Slider Down Speed
9–18 mm/s Slider Pressing Speed
180 mm/s Slider Return Speed

01 — Press System

800T Four Column Hydraulic Press Machine

The 800-ton four-pillar hydraulic press provides a high-precision, heavy-duty industrial forming platform engineered specifically for demanding hot forging applications. This highly stable configuration satisfies global manufacturing standards within the aerospace, defense, and energy sectors where material microstructures must be flawlessly maintained.

Use Case

Manufacturing bearing cases and titanium alloy fasteners demands stable, ultra-precise tonnage application to overcome high material deformation resistance without inducing surface cracks. This press provides the necessary thermal stability, structural rigidity, and variable speed flexibility required to form complex near-net-shape geometries from sensitive high-strength alloys.

Core Applications

  • Precision closed-die hot forging and net-shape forming of high-stress industrial rotating component housings
  • High-temperature upset forging, heading, and shank extrusion processing for specialized aerospace fasteners
  • Blocker and finisher die sequence forming for medium-weight structural engine and drivetrain brackets

Material

  • Premium aerospace-grade titanium alloys including titanium 6Al-4V and beta-stabilized titanium matrices
  • High-strength chrome-nickel structural steels, specialized bearing steels, and superalloys like Inconel

Typical Products Processed

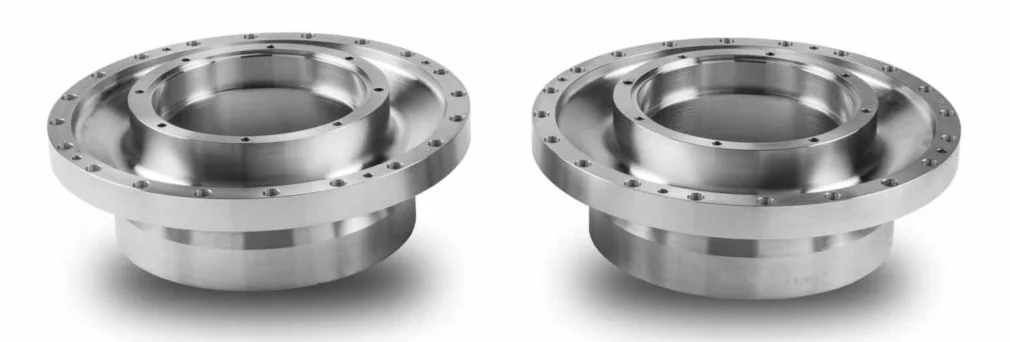
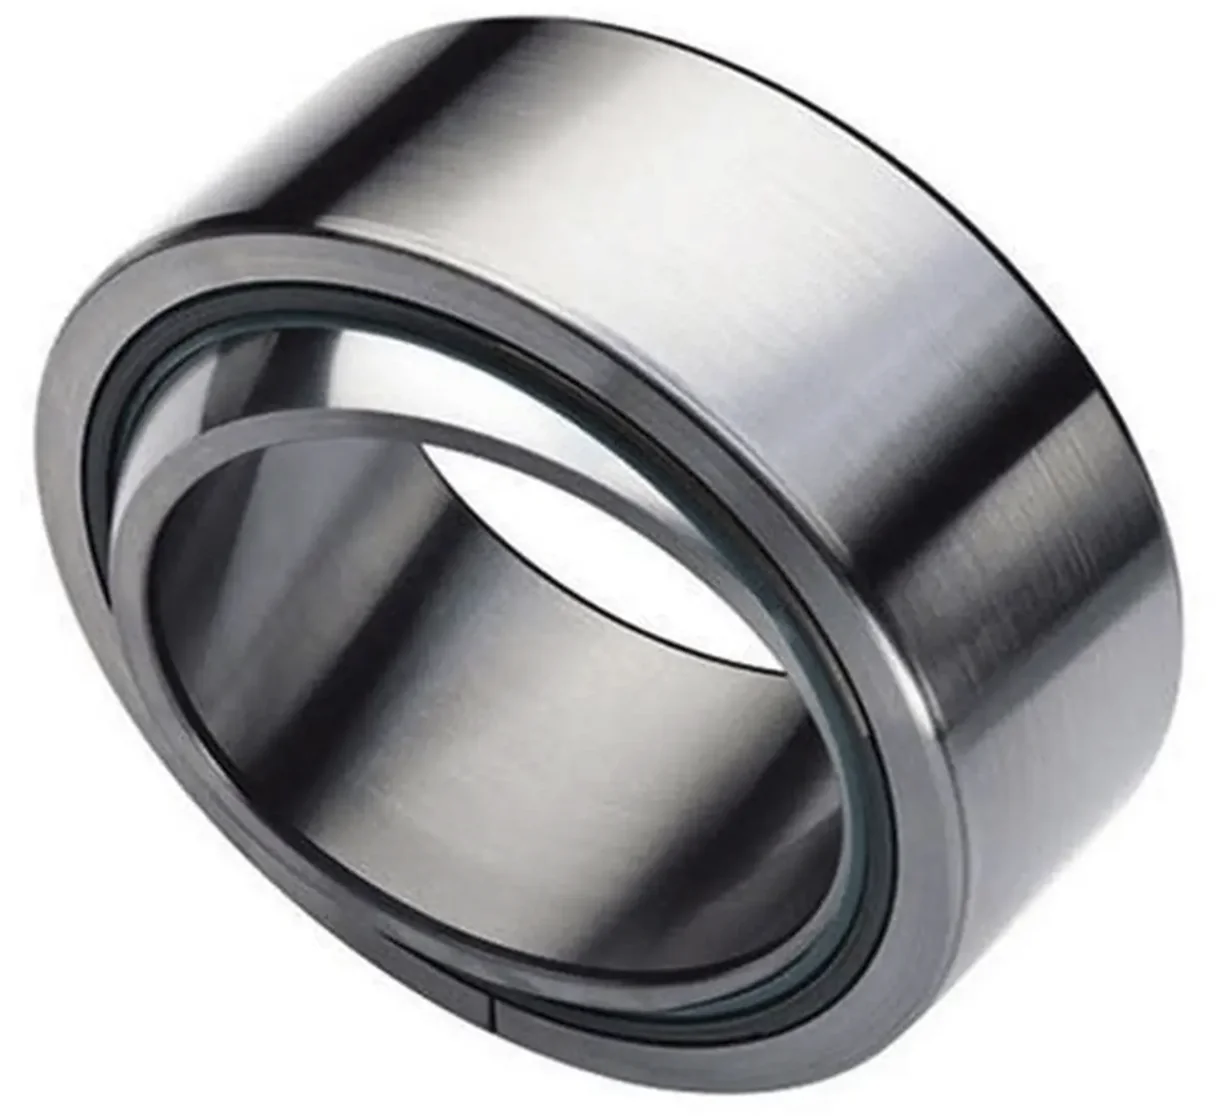
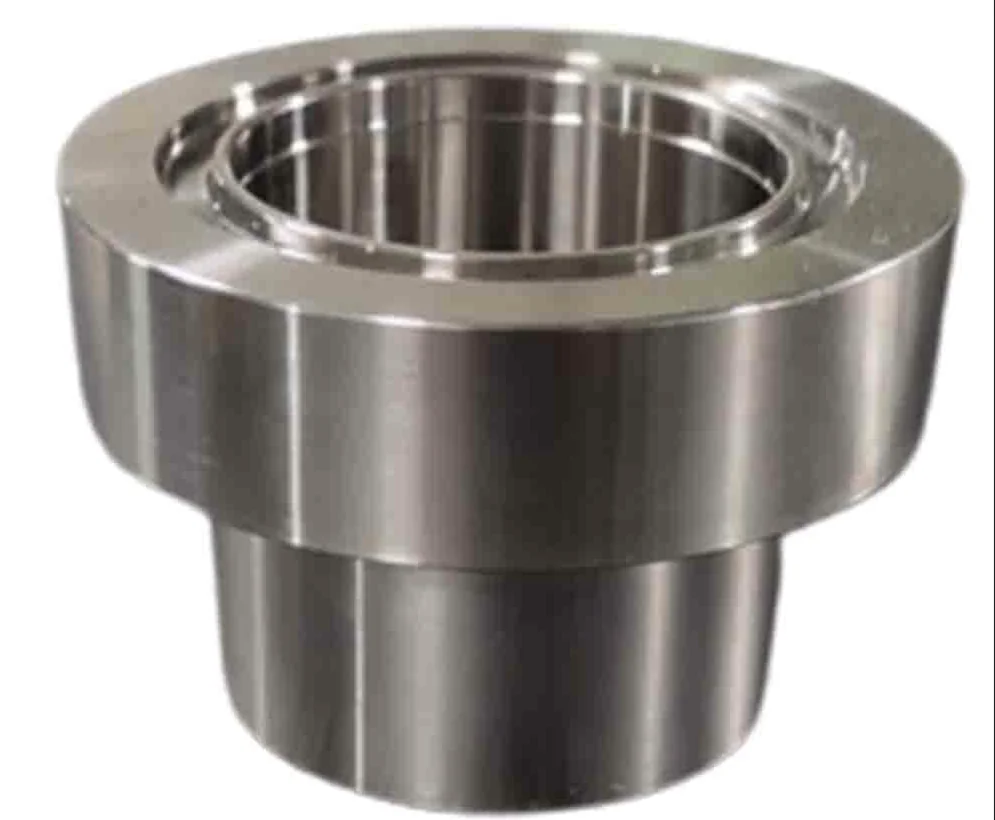
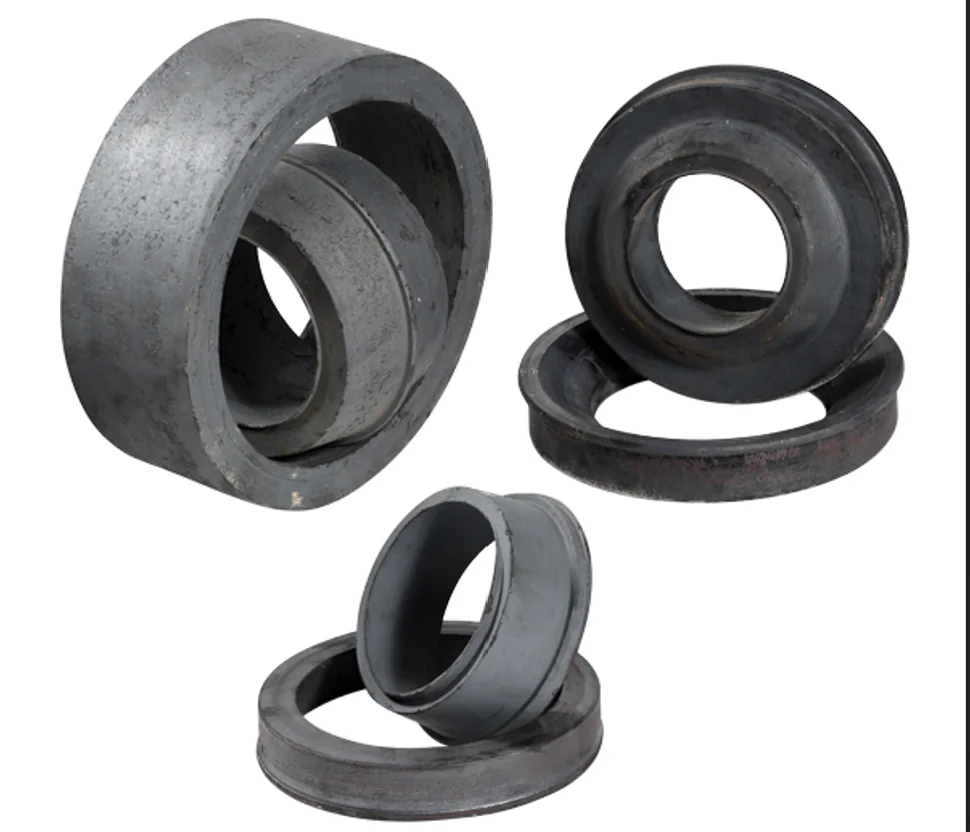
  • Heavy-duty industrial bearing cases, flanged hubs, split bearing housings, and turbine rotor rings
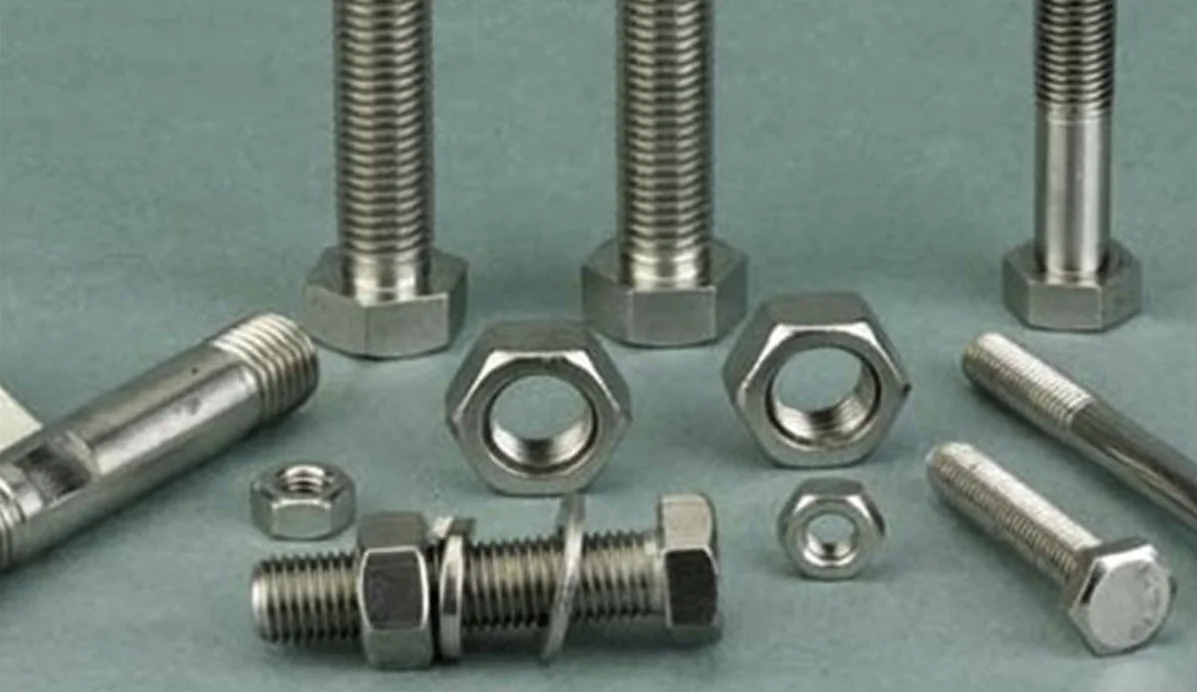
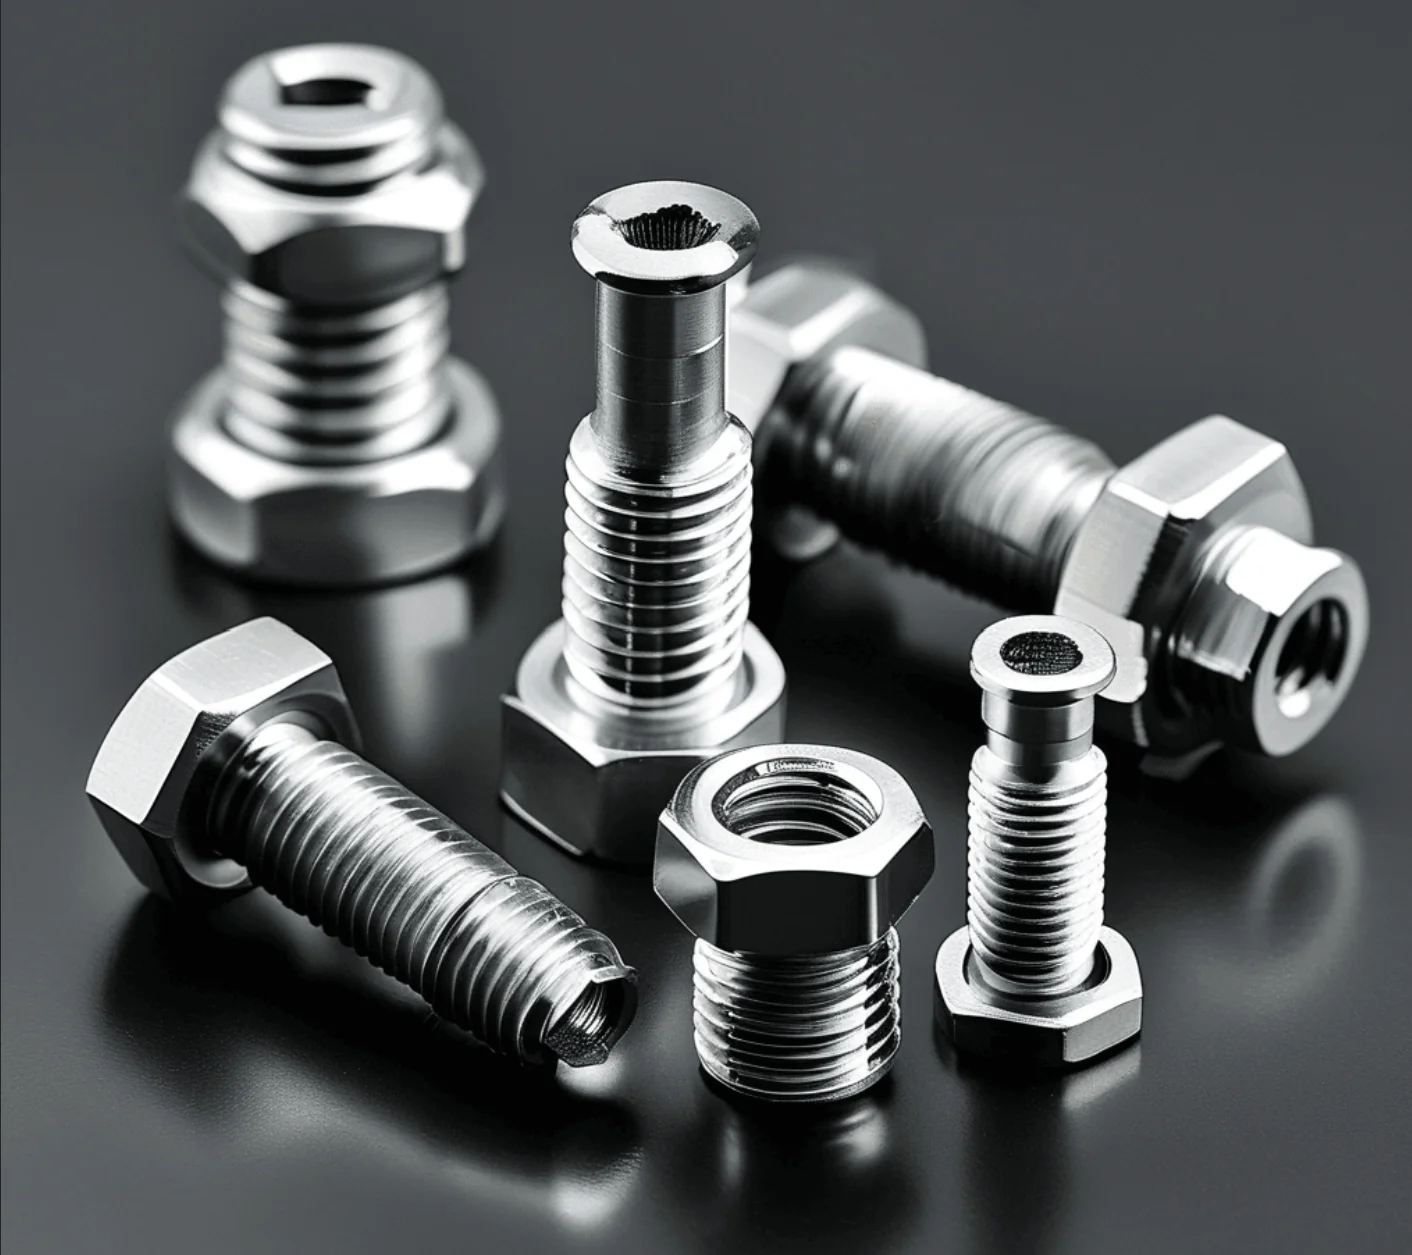
  • High-tensile aerospace engine bolts, critical airframe shear pins, 12-point nuts, and military-grade structural fasteners

Key Functions

  • Multi-stage velocity profiling to accommodate the narrow thermal working window and strain-rate sensitivity of titanium
  • High-tonnage hydraulic knockout systems integrated into both the bed and slide to ensure seamless part extraction

Why 800 Ton Hydraulic Press?

  • Delivers the exact tonnage threshold needed to forge medium-weight dense alloy blanks without causing machine frame deflection
  • Rigid four-pillar architecture maintains perfect platen parallelism under extreme thermal stress, eliminating asymmetrical tooling wear

02 — Technical Specifications

SM 800 HP – HYDRAULIC PRESS MACHINE COMPLETE TECHNICAL DATA

The SM 800 HP hydraulic press delivers highly regulated tonnage and extreme structural rigidity engineered for the thermal demands of titanium and steel forging. Its closed-loop servo system and precision platen parallelism guarantee uniform material deformation and exceptional near-net-shape accuracy.

Capacity

  • Maximum continuous hot forging compression force capacity of 800 metric tons
  • Uniform force distribution rating across the full active tool bed area

Structural Design

  • Continuous precision hot forging layout built to resist high cyclical thermal shock
  • Strict load structural safety factor rating equal to or greater than 1.30
  • Maximum elastic frame deflection under full mechanical load restricted to 0.08 to 0.10 mm

Frame Type

  • Four pillar guided press configuration utilizing precision aligned heavy steel columns
  • Heavy fabricated structural steel frame assembly fully stress relieved after welding

Hydraulic System

  • Variable displacement axial piston pump delivery assembly with energy saving control
  • Closed loop electronic force and position sensor feedback tracking mechanisms
  • Integrated multi step forging mode system with programmable dwell time capability
  • Controlled pressure ramping sequences engineered for advanced die and material protection

Main Ram Stroke

  • High precision double acting guided main forging cylinder ram construction
  • Adjustable stroke controlled hot forging compression distance of 700 to 1100 mm

Working Hydraulic Pressure

  • Standard maximum continuous operating system fluid pressure of 30 to 32 MPa
  • Peak safety valve circuit pressure calibration threshold limit of 35 MPa

Daylight Gap

  • Maximum open vertical daylight window working clearance of 1300 to 1700 mm
  • Precision platen parallelism variance maintained within 0.02 to 0.03 mm per 300 mm

Approach Speed

  • Accelerated downward slide rapid advance travel speed of 280 mm/Sec
  • Soft touch tool contact deceleration control velocity of 15 mm/Sec

Pressing / Drawing Speed

  • Precise strain rate sensitive titanium alloy press speed of 5 to 25 mm/Sec
  • Constant force high pressure metal squeezing velocity of 40 mm/Sec

Return Speed

  • High speed upward ram extraction retraction travel speed of 240 mm/Sec
  • High frequency automated fluid decompression valve cycling system operation

Bed / Platen Size Platen

  • Standard structural upper and lower platen width and depth of 1100 by 1100 mm
  • Optional heavy duty expanded platen width and depth of 1300 by 1300 mm

Columns

  • Total guide column layout consisting of 4 high strength solid steel pillars
  • Solid alloy steel guide column shaft diameter of 160 to 200 mm
  • Hardened hard chromed and precision ground column outer surface treatment

Working Envelope

  • Total standard internal clear horizontal workspace area of 1100 by 1100 mm
  • Maximum allowable upper die tool assembly mass weight capacity of 6000 kg

Control System

  • Dedicated industrial programmable logic controller paired with a central processor
  • Real time data visualization of active forging force versus stroke curve profiles
  • Digital bottom dead center accuracy tracking accurate down to 0.02 mm
  • Automated digital die load monitoring paired with lifetime cycle counter registries

Main Motor Power

  • Primary high efficiency electric pump drive motor rating of 90 kW
  • Dedicated secondary hydraulic oil cooling loop motor capacity of 11 kW

Valves & Hydraulics

  • High precision servo hydraulic and proportional pressure control valve manifolds
  • Fast acting main cylinder gravity oil pre fill valve block assembly

Automation

  • Integrated digital communication ports for robotic billet handling manipulator arms
  • Automated diagnostic fault display software tracking data storage for 5000 hours

Safety Features

  • Safety integrity level rated digital programmable logic controller architecture
  • Multi channel infrared safety light curtains paired with optical area scanners
  • Automated hydraulic loop pressure relief and thermal overload safety valves
  • Dual channel emergency stop circuit loops connected to independent dump valves

SM 800 HP — Model Specifications

  • Nominal Force: 8000 KN
  • Maximum Hydraulic Pressure: 25 MPa
  • Max Opening Height of the Slider: 1500 mm
  • Max Stroke of the Slider: 900 mm
  • Effective Bed Size: 1600 × 1600 mm
  • Slider Down Speed: 180 mm/s
  • Slider Pressing Speed: 9–18 mm/s
  • Slider Return Speed: 180 mm/s
  • Ejector Cylinder Nominal Force: 600 KN
  • Stroke of the Ejection Cylinder: 300 mm
Production Case Study

Hot Forging Bearing Case & Titanium Alloy Fasteners Production Line

15 to 90mmBillet/Blank
Thick900–1,150 °C Temperature Range
10–20 secondsCycle time
300 to 600 PartsOutput/Hout
Grain flow optimized perfectly
Structural cracking eliminated completely
Near net dimensions achieved
Die wear minimized significantly
Titanium alpha case prevented
Component scrap rates minimized
Machining time slashed drastically
03 — Die / Mold System

Precision Hot Forging Bearing Case & Titanium

Alloy Fasteners Die Mold Engineering

This precision tooling system utilizes specialized hot work dies engineered to manage the narrow thermal windows and high flow resistance of advanced aerospace alloys. Its robust structural architecture resists intense heat transfer and cyclical micro-abrasion, ensuring long-term dimensional stability under continuous industrial operation.

Technical Specifications (Tooling)

Die Type

  • Precision closed die hot upset forging tool set optimized for high temperature heading
  • Multi cavity progressive insert layout engineered for net shape industrial production

Die Materials

  • Premium grade high tungsten alloy hot work tool steel matrix structure
  • Vacuum melted cobalt base superalloy inserts positioned in high wear zones

Tool Configuration & Construction

  • Pre stressed shrink ring container layout built to handle immense lateral forces
  • Quick change modular die block architecture designed to minimize factory downtime

Key Tooling Features

  • Integrated high force pneumatic knockout rods to ensure clean component ejection
  • Internal thermal couples linked with localized induction heating block assemblies

Alignment Accuracy

  • Die halves axial mismatch deviation held strictly below a limit of 0.100 mm
  • Guide pillar location concentricity tolerance restricted within a limit of 0.020 mm

Process Materials

  • Aerospace grade titanium six aluminum four vanadium alloy structural rod blanks
  • High strength chromium nickel base superalloys and premium bearing steel stocks

Surface Finish

  • Internal die cavity profiles precision polished down to Ra 0.40 microns
  • Advanced physical vapor deposition titanium aluminum nitride coating at 0.006 mm thickness

Tool Life

  • Expected production span of 8000 cycles before mandatory die cavity reconditioning
  • Total structural tooling lifespan capacity reaching 60000 production cycles
Case Study (Die Performance)

Precision Hot Forging Bearing Case & Titanium Alloy Fasteners Die Mold

Tungsten-AlloyDie Material
54-60 HRCHardness
Vacuum Gas HardeningHeat Treatment
Thermal fatigue cracking eliminated
Micro-abrasive wear reduced drastically
Material adhesion prevented completely
Component dimensions held strictly
Die life extended significantly
Production downtime minimized fully
Post-forge machining cut substantially

04 — Product Application

Where Precision Hot Forging Bearing Case & Titanium Alloy Fasteners Are Used

Precision hot forged bearing cases and titanium alloy fasteners serve as critical, high-strength joining and containment components within extreme-environment structural assemblies. These specialized components deliver maximum fatigue strength and heat resistance, preventing structural failure under immense cyclical stress, pressure loads, and rapid thermal fluctuations.

Industry Applications

These ultra-precise forgings are indispensable across the global aerospace defence, commercial aviation, deep-sea marine engineering, and high-performance automotive industries. Their superior material density and tight dimensional tolerances enable global manufacturers to achieve stringent weight-reduction goals, maximize energy efficiency, and meet extreme operating lifetime mandates.

Commercial and Military Aircraft Airframes

Ultra-strong titanium fasteners secure high-stress structural joints, wing spars, and landing gear attachment brackets across modern aviation platforms. Their high strength-to-weight ratio and exceptional corrosion resistance reduce total aircraft empty weight while guaranteeing absolute safety during high-stress flight maneuvers.

Aerospace Jet Engines and Gas Turbines

Precision forged bearing cases and high-temperature alloy fasteners enclose and stabilize the high-speed main rotor shafts inside jet engines. The flawless metallurgical integrity prevents structural deformation at extreme operating velocities, keeping vital compressor and turbine blades perfectly aligned.

Automotive Drivetrains and Electric Vehicles

High-performance bearing housings and heavy-duty hub fasteners secure the rotating assemblies inside advanced transmission systems and electric drive units. The optimized microstructural grain flow manages high torque outputs smoothly, ensuring quiet vehicle operation and long-term drivetrain reliability.

Deep-Sea Oil, Gas, and Marine Propulsion

Corrosion-resistant titanium bolts and heavy bearing cases anchor underwater drilling manifolds, marine prop shafts, and deep-sea exploration equipment. The specialized metal structure completely resists aggressive saltwater pitting and extreme subsea pressures, avoiding catastrophic fluid leaks or structural failures.

Finished Product Gallery

05 — Key Advantages

Why Choose the 800-Ton Sinter Hydraulic Press

The 800-Ton Sinter Hydraulic Press provides precise stroke velocity control and highly stable frame rigidity designed specifically for the narrow forging windows of exotic alloys. Its advanced closed-loop tonnage regulation and outstanding platen parallelism prevent structural cracking, optimizing material yields and ensuring exceptional component repeatability.

Technical & Commercial Benefits

01

Programmable Strain-Rate Velocity Profiling System

The advanced hydraulic control system dynamically modifies slide speed down to milliseconds during active material deformation to match metallurgical flow rates. This precise slow-deceleration control prevents temperature spikes and localized cracking in strain-sensitive titanium alloys, ensuring perfect structural density.

02

Ultra-Precise Bottom Dead Center Position Accuracy

High-resolution linear transducers track vertical platen travel within a tight fraction of a millimeter to establish repeatable stroke endings. Achieving this precise net-shape height straight out of the press bed dramatically cuts down expensive post-forge CNC machining operations.

03

Rigid Four-Pillar Construction Minimizing Elastic Deflection

The induction-hardened solid columns and heavy stress-relieved plates maintain parallel alignment even when handling eccentric multi-stage tool configurations. Eliminating frame tilting guarantees identical wall thicknesses across bearing cases, preventing asymmetrical tool wear and premature die failure.

04

Synchronized Dual-Acting High-Force Ejector Systems

Integrated bottom and top hydraulic knockout circuits deliver powerful, rapid upward mechanical forces to clear finished parts from tight cavities instantly. Minimizing the time glowing billets stay inside the mold drops heat transfer, protecting the tool steel from thermal fatigue cracking.

05

Substantial Reductions in Raw Material Scrap Costs

The tight dimensional repeatability allows aerospace-grade titanium rods and bearing steel blanks to be sized close to finished dimensions. Maximizing near-net-shape accuracy slashes waste on expensive superalloy raw stocks, directly lowering net material overhead per factory production batch.

06

Rapid Decompression Control for Shorter Cycle Times

Specialized fast-acting pre-fill circuits bleed off massive internal hydraulic pressure smoothly to compress total slide return travel times. Accelerating these processing cycles raises hourly part throughput on automated lines while lowering net electrical consumption per forged unit.