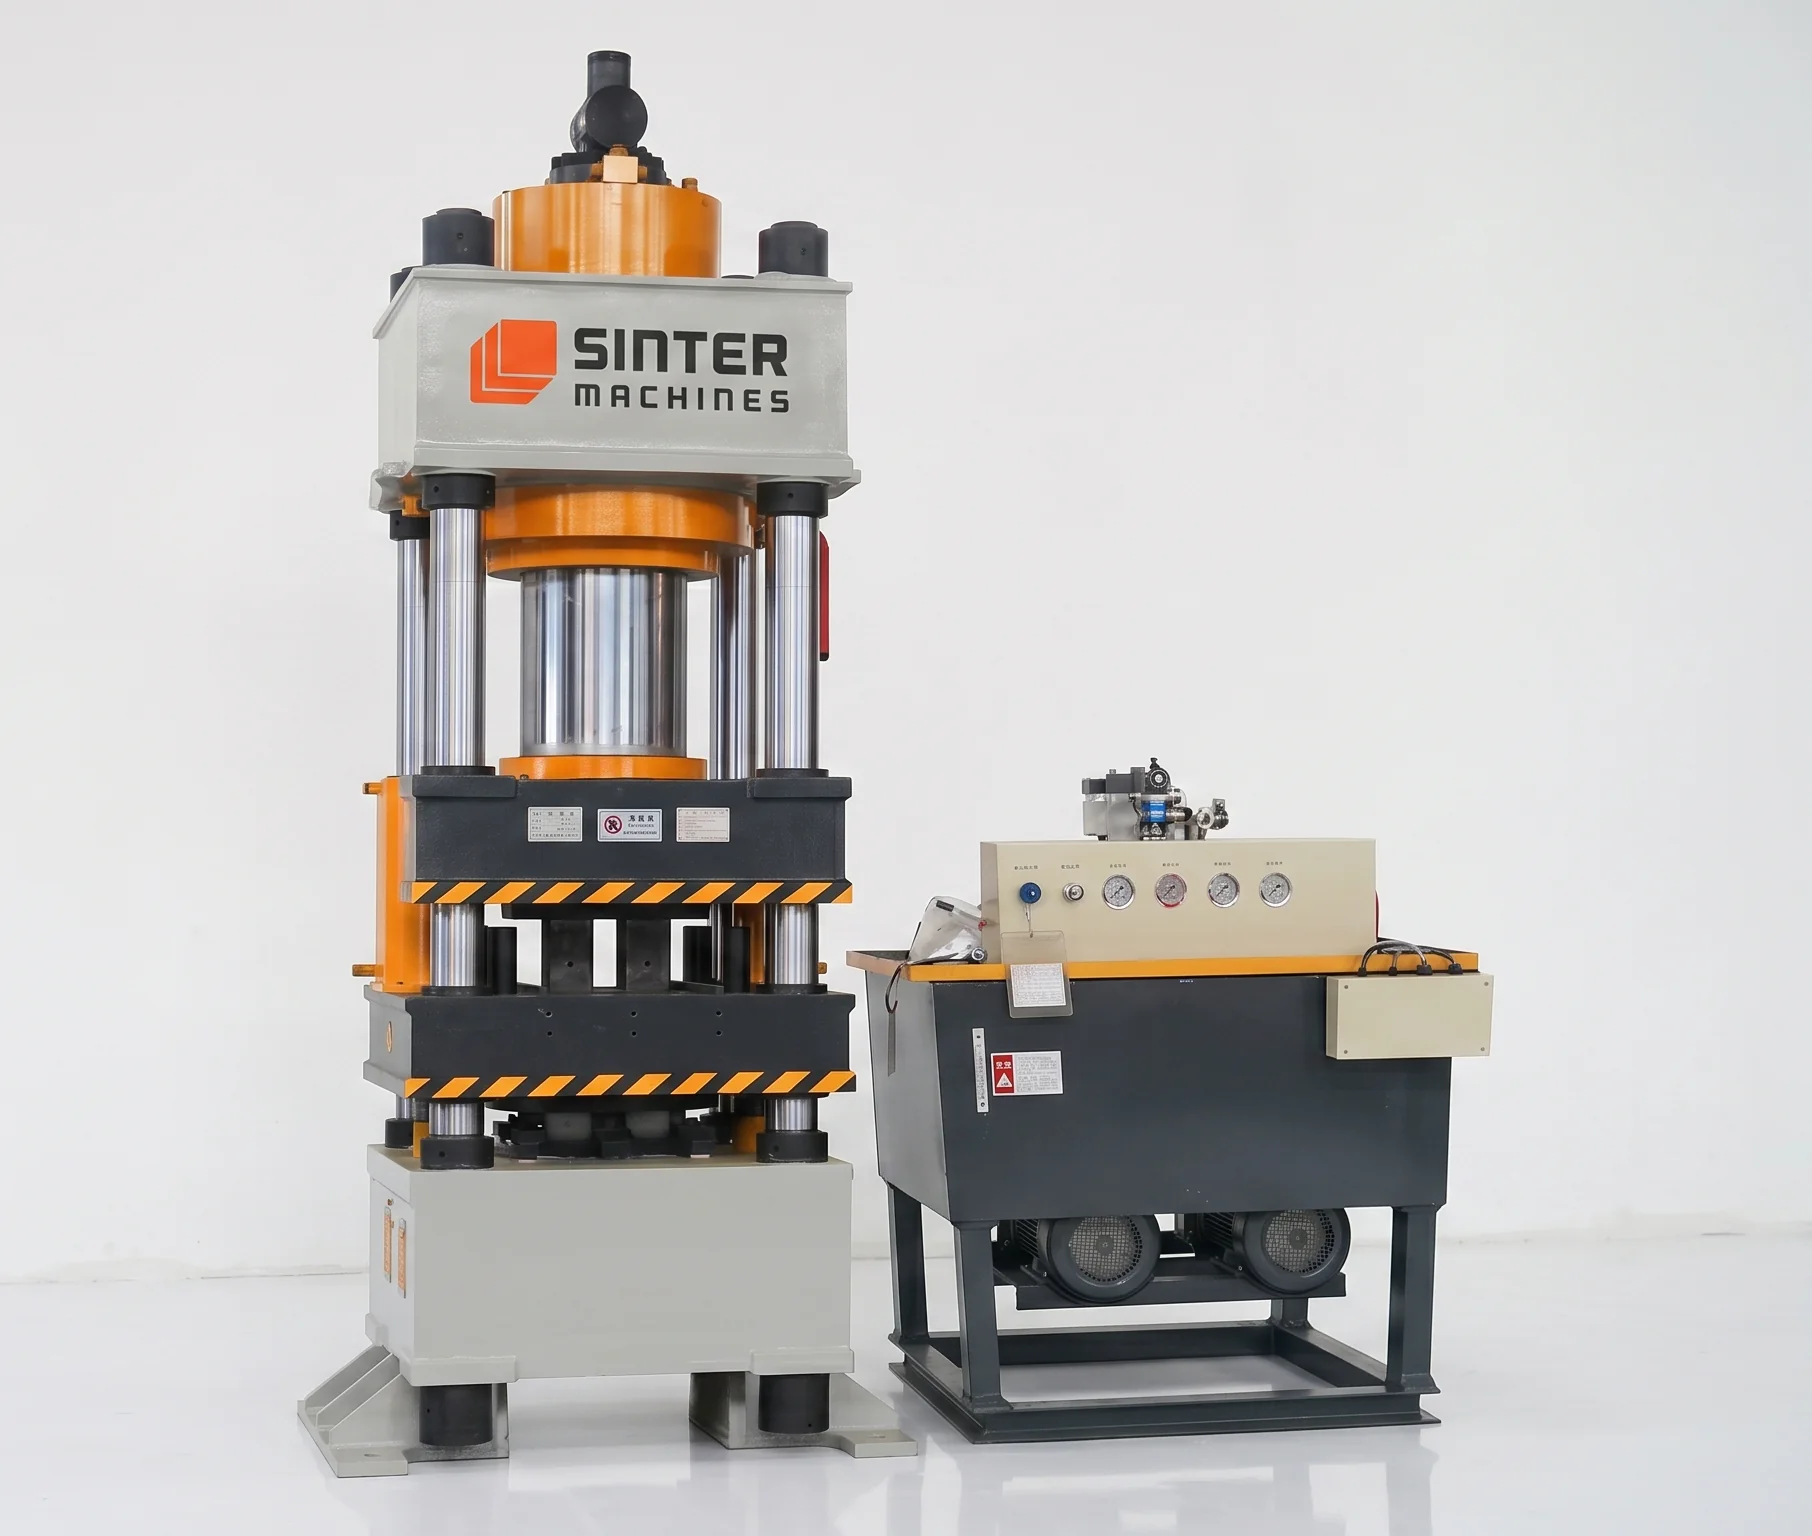
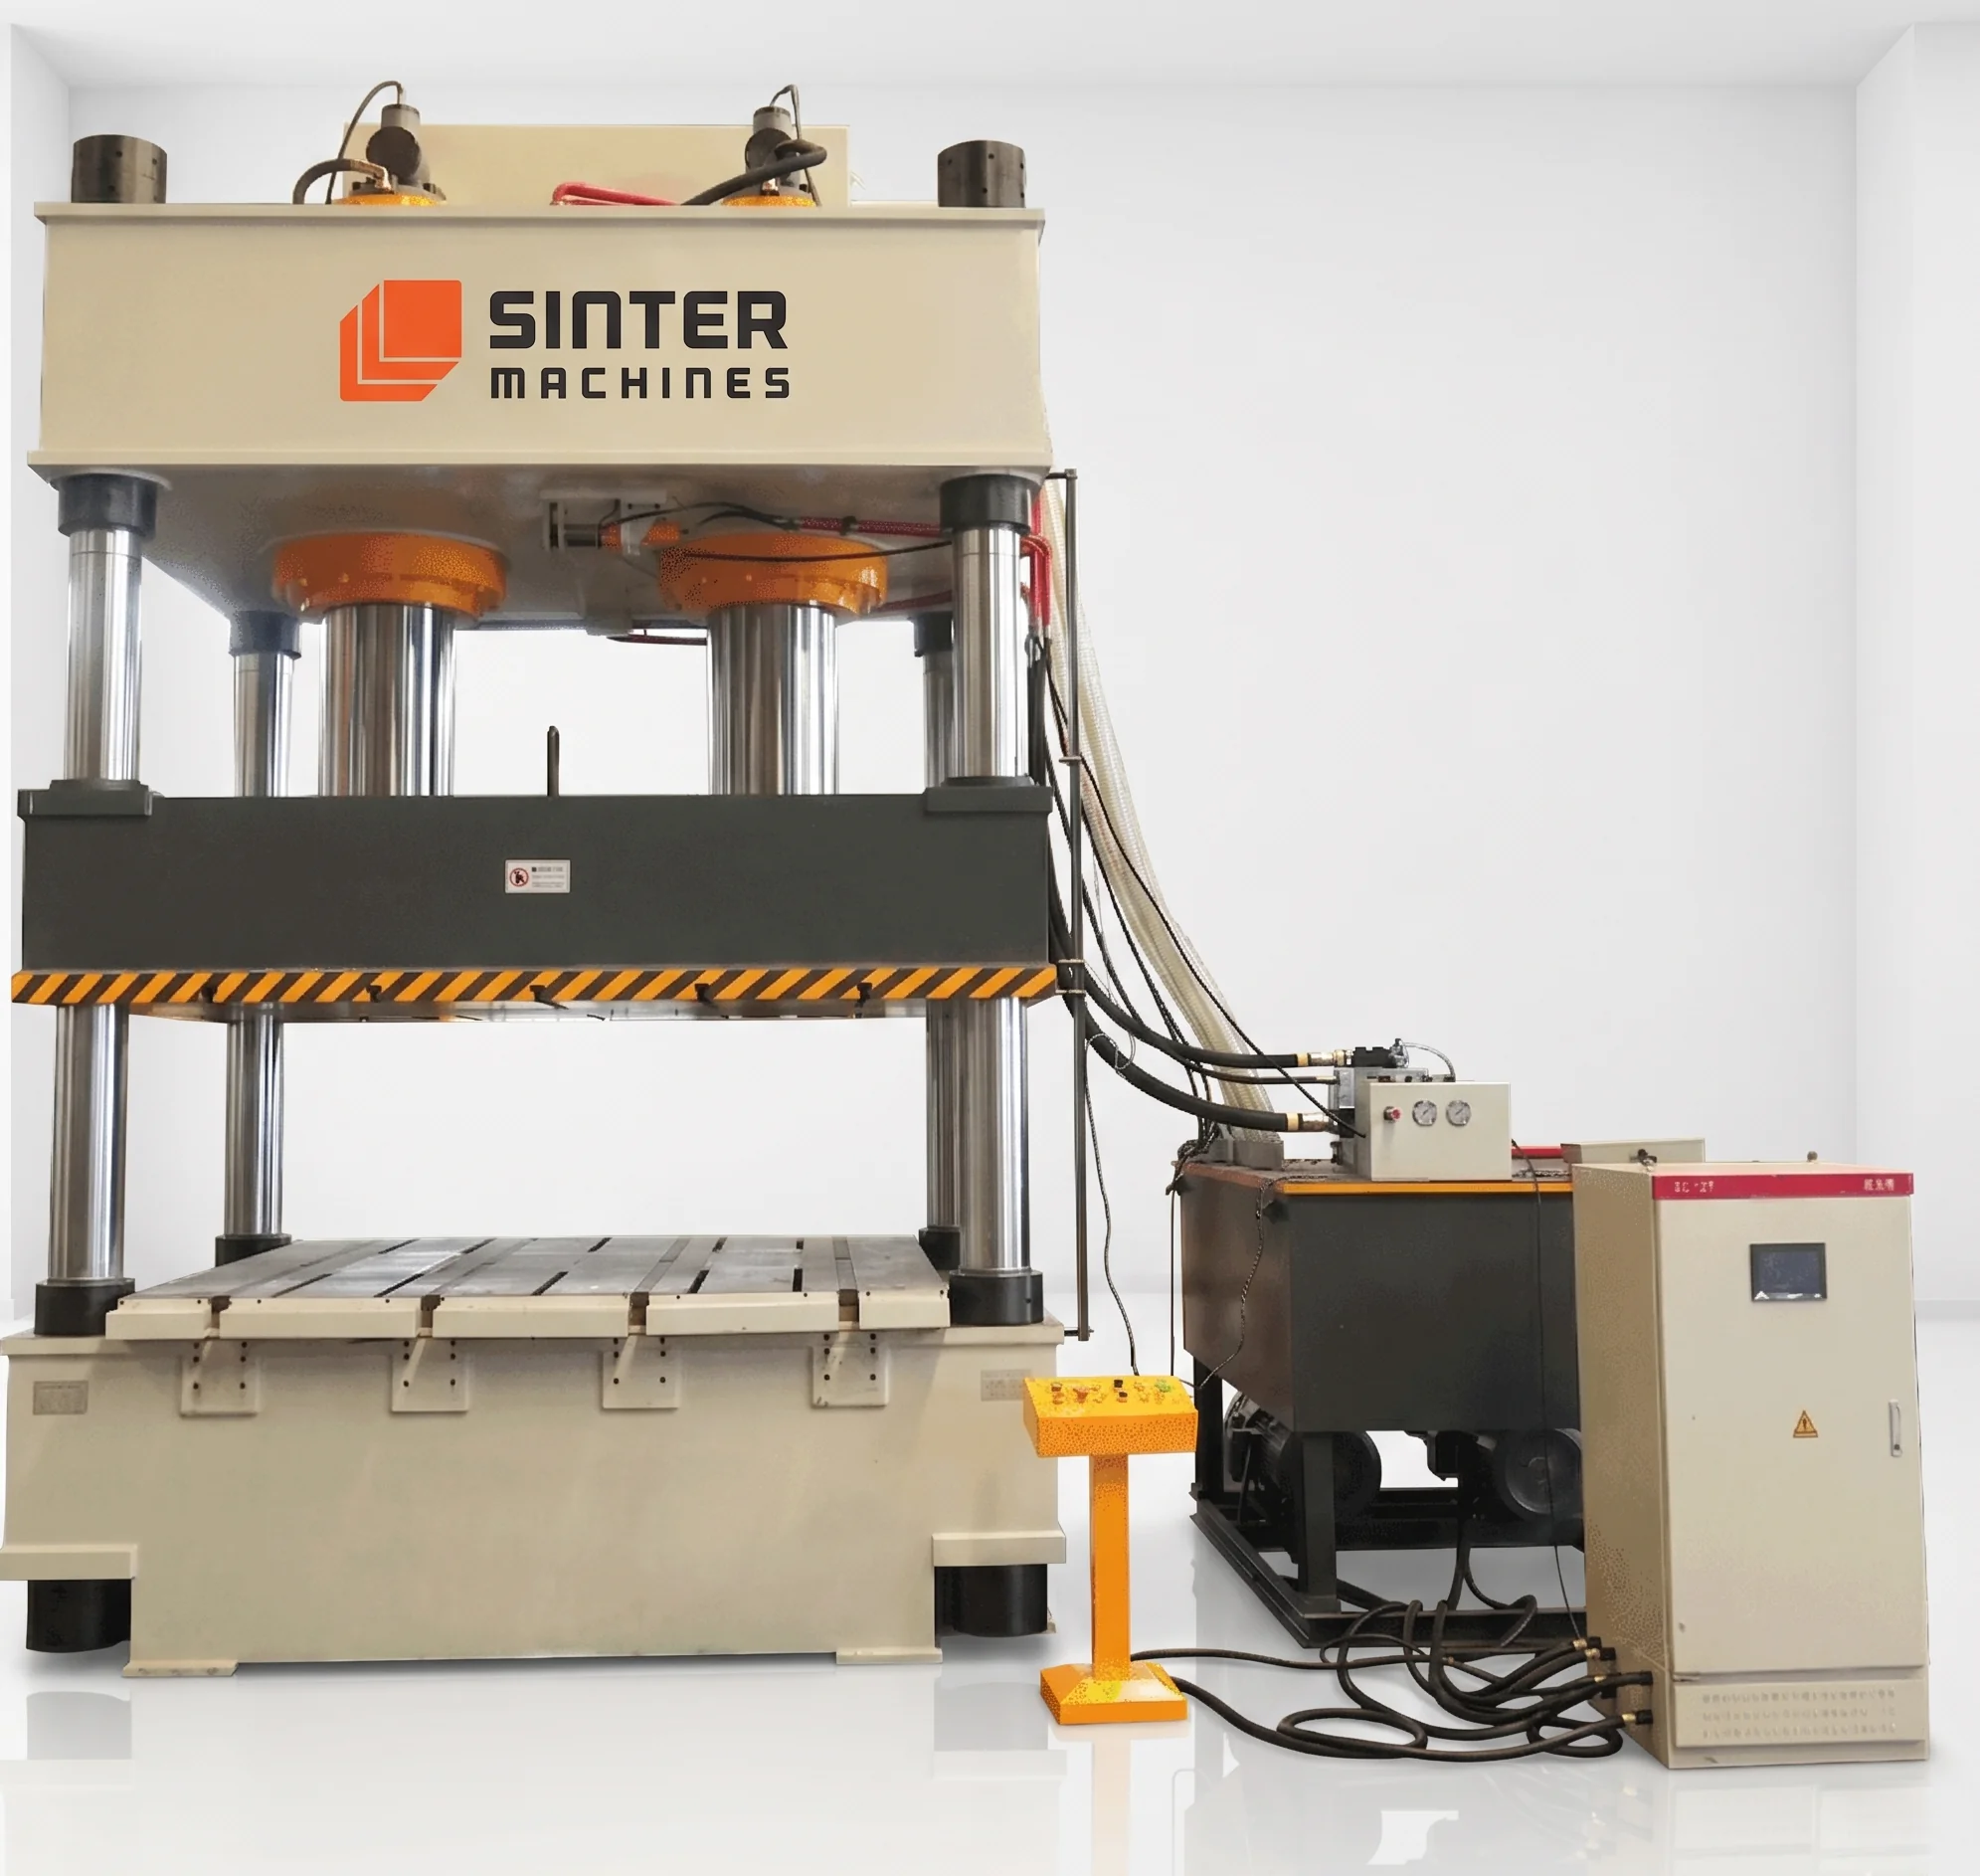
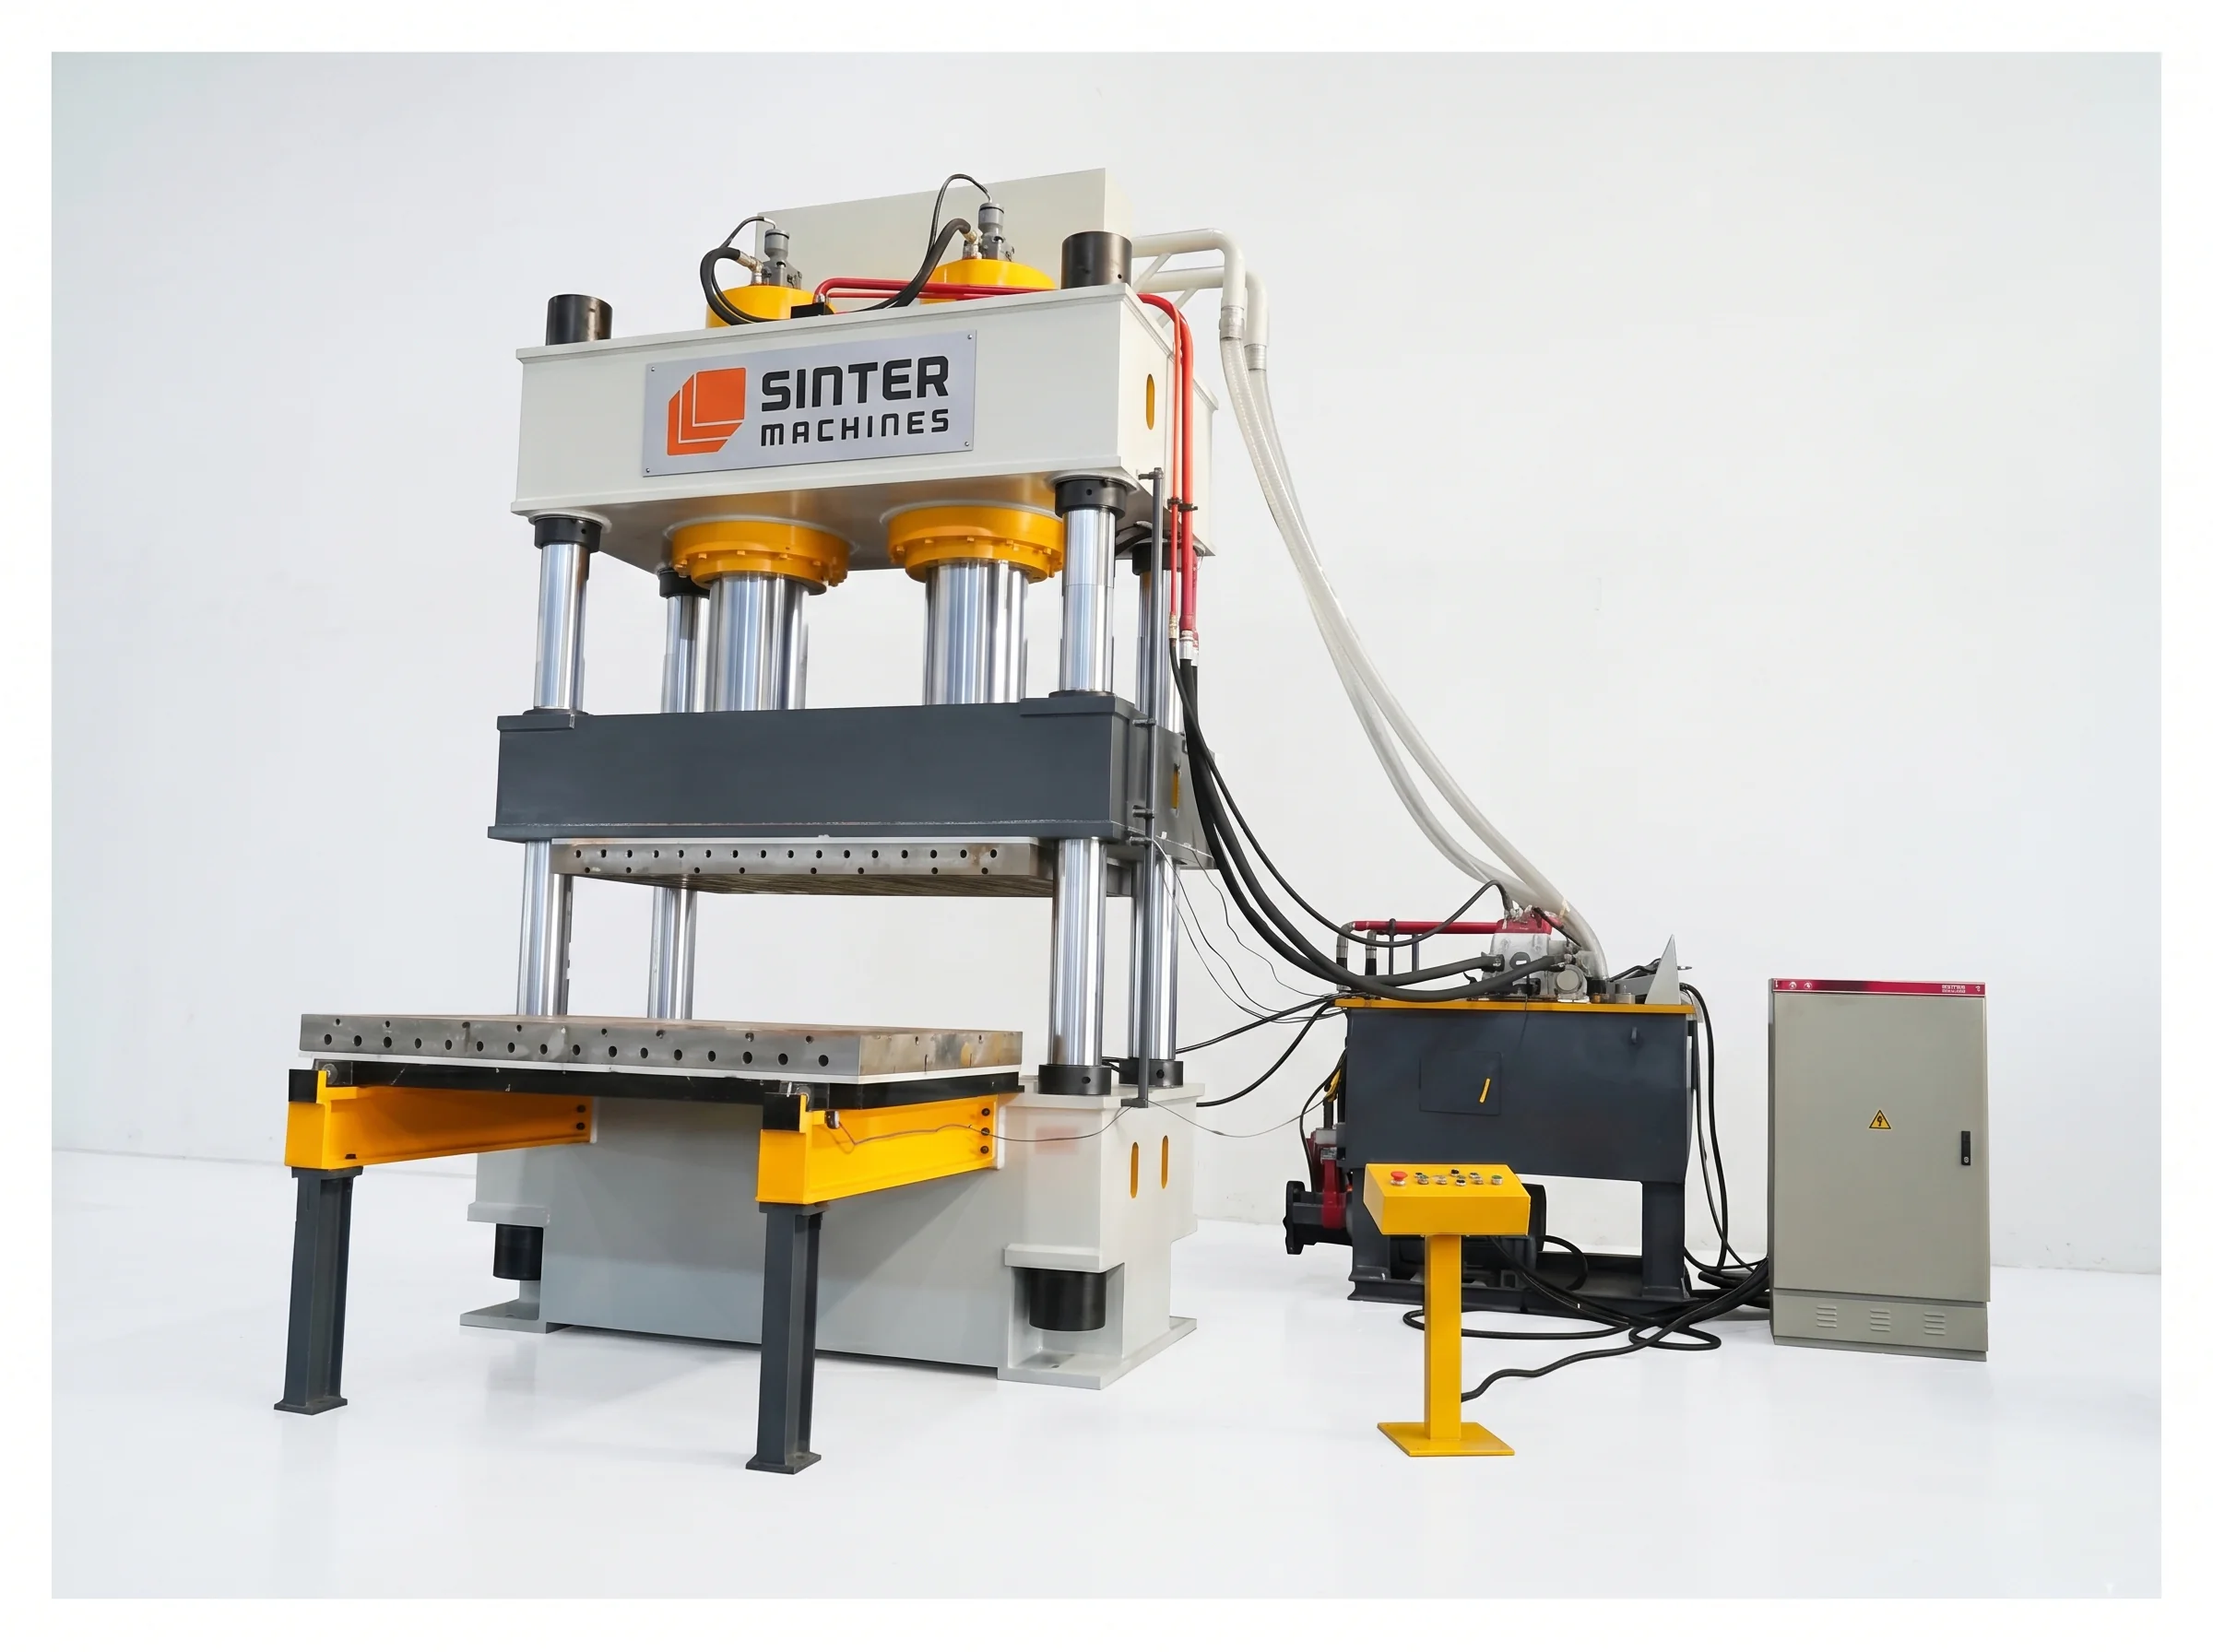
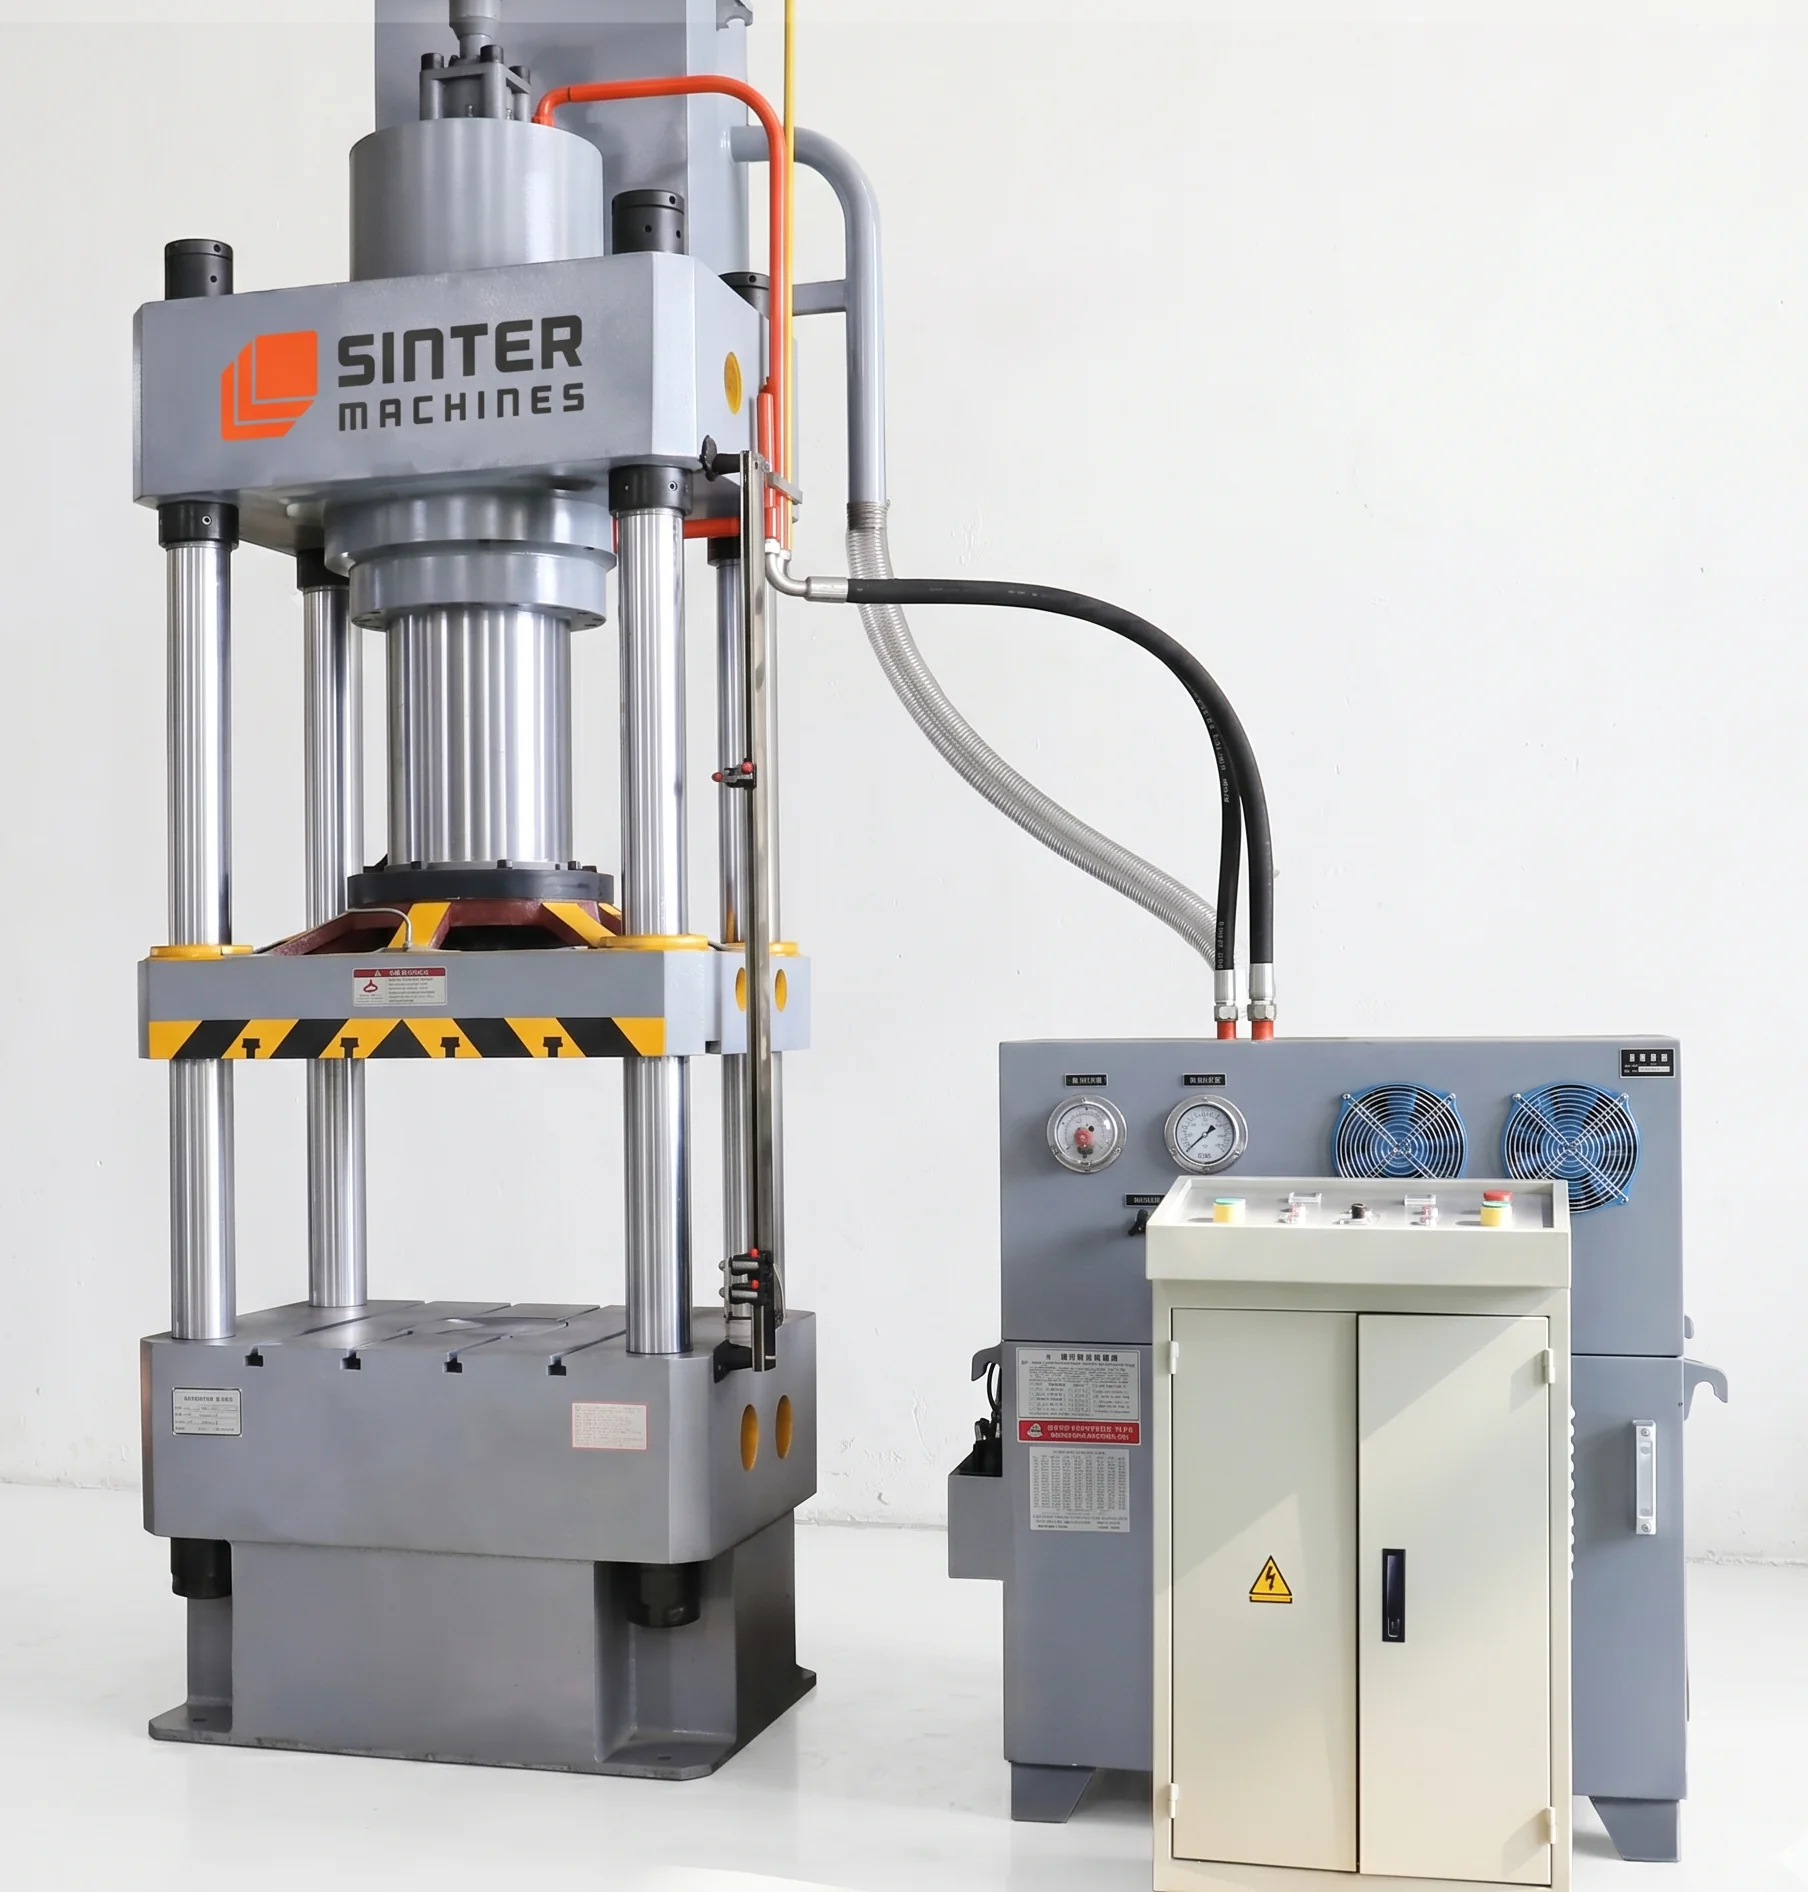
1600T Aerospace turbine components Press press view 1
Aerospace Turbine Components · Hydraulic Press Machine

1600T Four Column Hydraulic Press for Hot Forging Aerospace Turbine Components

1600T Rated Capacity
190 mm/s Slider Down Speed
6–14 mm/s Slider Pressing Speed
220 mm/s Slider Return Speed

01 — Press System

1600T Four Column Hydraulic Press Machine

The 1600-ton four-pillar hydraulic press provides a top-tier, heavy-duty industrial forming platform engineered specifically for demanding aerospace hot forging operations. This highly precise configuration satisfies international aerospace manufacturing standards to supply certified engine and landing gear components globally.

Use Case

Manufacturing aerospace turbine components requires extreme force control and thermal stability to overcome the high deformation resistance of specialized superalloys. This press system provides the structural rigidity and variable speed profiling needed to achieve flawless internal grain structure without introducing micro-voids.

Core Applications

  • Precision closed-die hot forging and isothermal processing of critical rotating engine parts
  • High-tonnage structural extrusion and net-shape forming of heavy airframe structural components
  • Advanced heavy-duty stamping, upsetting, and preform blanking of aerospace-grade superalloy billets

Material

  • High-strength titanium alloys including titanium 6Al-4V and beta-stabilized titanium matrices
  • Nickel-based and cobalt-based superalloys such as Inconel 718, Waspaloy, and Rene alloys
  • Ultra-high-strength structural steels, specialized stainless steels, and advanced aluminum-lithium formulations

Typical Products Processed

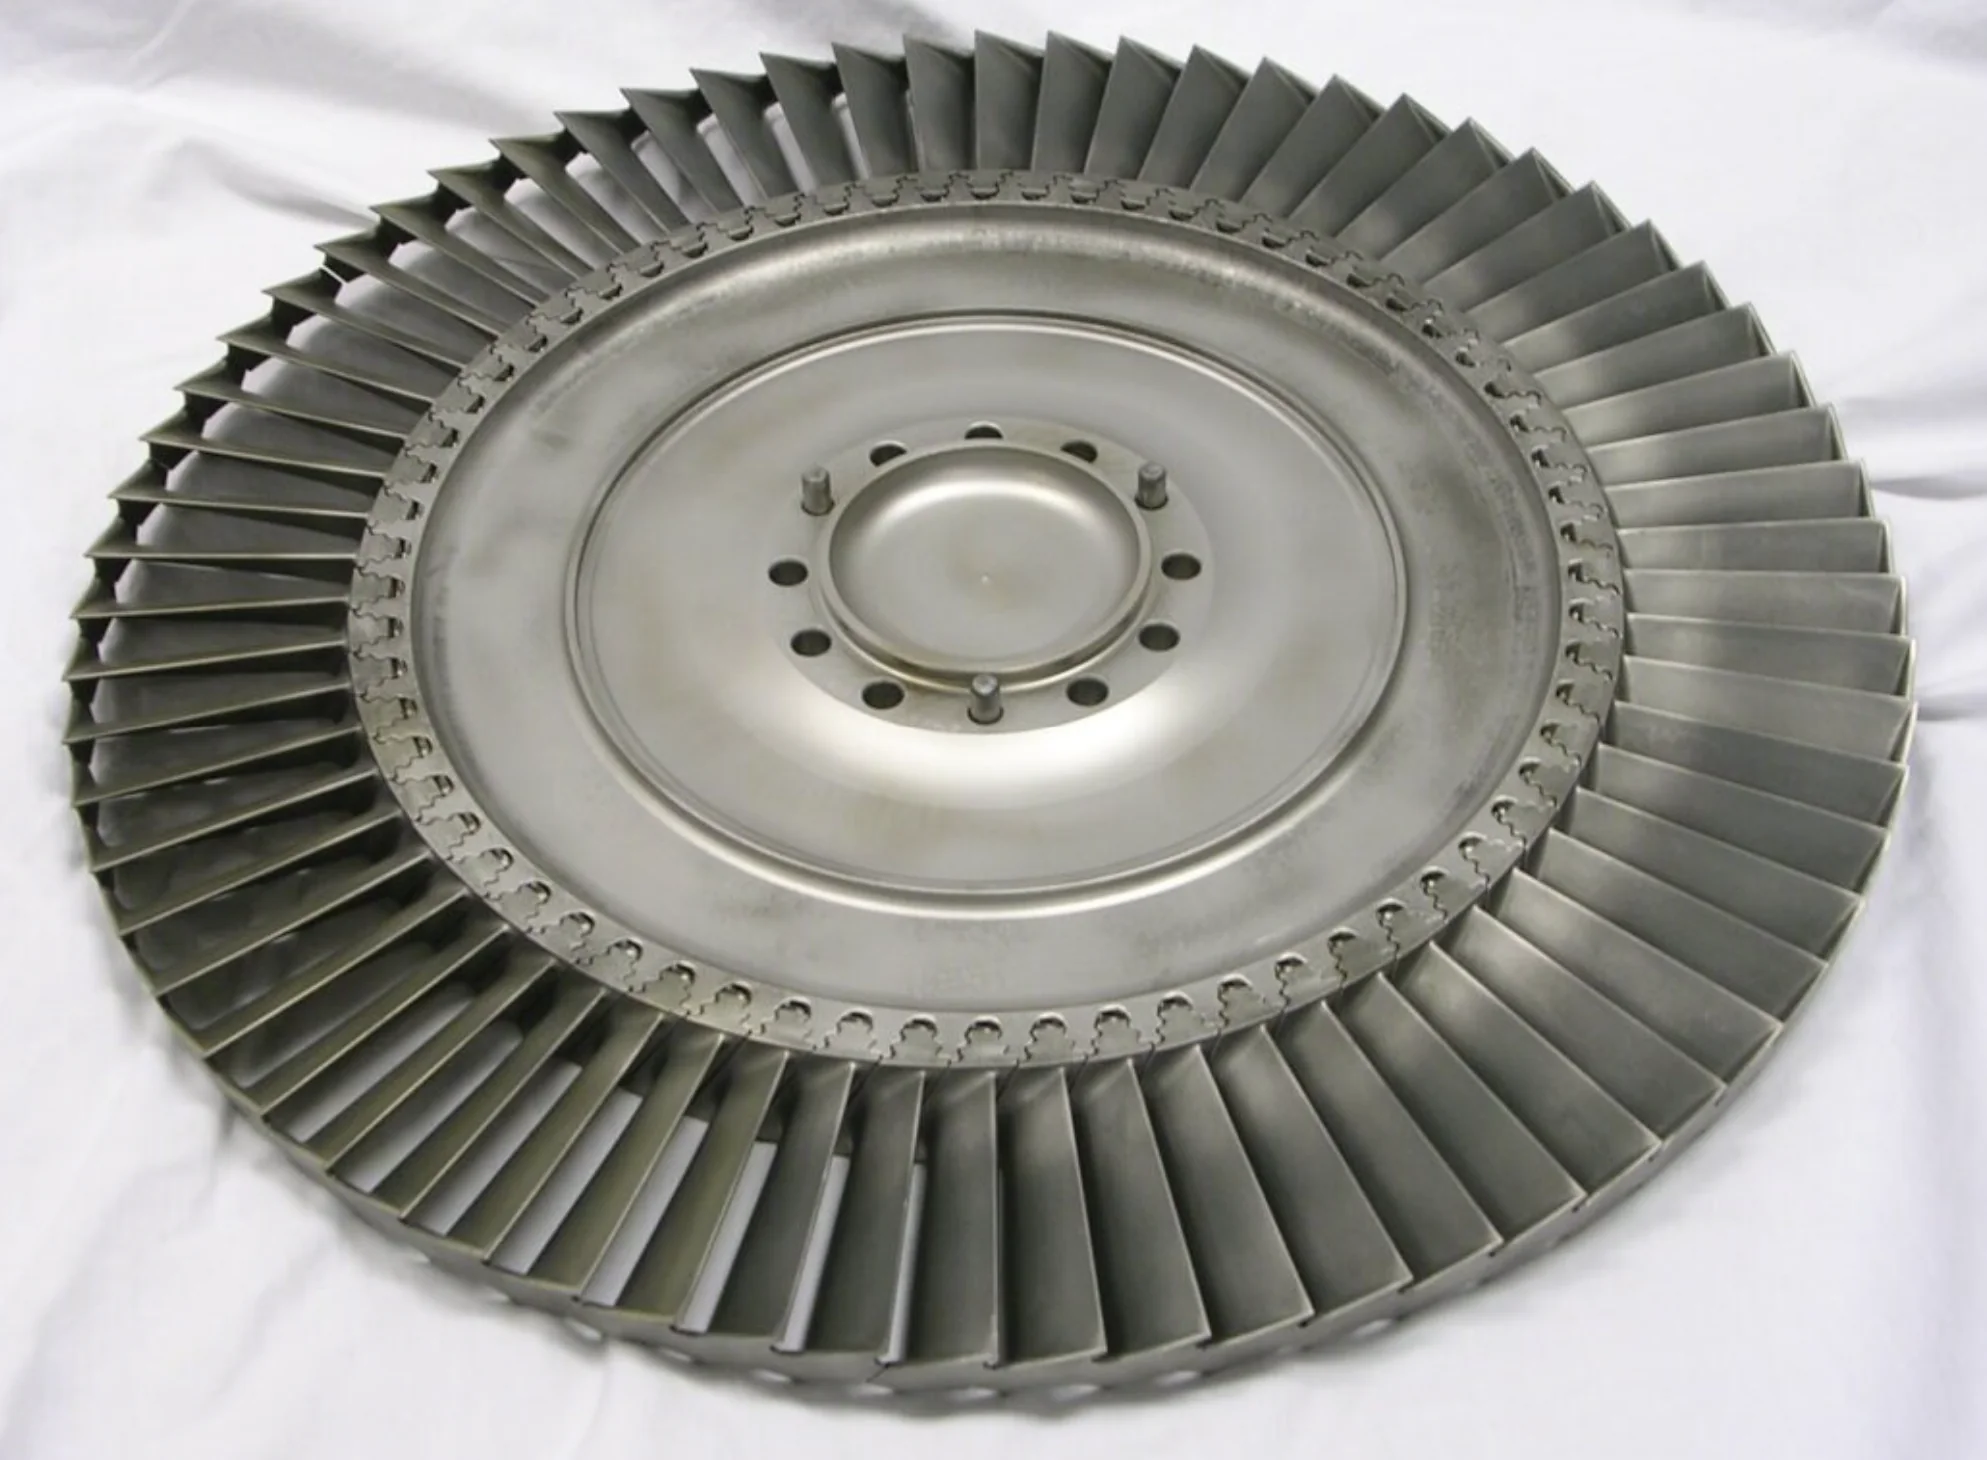
  • High-pressure compressor and turbine discs, structural fan shafts, and seamless spacer rings
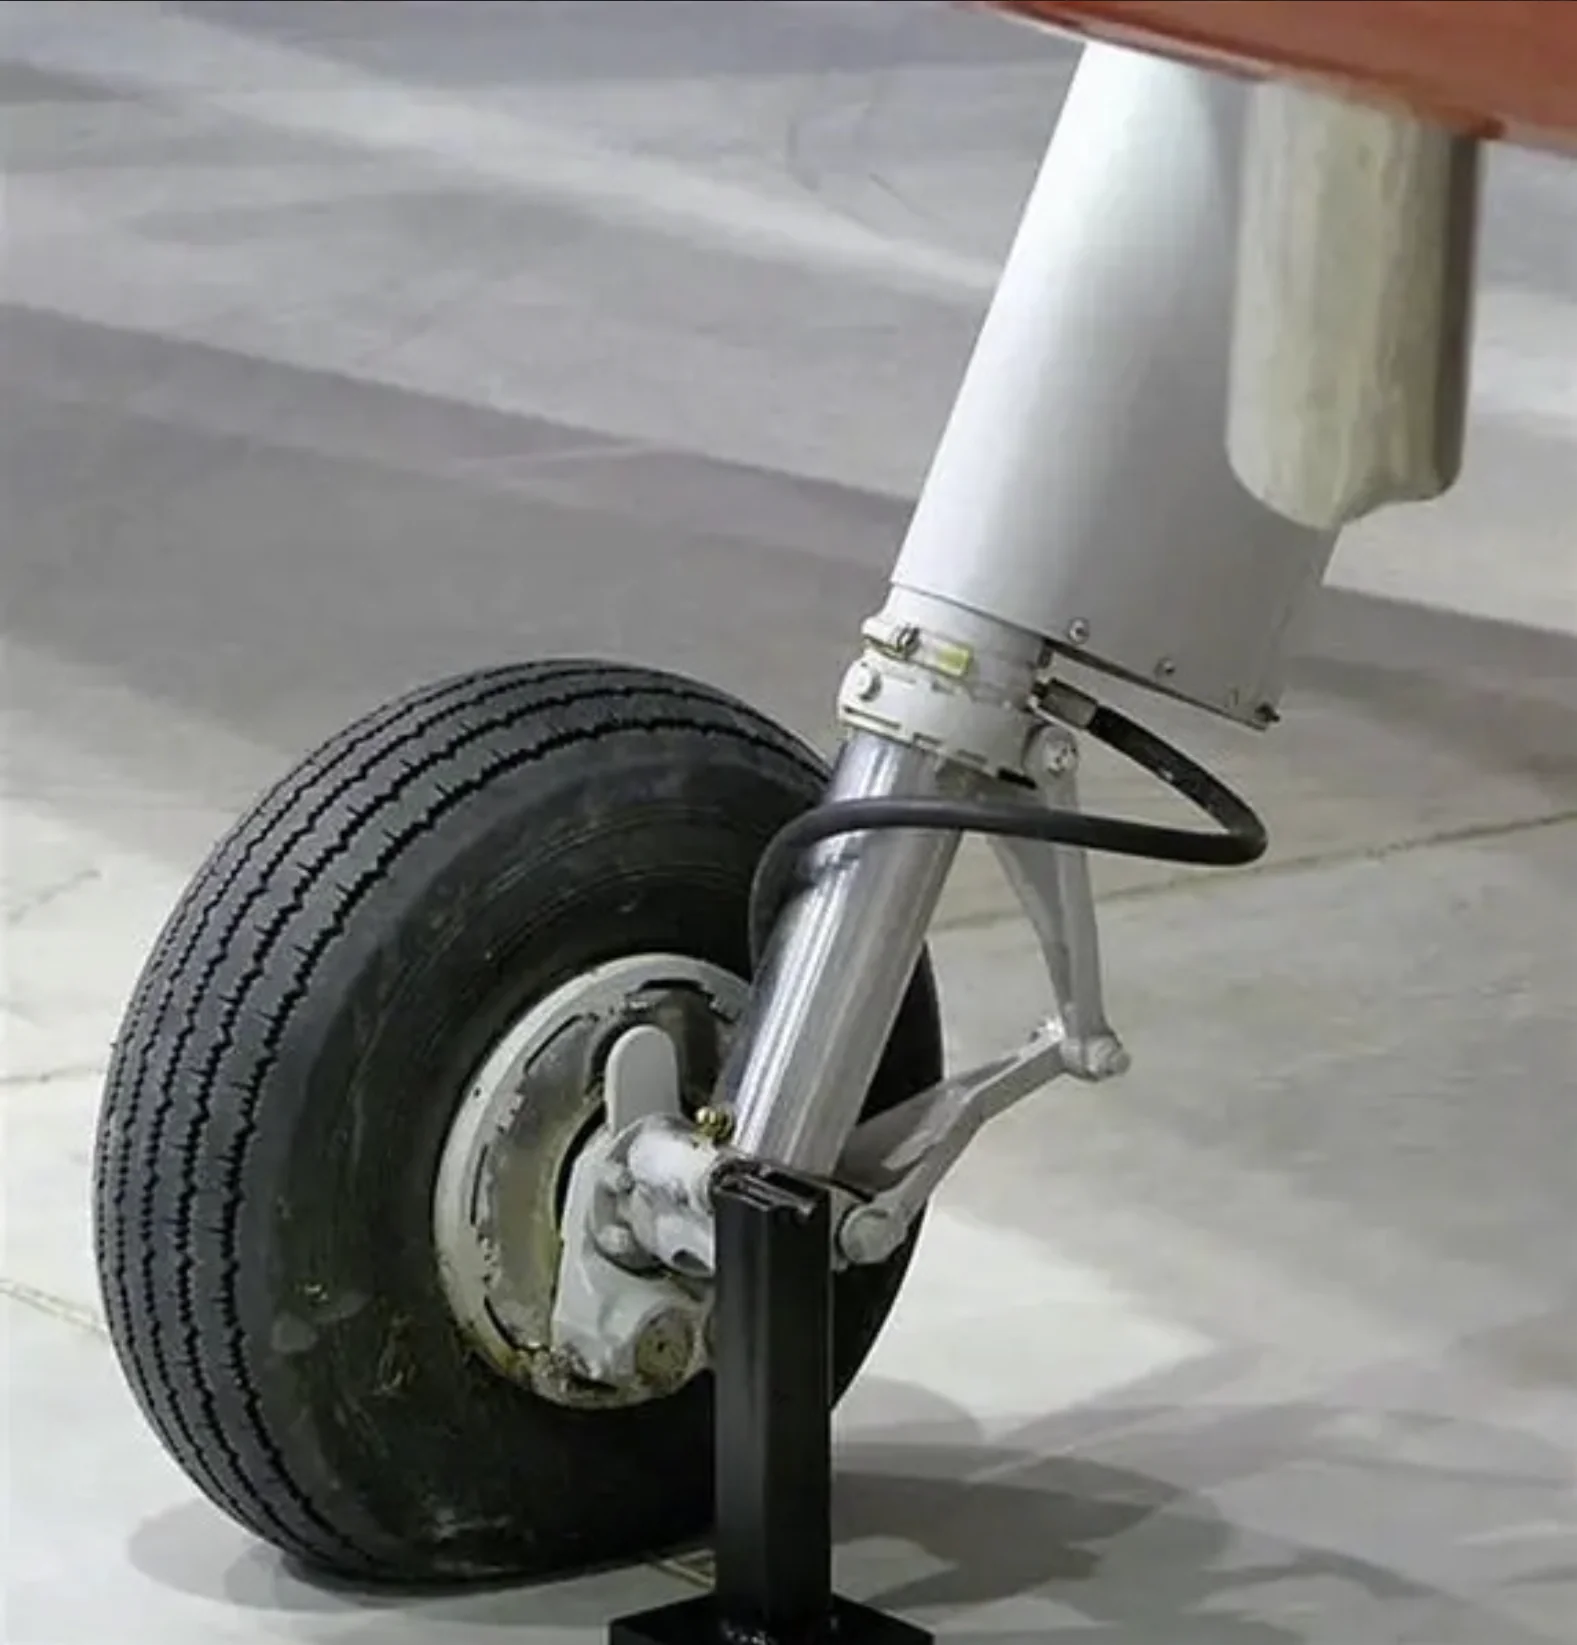
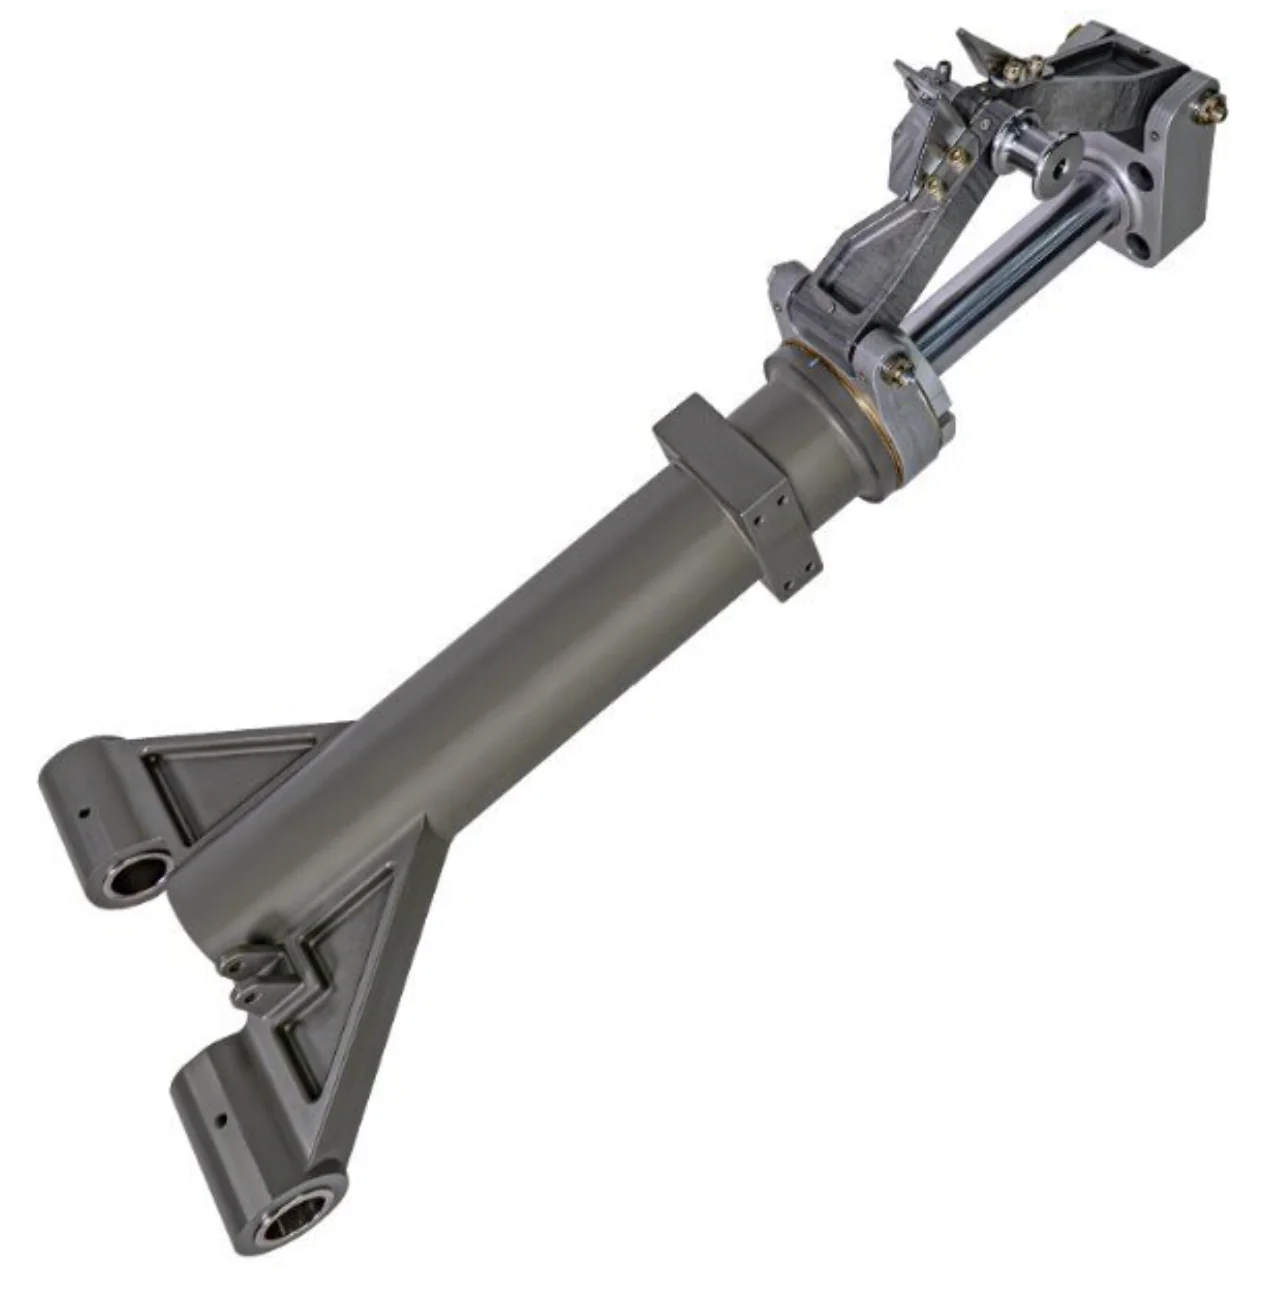
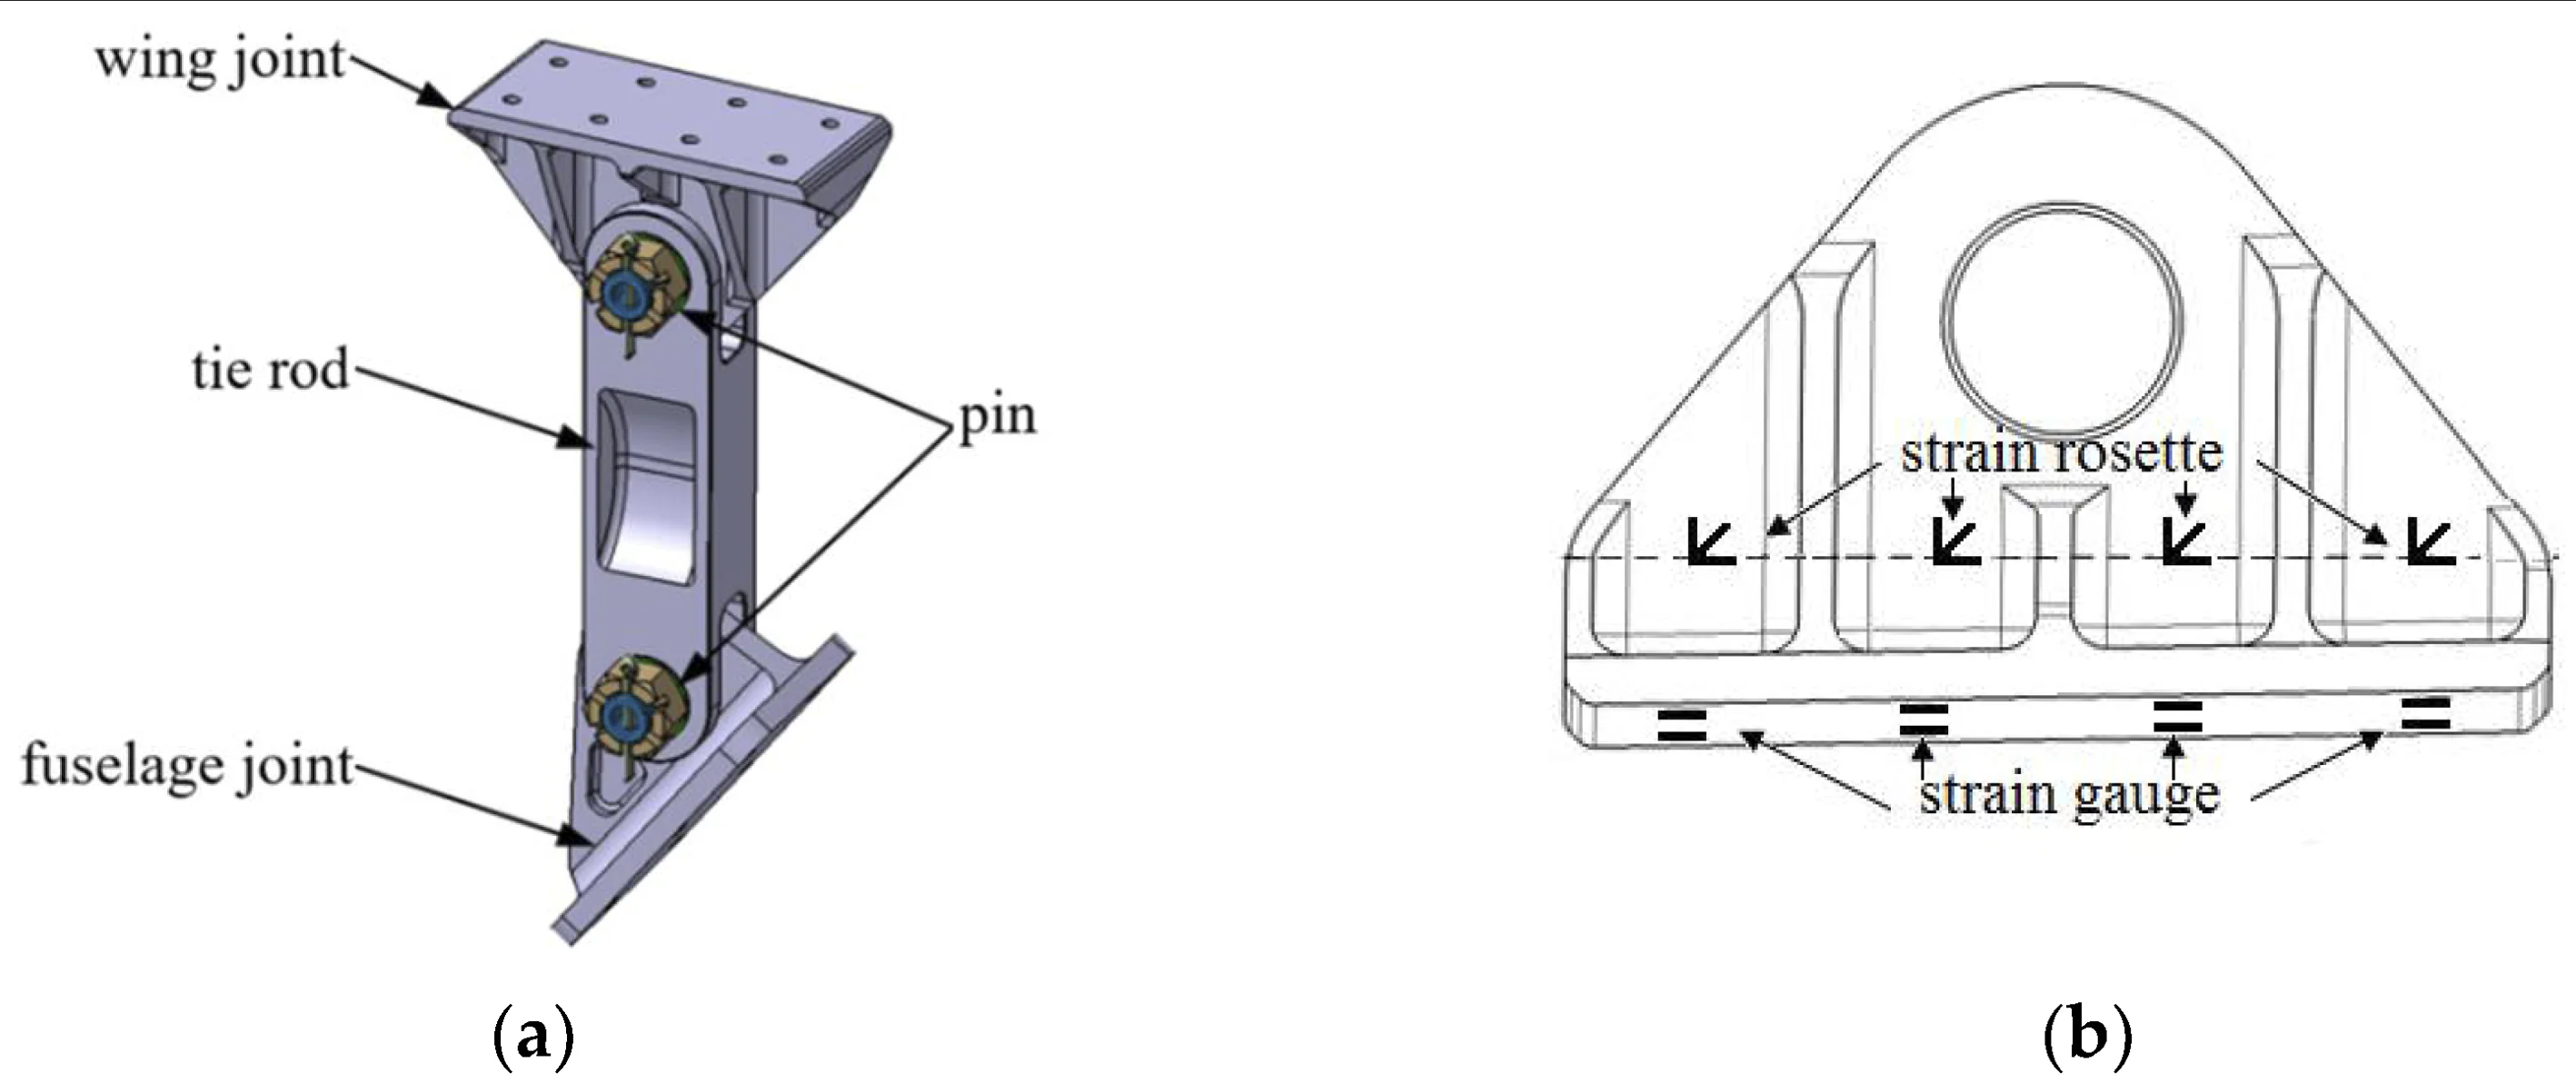
  • Heavy-duty landing gear cylinders, main axles, torque tubes, and structural airframe beam fittings
  • Missile fuselage segments, rocket motor cases, and high-stress military defense hardware components

Key Functions

  • Multi-step programmable strain-rate velocity control to prevent thermal spikes and localized cracking in superalloys
  • Synchronized high-pressure hydraulic ejector circuits integrated into both the bed and moving slide assemblies
  • Real-time electronic process data logging to ensure full traceability required for NADCAP audits

Why 1600 Ton Hydraulic Press?

  • Delivers the massive compression force needed to displace dense aerospace alloys within strict temperature windows
  • Pre-stressed four-pillar frame architecture minimizes structural deflection to maintain absolute platen parallelism under eccentric loads

02 — Technical Specifications

SM 1600 HP – HYDRAULIC PRESS MACHINE COMPLETE TECHNICAL DATA

The SM 1600 HP hydraulic press delivers massive compression forces and exceptional structural alignment tailored for processing high-density aerospace superalloys. Its advanced closed-loop velocity profiling and strict platen parallelism ensure flawless microstructural control and precise near-net-shape component geometry.

Capacity

  • Maximum continuous hot forging compression force capacity of 16000 kN
  • Dedicated heavy duty bottom ejector stripping force capacity of 1200 kN

Structural Design

  • High fatigue resistant pre stressed four column configuration built for rigorous aerospace production
  • Finite element analysis structural simulation frame designed to absorb intense thermal shocks

Frame Type

  • Precision aligned solid induction hardened pillar frame guide structure
  • Stress relieved heavy welded steel plate bolster and upper moving slide assembly

Hydraulic System

  • High output variable displacement axial piston pump fluid power assembly
  • Multi stage high capacity offline oil filtration loop with integrated oil coolers

Main Ram Stroke

  • Maximum vertical slide forming travel distance capability of 900 mm
  • Electronic stroke length limitation positioning resolution accurate within 0.02 mm

Working Hydraulic Pressure

  • Maximum continuous operating main hydraulic system fluid pressure of 315 bar
  • Peak shock safety valve pressure relief calibration threshold limit of 350 bar

Daylight Gap

  • Maximum open vertical daylight window working clearance of 1500 mm
  • Minimum closed shut die height tool workspace space of 600 mm

Approach Speed

  • Accelerated downward advance slide rapid travel speed of 250 mm/Sec
  • Controlled high temperature tool engagement deceleration velocity of 12 mm/Sec

Pressing / Drawing Speed

  • Dynamic high pressure hot forging compression speed of 2 to 20 mm/Sec
  • Maximum resistance continuous metal displacement squeezing velocity of 30 mm/Sec

Return Speed

  • High speed upward ram extraction retraction travel speed of 220 mm/Sec
  • Ultra fast automated hydraulic pre return system decompression cycle timing

Bed / Platen Size Platen

  • Total clear bolster bed width left to right of 1600 mm
  • Total clear bolster bed depth front to back of 1400 mm

Columns

  • Ultra high tensile forged alloy steel pillar diameter of 320 mm
  • Heavy duty heat resistant bronze guide bushings with automatic grease lubrication

Working Envelope

  • Total horizontal internal clear workspace area of 1600 by 1400 mm
  • Maximum permissible upper die tool assembly mass weight of 12000 kg

Control System

  • Industrial programmable logic controller linked with a graphical touchscreen station
  • Dual redundant non contact linear transducer position tracking systems accurate within 0.01 mm

Main Motor Power

  • High efficiency primary hydraulic pump electric drive motor power of 160 kW
  • Dedicated auxiliary cooling and continuous oil filtration motor power of 22 kW

Valves & Hydraulics

  • High dynamic response proportional servo flow control cartridge manifold block
  • Integrated fast acting overhead gravity pre fill oil valve unit assembly

Automation

  • Digital interface connection ports for synchronized industrial robotic billet handling manipulators
  • High temperature hydraulic quick action die clamping system connecting lines

Safety Features

  • Heat shielded front and rear dual channel infrared light curtain barriers
  • Automated heavy duty dual fail safe mechanical anti drop ram safety locking blocks

SM 1600 HP — Model Specifications

  • Nominal Force: 16000 KN
  • Maximum Hydraulic Pressure: 25 MPa
  • Max Opening Height of the Slider: 1500 mm
  • Max Stroke of the Slider: 900 mm
  • Effective Bed Size: 1600 × 1600 mm
  • Slider Down Speed: 190 mm/s
  • Slider Pressing Speed: 6–14 mm/s
  • Slider Return Speed: 220 mm/s
  • Ejector Cylinder Nominal Force: 800 KN
  • Stroke of the Ejection Cylinder: 300 mm
Production Case Study

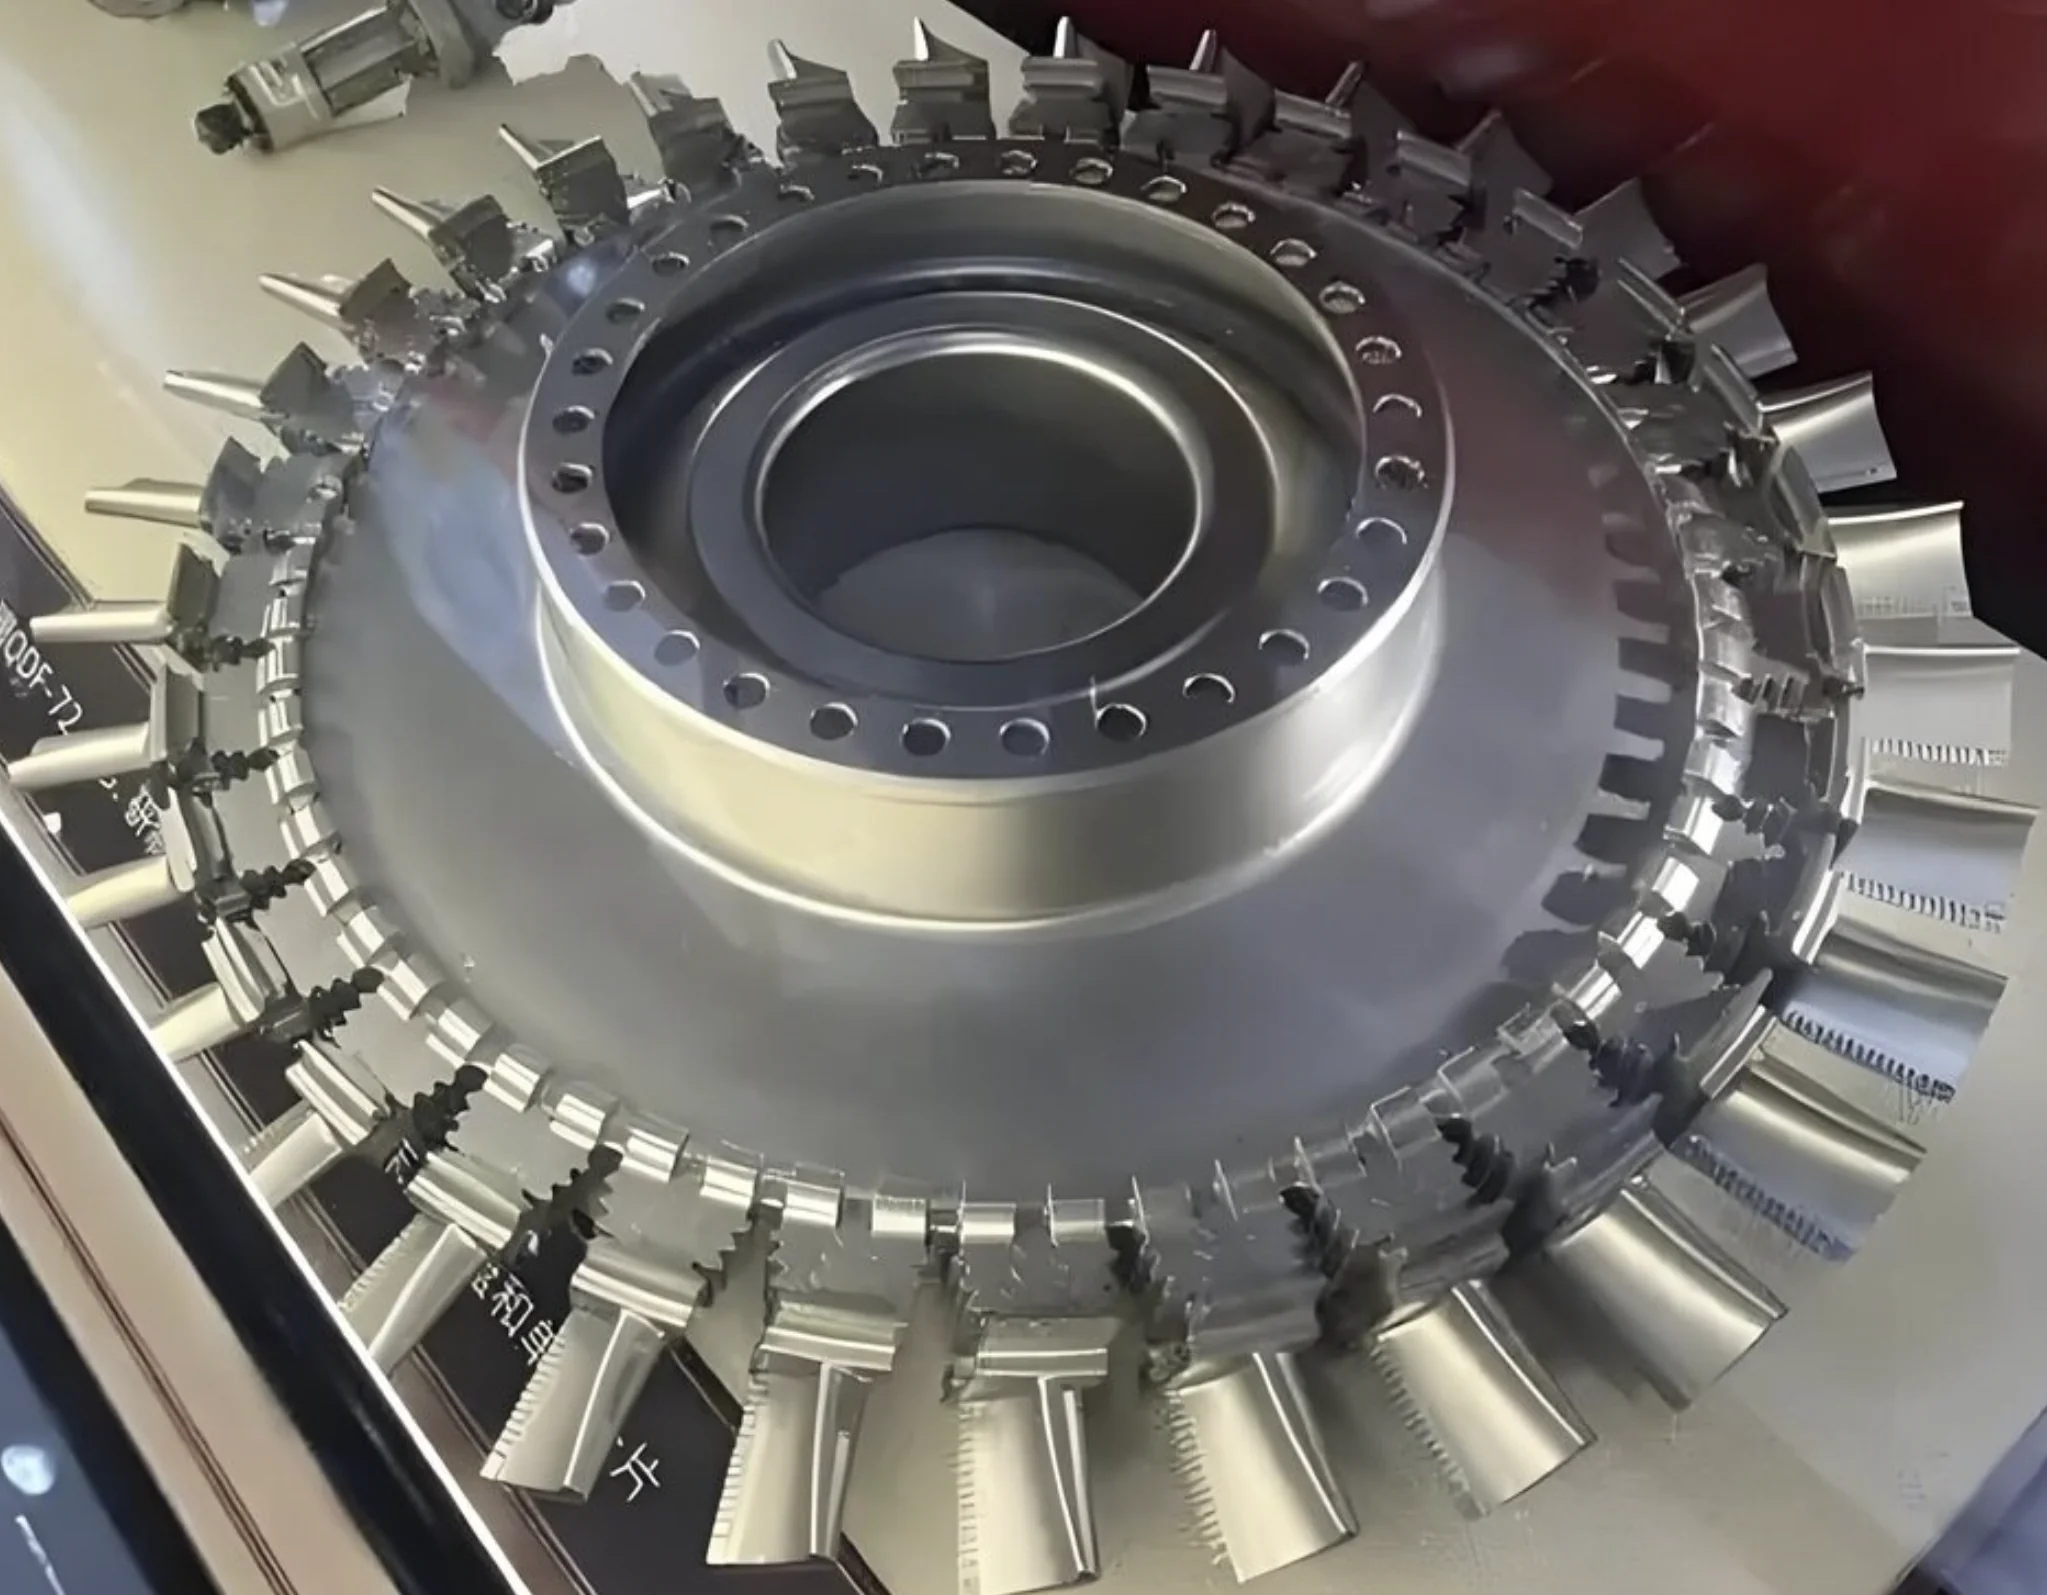
Hot Forging Aerospace Turbine Components Production Line

Ø 80 – 300 mmBillet dia
850–1,050 °CTemperature Range
45–90 secondsCycle time
40 to 80 PartsOutput/Hour
Grain structure optimized perfectly
Internal voids eliminated completely
Near net shapes achieved
Titanium alpha case prevented
Microstructural consistency verified fully
Die wear minimized significantly
Material scrap rates minimized
03 — Die / Mold System

Precision Hot Forging Aerospace Turbine Components Die Mold Engineering

This precision tooling system integrates high-stability isothermal closed-die architectures engineered to handle the extreme thermal loads and high deformation resistance of aerospace superalloys. The rugged structural configuration prevents thermal cracking and geometrical shifting during prolonged high-pressure squeezing cycles.

Technical Specifications (Tooling)

Die Type

  • Isothermal precision closed die hot forging tool set featuring advanced hot blank positioning systems
  • Multi stage progressive industrial tooling assembly engineered for safety critical aerospace components

Die Materials

  • Premium vacuum melted molybdenum base alloy providing extreme high temperature yield strength
  • Ultra high strength cobalt based superalloys utilized at high friction die throat zones

Tool Configuration & Construction

  • Heavy duty multi piece insert container configuration built to counteract intense lateral forces
  • Rigid pre stressed die block holder design optimized for quick mechanical tool changing operations

Key Tooling Features

  • Integrated multi zone induction heating elements designed to maintain constant die surface temperatures
  • Specialized high tonnage gas cushion ejection pins engineered for smooth part stripping sequences

Alignment Accuracy

  • Upper and lower die mismatch alignment deviation held strictly below a limit of 0.080 mm
  • Precision guide column geometric concentricity tolerance restricted within a limit of 0.015 mm

Process Materials

  • High density nickel based superalloys titanium alloys and specialized high strength stainless steel bars
  • Premium aerospace grade advanced structural metals matching international flight safety standards

Surface Finish

  • Active molding cavity internal surfaces mirror polished down to a limit of Ra 0.20 microns
  • Advanced physical vapor deposition multilayer titanium aluminum nitride coating at 0.008 mm thickness

Tool Life

  • Expected production span of 3000 cycles before requiring mandatory cavity reconditioning procedures
  • Total structural tooling lifespan capacity reaching 25000 production cycles before complete replacement
Case Study (Die Performance)

Precision Hot Forging Aerospace Turbine Components Die Mold

Mo AlloyDie Material
48–54 HRCHardness
Vacuum Stress AnnealingHeat Treatment
Thermal fatigue cracking eliminated
Plastic deformation resisted completely
Die wear minimized significantly
Dimensional drift prevented totally
Component surface defects avoided
Tooling life extended substantially
Production scrap reduced fully

04 — Product Application

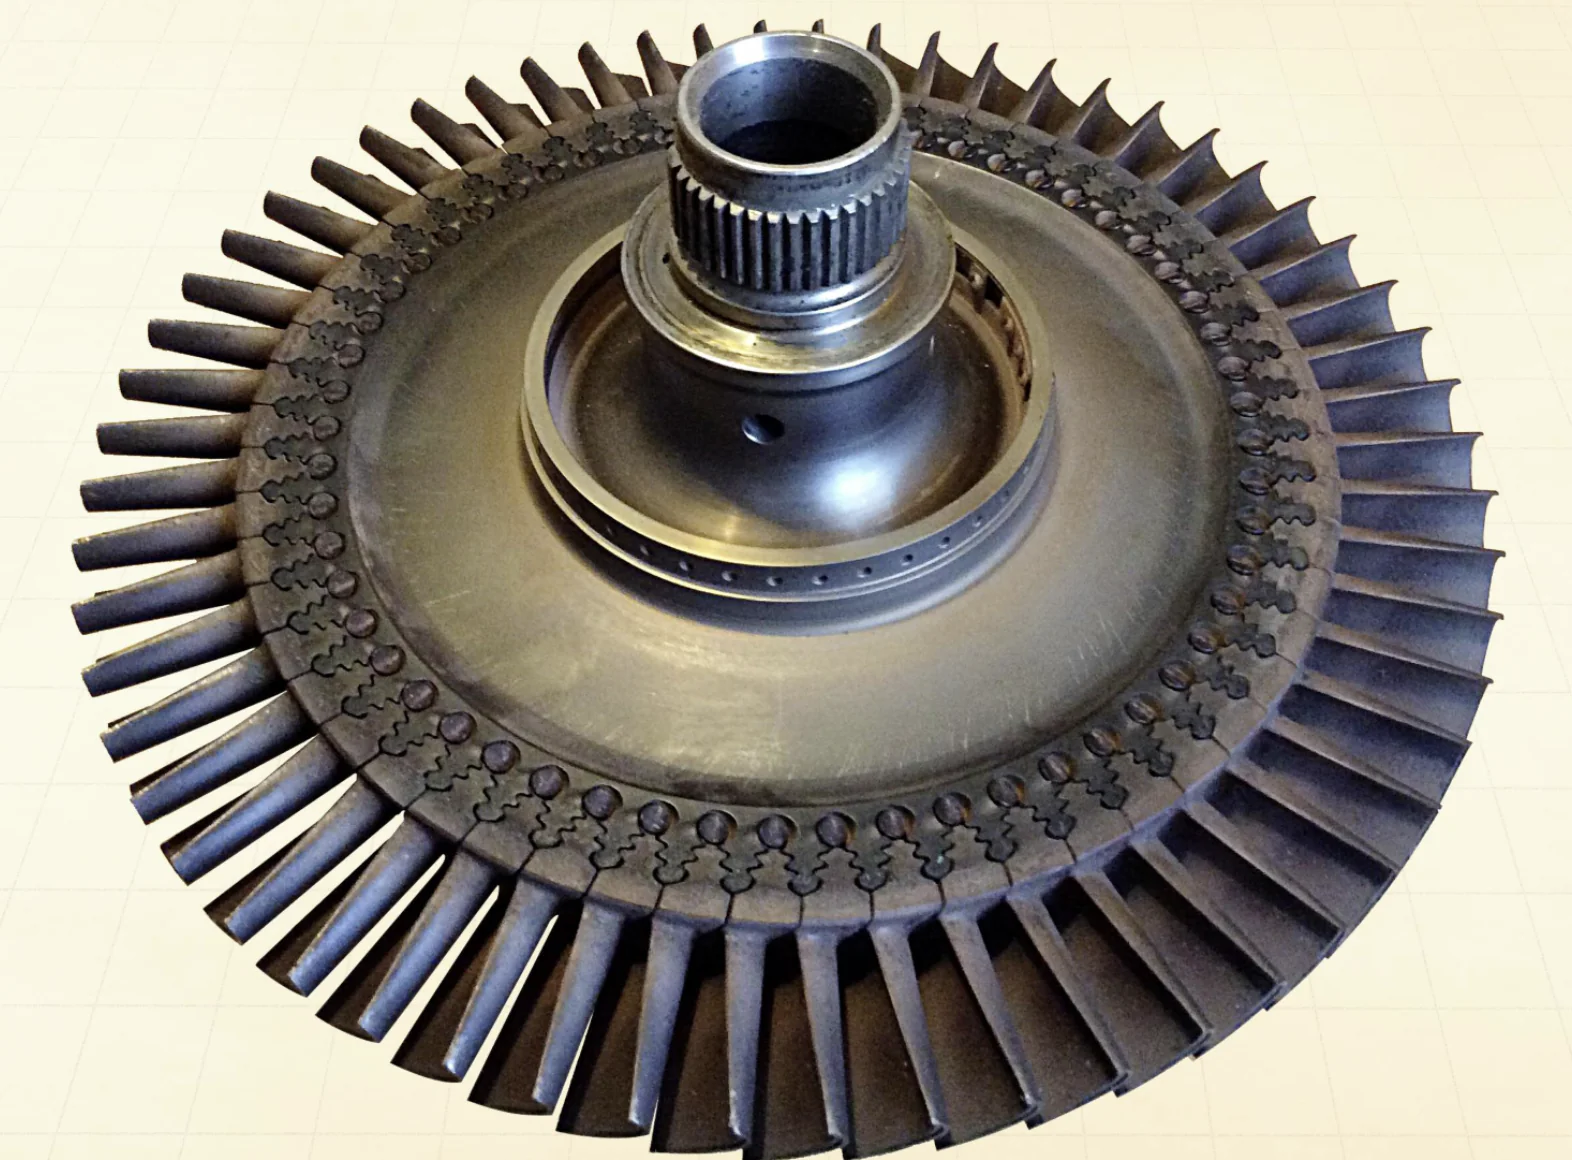
Where Precision Hot Forging Aerospace Turbine Components Are Used

Precision hot forged aerospace turbine components serve as high-integrity, safety-critical elements engineered to perform within the harshest thermal and mechanical environments of modern aviation. These advanced structural forgings ensure absolute structural reliability under extreme multi-axis g-forces, rapid rotational speeds, and corrosive high-temperature combustion exhaust gases.

Industry Applications

These ultra-precise aerospace forgings are indispensable across the global commercial aviation, military defense aerospace, rocket propulsion manufacturing, and heavy industrial power generation sectors. Their superior fatigue resistance, verified grain structures, and near-net-shape accuracy enable engineering teams to achieve extreme power-to-weight ratios, meet stringent emissions limits, and guarantee thousands of operational hours between mandatory maintenance cycles.

Commercial Jet Engines and Turbofans

Forged turbine discs, compressor rotors, and main fan shafts act as the primary rotating cores inside high-bypass commercial aircraft engines. Their uniform microstructural density prevents centrifugal deformation and creep failure during long-haul flights, ensuring maximum fuel efficiency and passenger safety.

Military Fighter Jet Propulsion Systems

High-strength titanium and nickel superalloy forgings handle the aggressive throttle cycles and thermal spikes characteristic of combat aircraft powerplants. The flawless grain flow structure delivers high fracture toughness, protecting the engine core against catastrophic disintegration during intense supersonic maneuvers.

Industrial Gas Turbines and Power Generation

Heavy-duty forged rings, spacer discs, and turbine blades drive large-scale electricity generation plants and pipeline compression stations. These robust components resist continuous thermal mechanical fatigue under uninterrupted, round-the-clock base-load operations, extending major plant overhaul intervals.

Space Launch Vehicles and Rocket Turbopumps

Ultra-dense rocket motor components and high-pressure turbopump impellers deliver cryogenic propellants into high-thrust rocket combustion chambers. The specialized metal structure maintains strict dimensional stability while transitioning instantly from freezing liquid fuel temperatures to extreme exhaust heat.

Finished Product Gallery

05 — Key Advantages

Why Choose the 1600-Ton Sinter Hydraulic Press

The 1600-Ton Sinter Hydraulic Press provides extreme compression force combined with micro-precision speed regulation to process dense, crack-sensitive aerospace superalloys. Its highly rigid four-pillar guidance and closed-loop process monitoring guarantee the flawless microstructural integrity and strict traceability required for flight certification.

Technical & Commercial Benefits

01

Ultra-Precise Programmable Strain-Rate and Velocity Profiling

The advanced servo-hydraulic controls adjust the slide velocity down to millimeters per second during the deformation process. This precise speed management prevents thermal spikes and micro-cracking in strain-sensitive titanium and nickel alloys, ensuring optimal grain refinement.

02

Exceptional Platen Parallelism Under Severe Asymmetric Loads

The heavy pre-stressed column design minimizes structural deflection to keep the moving slide perfectly aligned under eccentric forces. Maintaining absolute structural alignment eliminates geometric dimensional drift, extending the operating life of expensive molybdenum-base dies.

03

Synchronized High-Force Dual Hydraulic Ejection Systems

Integrated top and bottom high-tonnage knockout circuits deliver powerful, uniform stripping actions to clear deep-cavity turbine components. Rapid part extraction reduces the duration of high-temperature contact between the glowing billet and the die, preventing thermal fatigue cracking.

04

Real-Time Data Acquisition for Stringent Aerospace Traceability

The control network logs exact pressure curves, stroke distances, and heating parameters for every single forging cycle. Providing this comprehensive data buffer simplifies compliance documentation, satisfying the strict requirements of AS9100 and NADCAP certification audits.

05

Outstanding Near-Net-Shape Accuracy Minimizing Material Waste

Dual redundant linear transducers establish repeatable stroke endings to form components within small fractions of a millimeter. Achieving these tight dimensions straight out of the press bed reduces the loss of expensive superalloy raw stocks during post-forge machining.

06

Advanced Pressure Decompression Systems for Faster Cycle Times

Fast-acting hydraulic circuits bleed off massive internal system fluid pressures smoothly to accelerate the upper slide return stroke. Speeding up these processing steps increases hourly component throughput while reducing net electrical energy consumption per manufactured unit.