01 — Press System
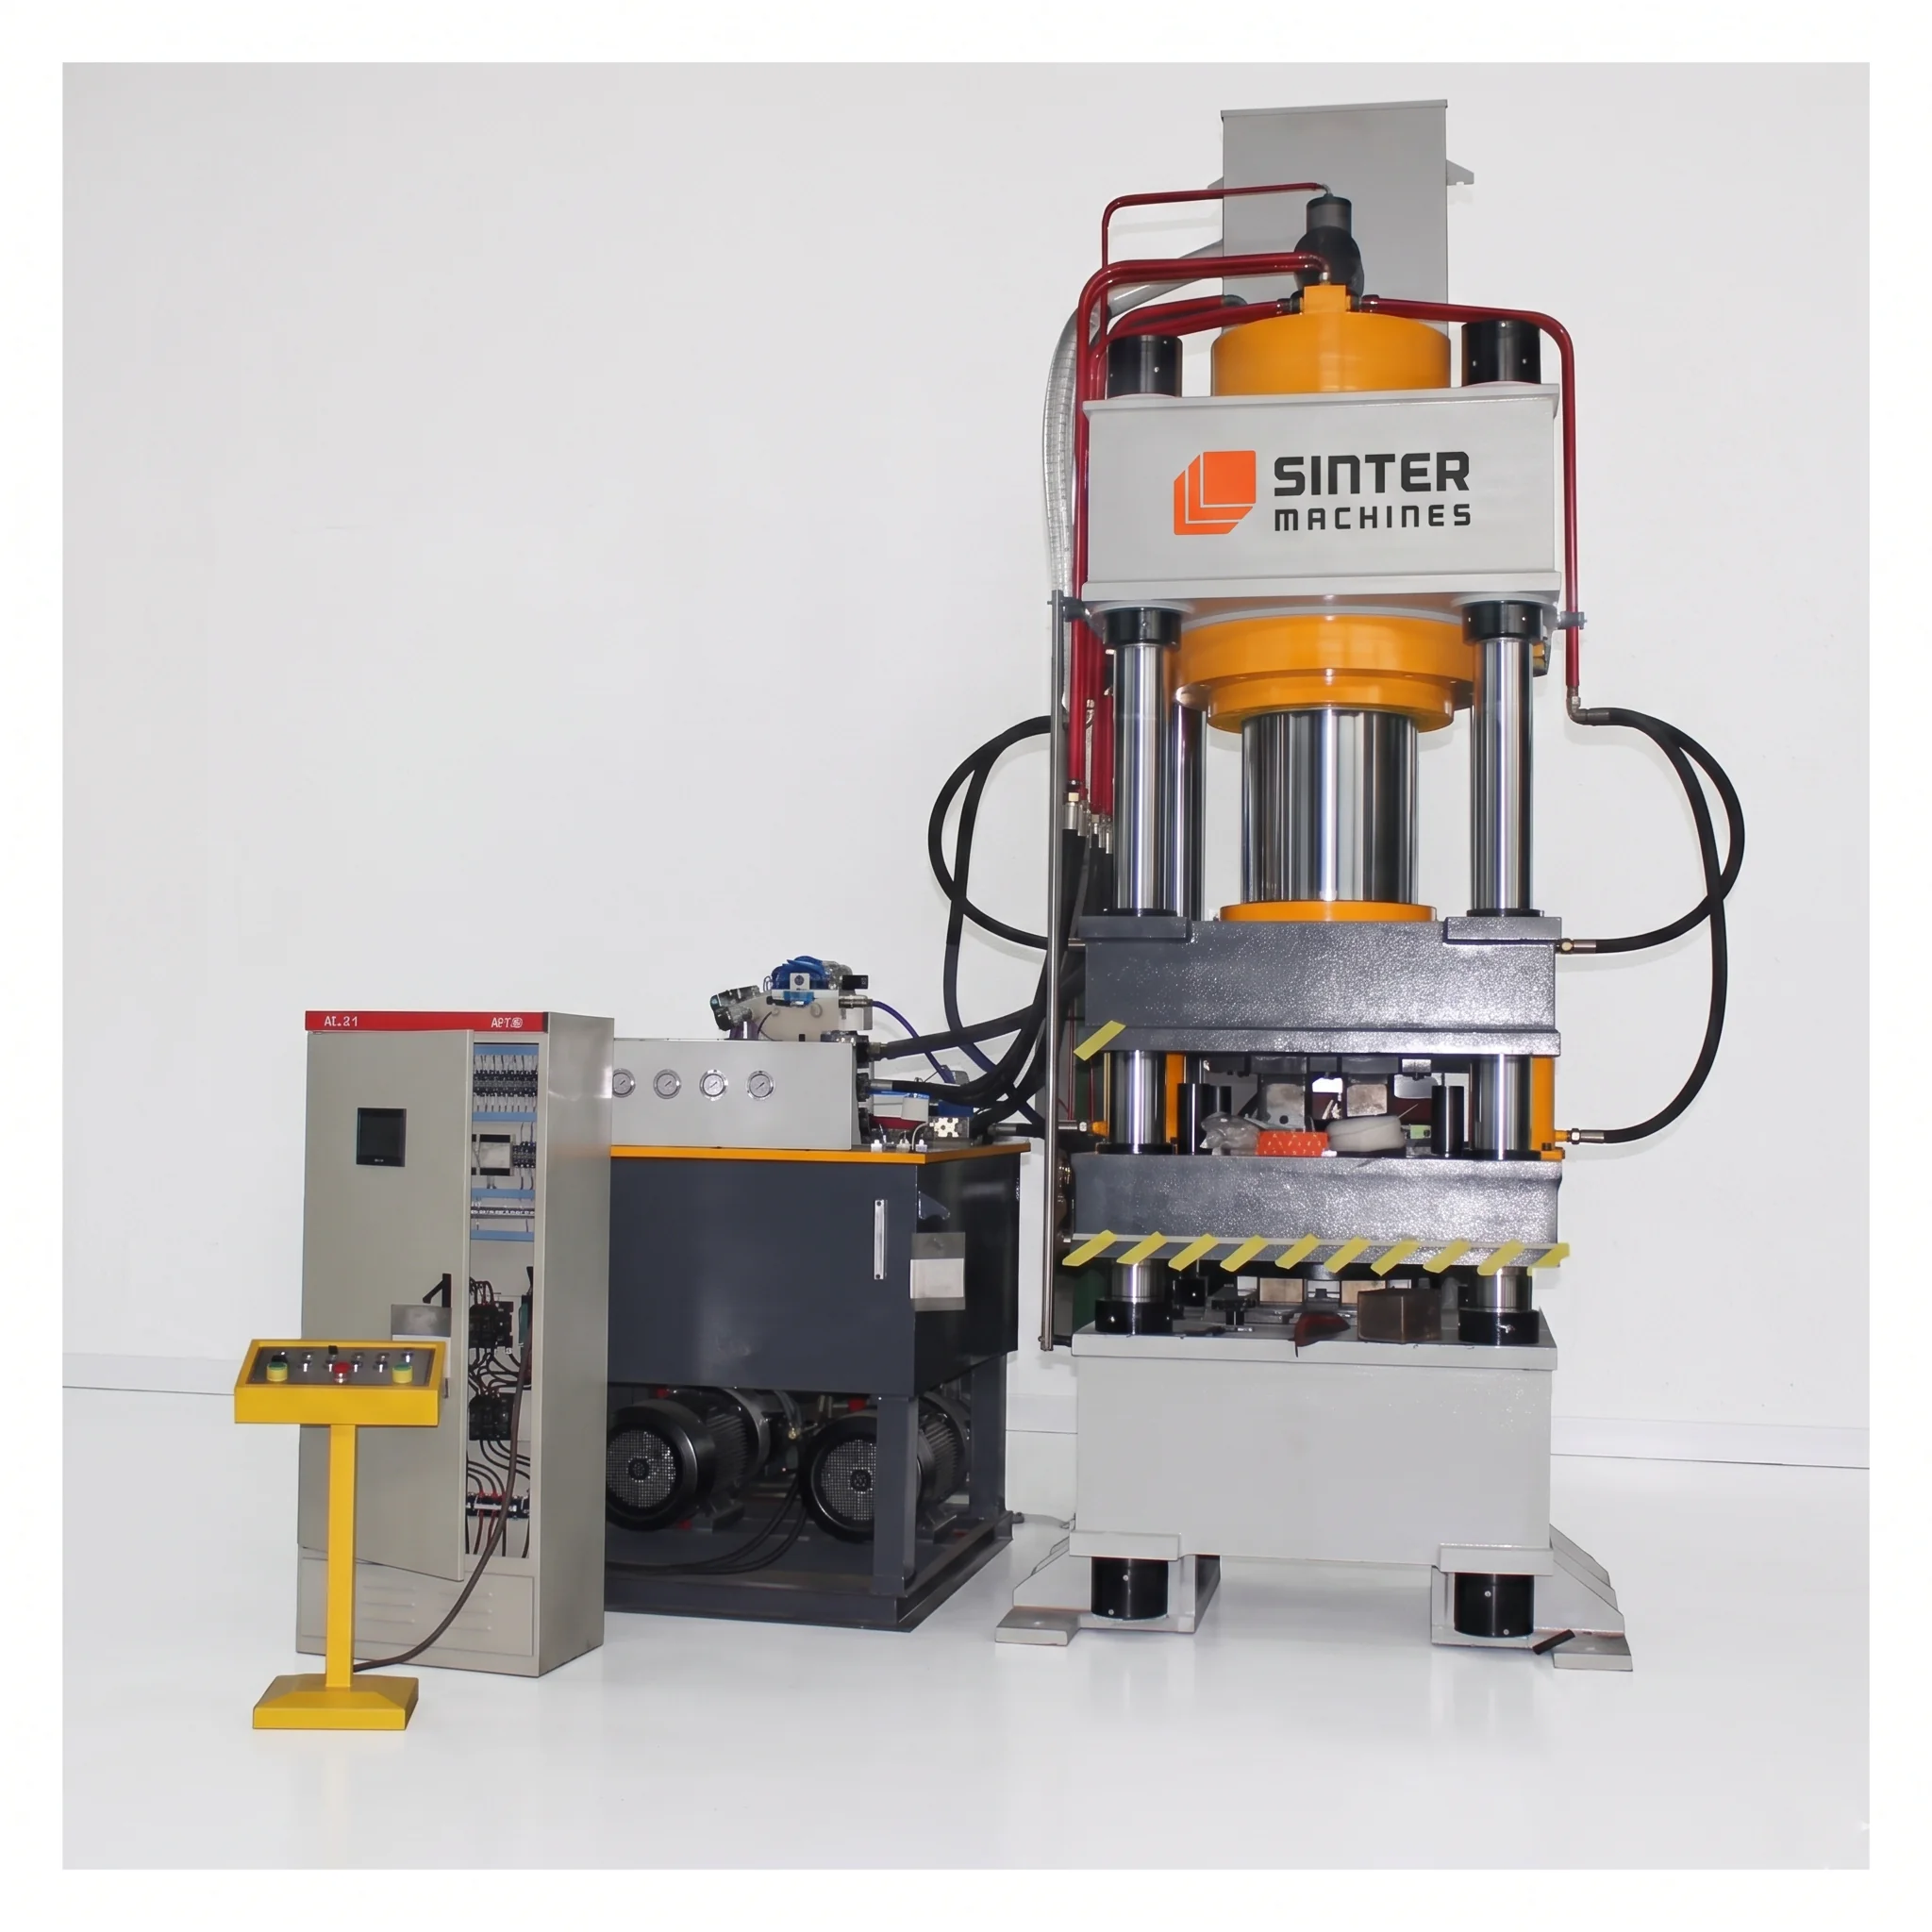
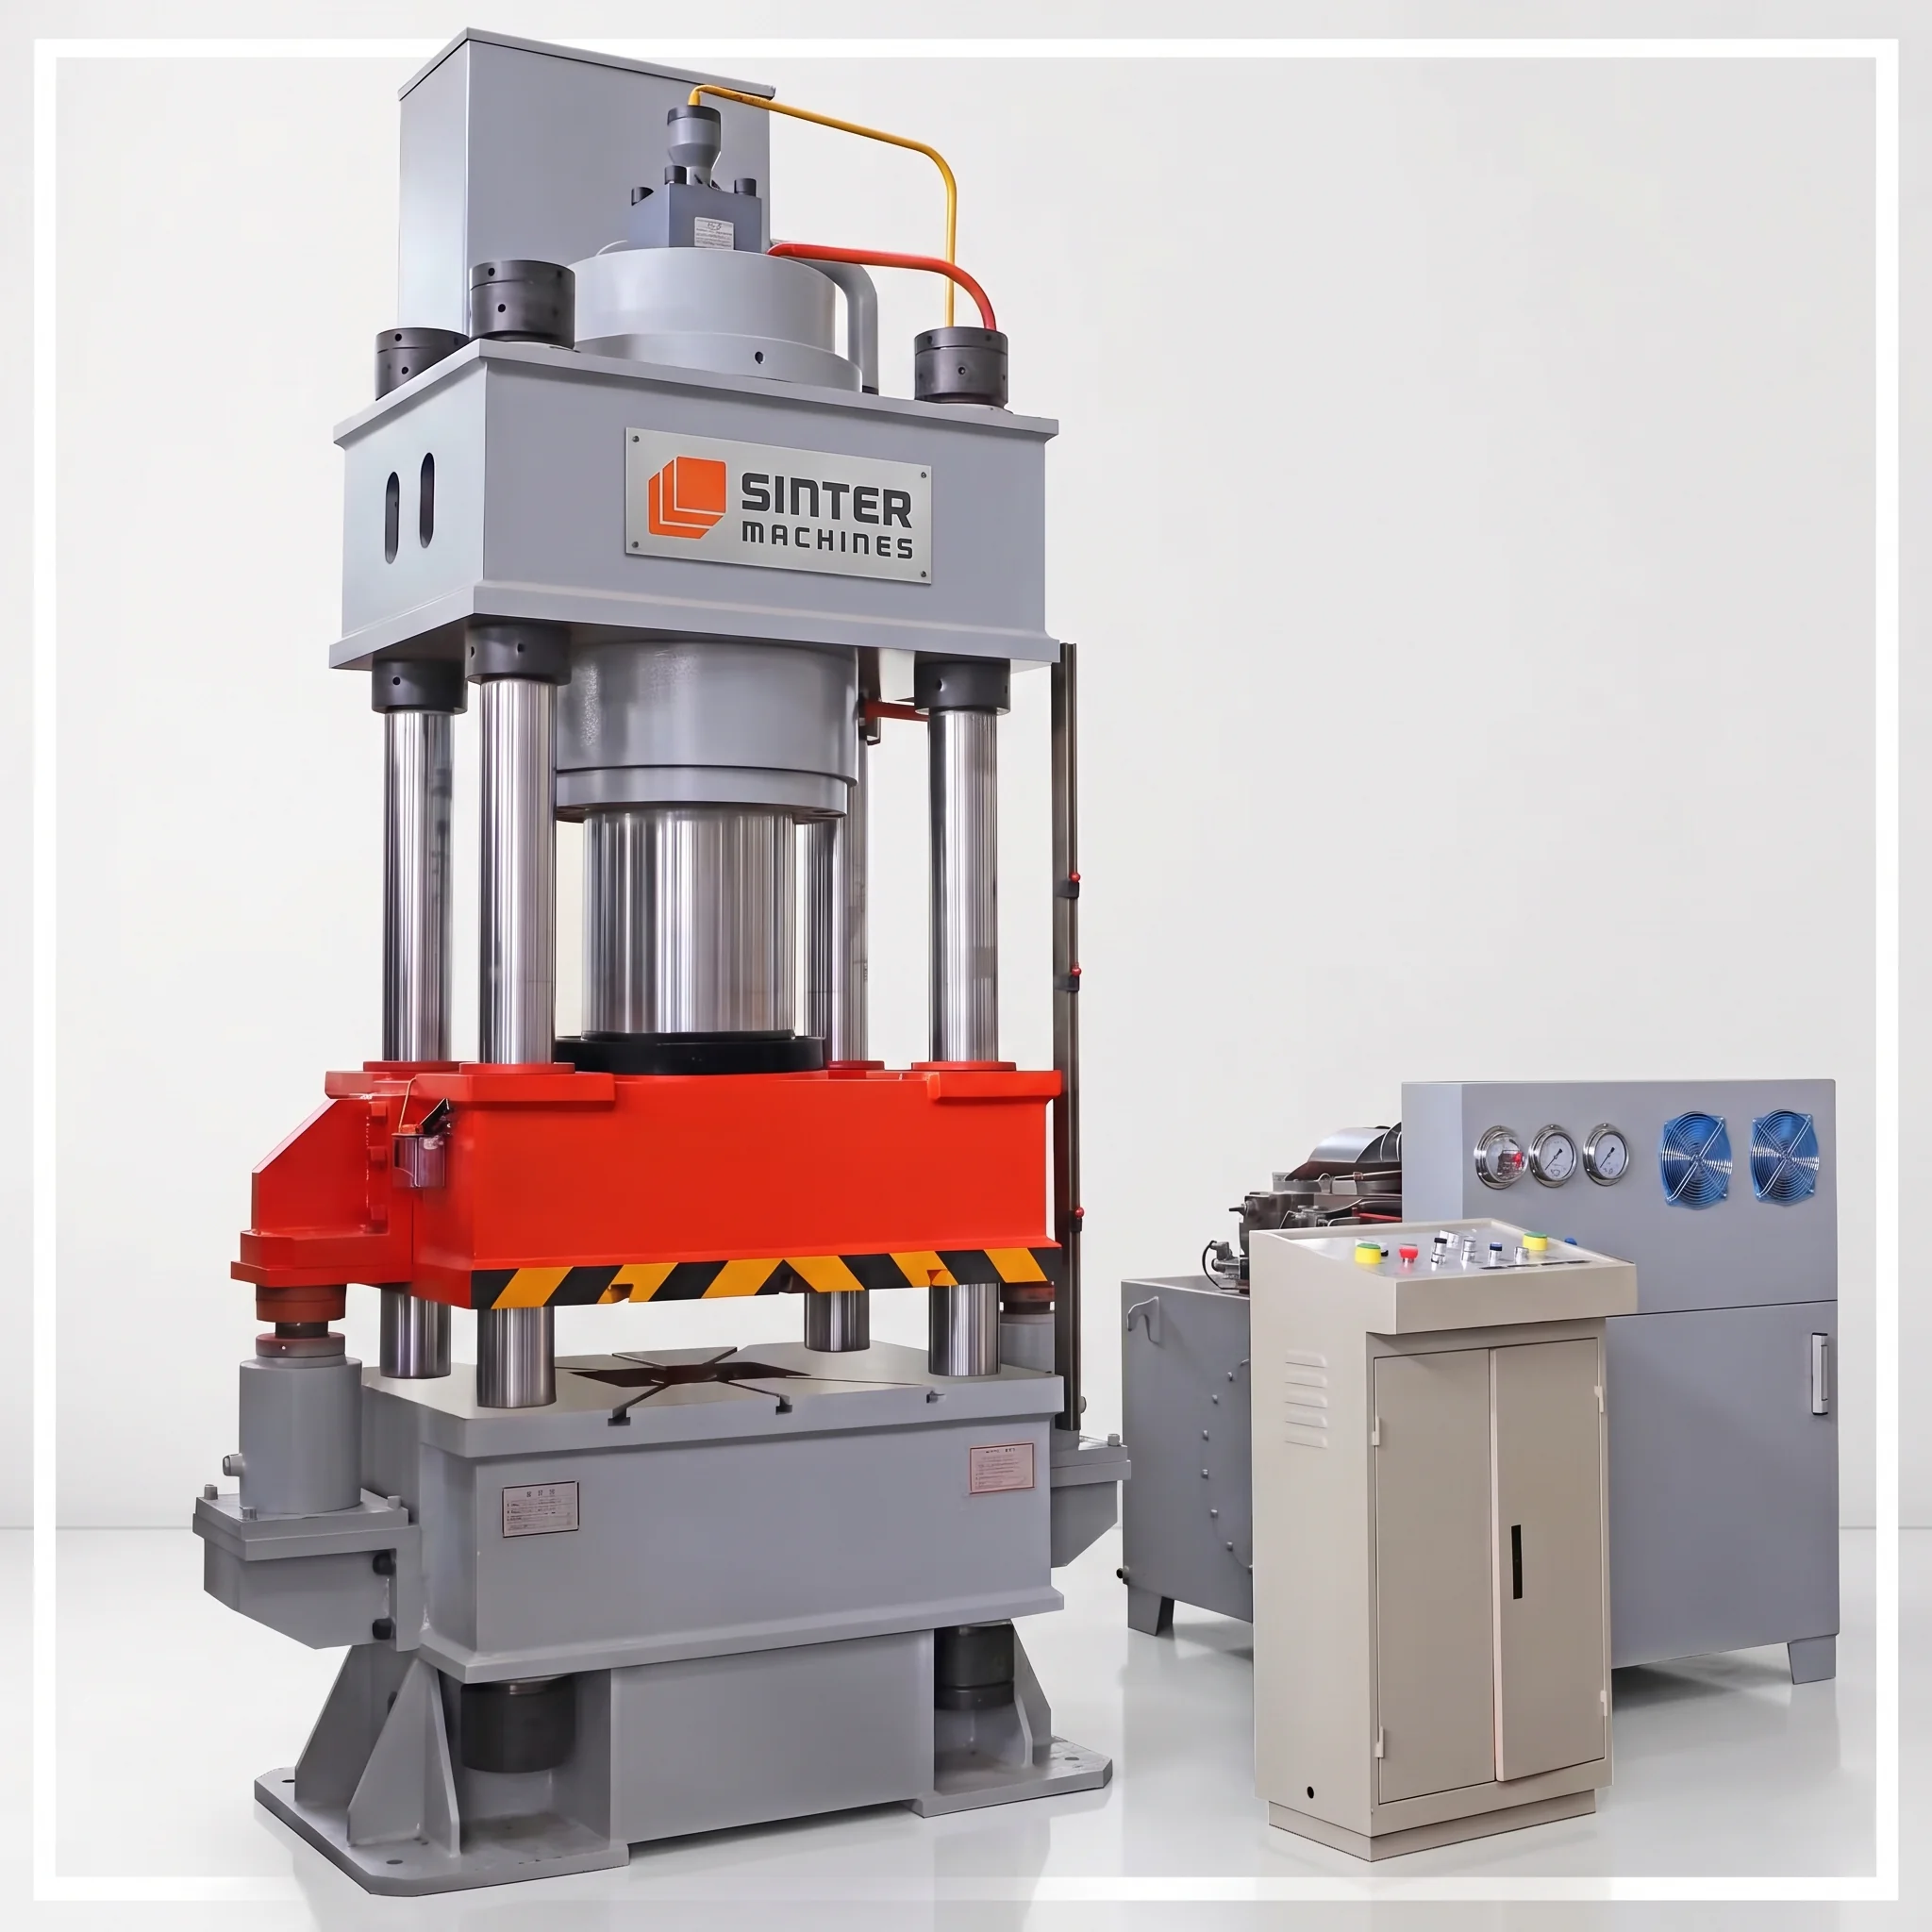
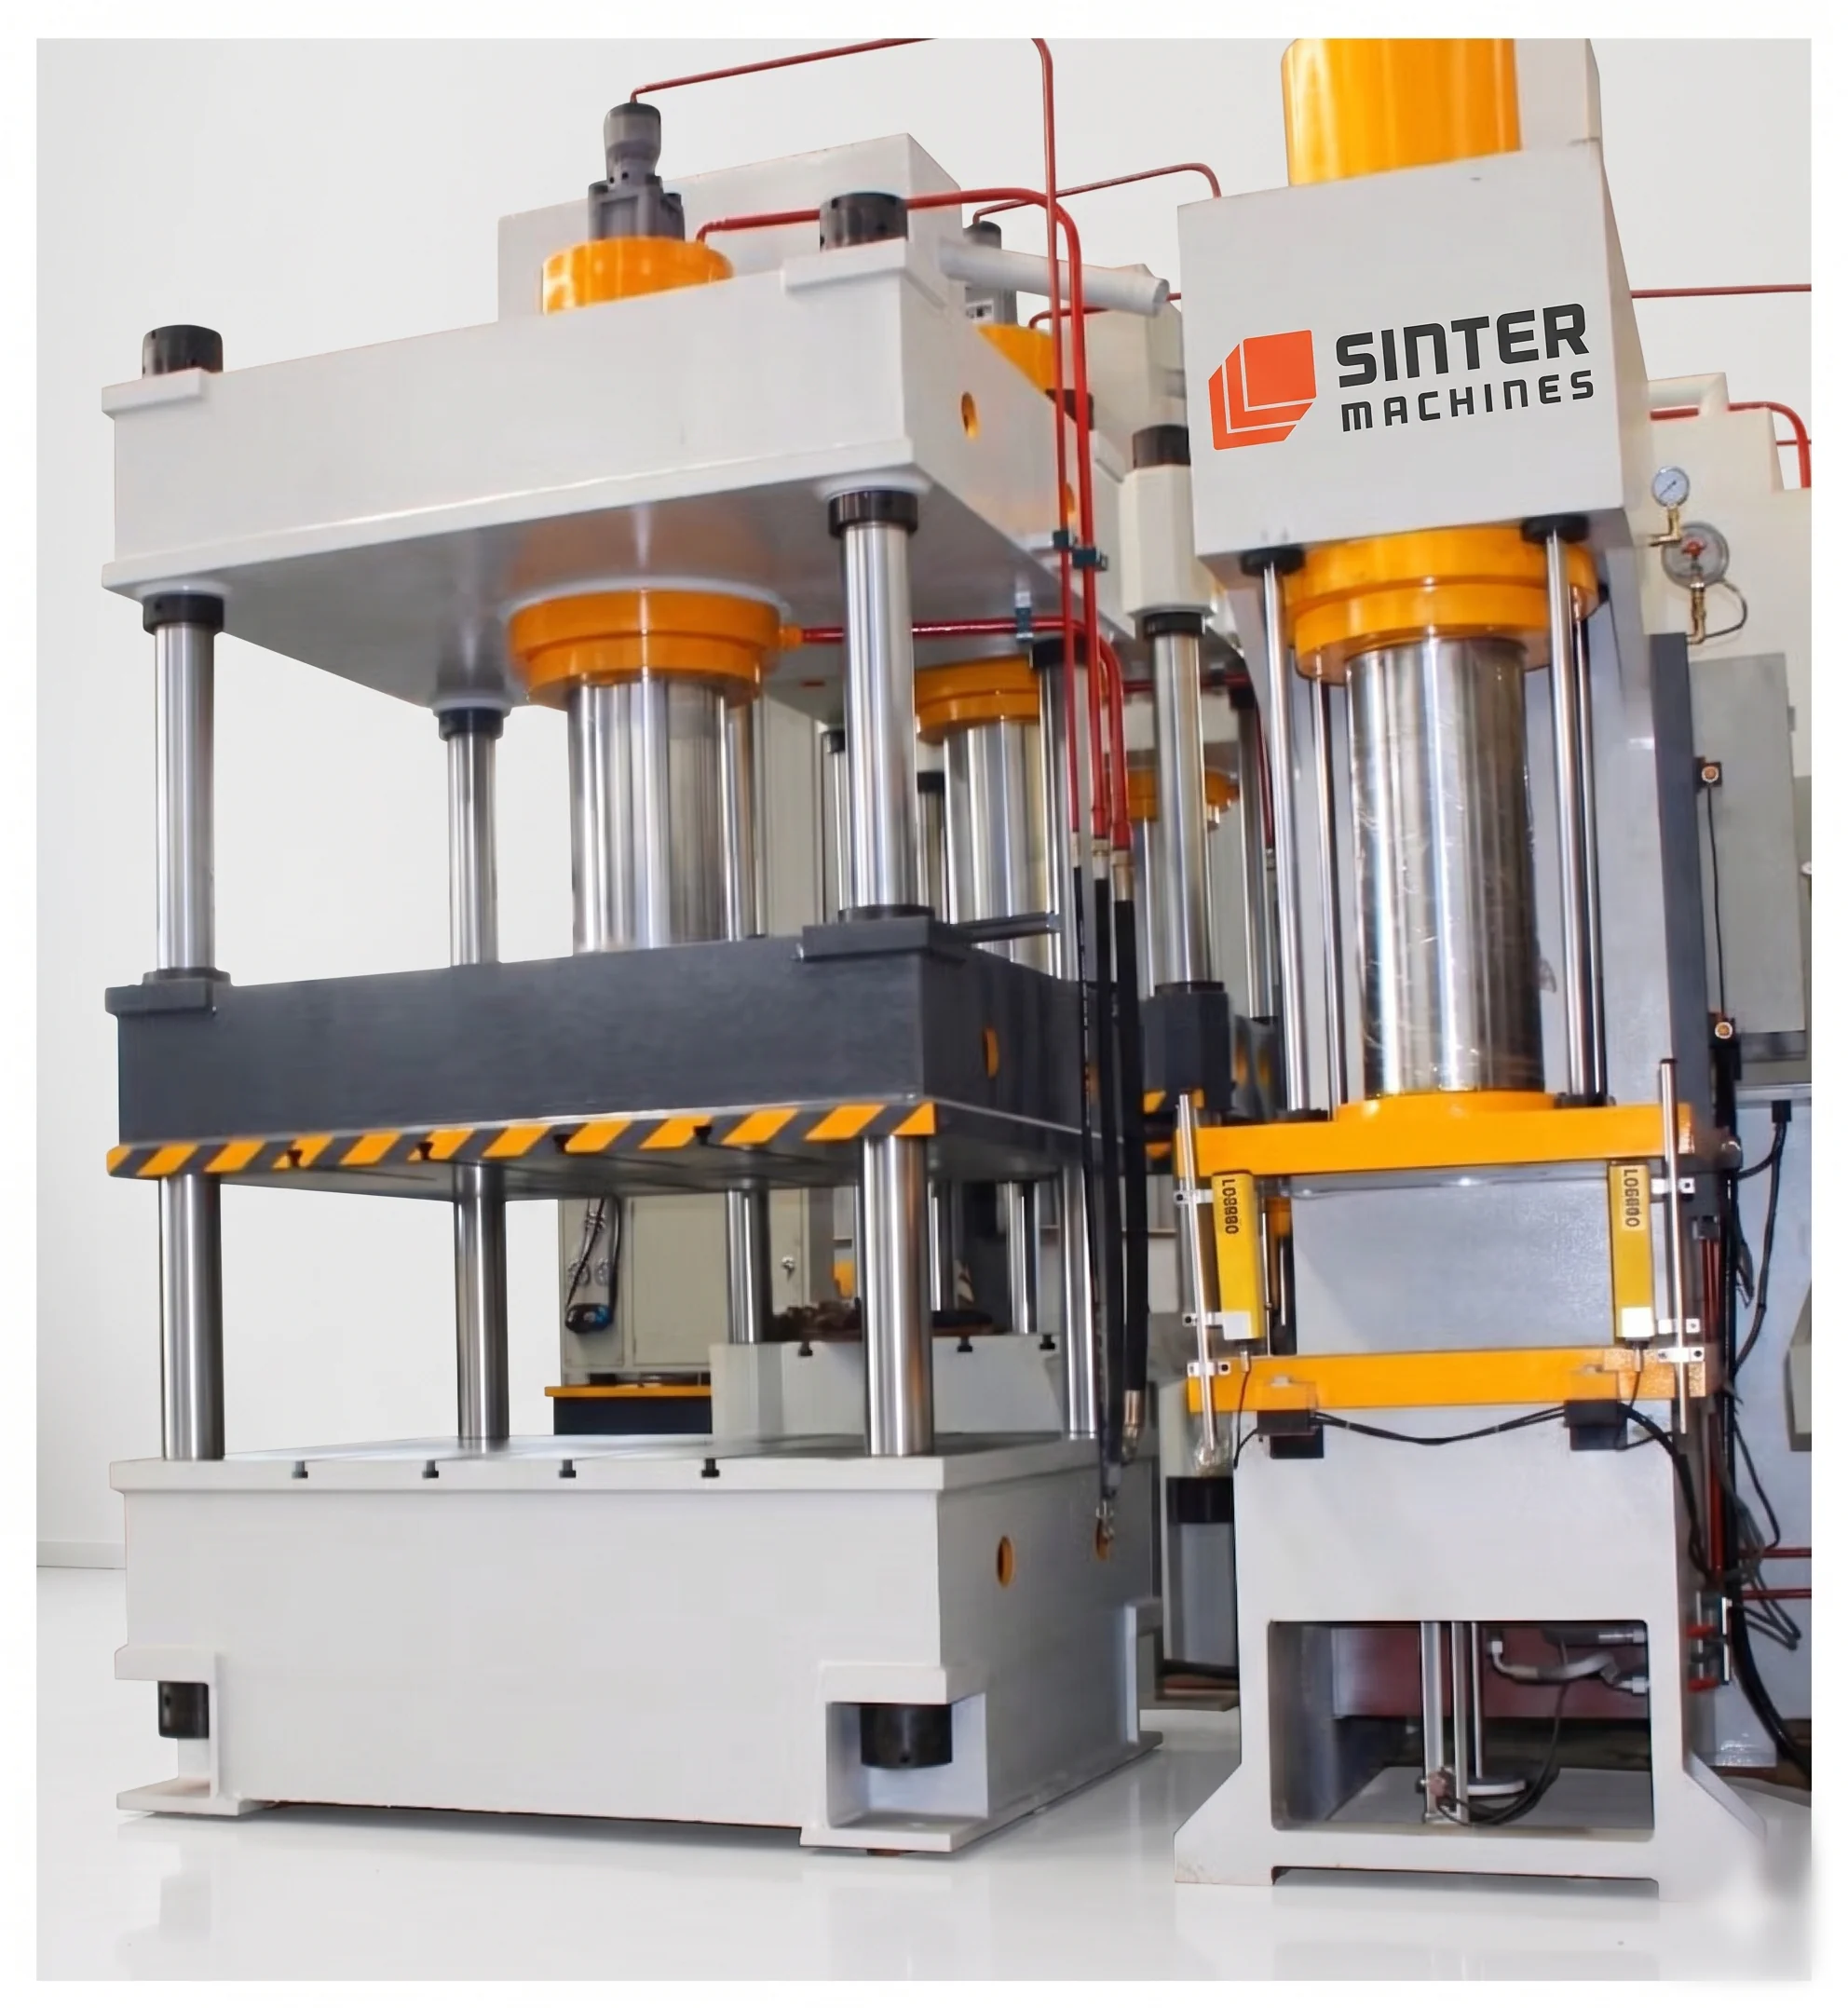
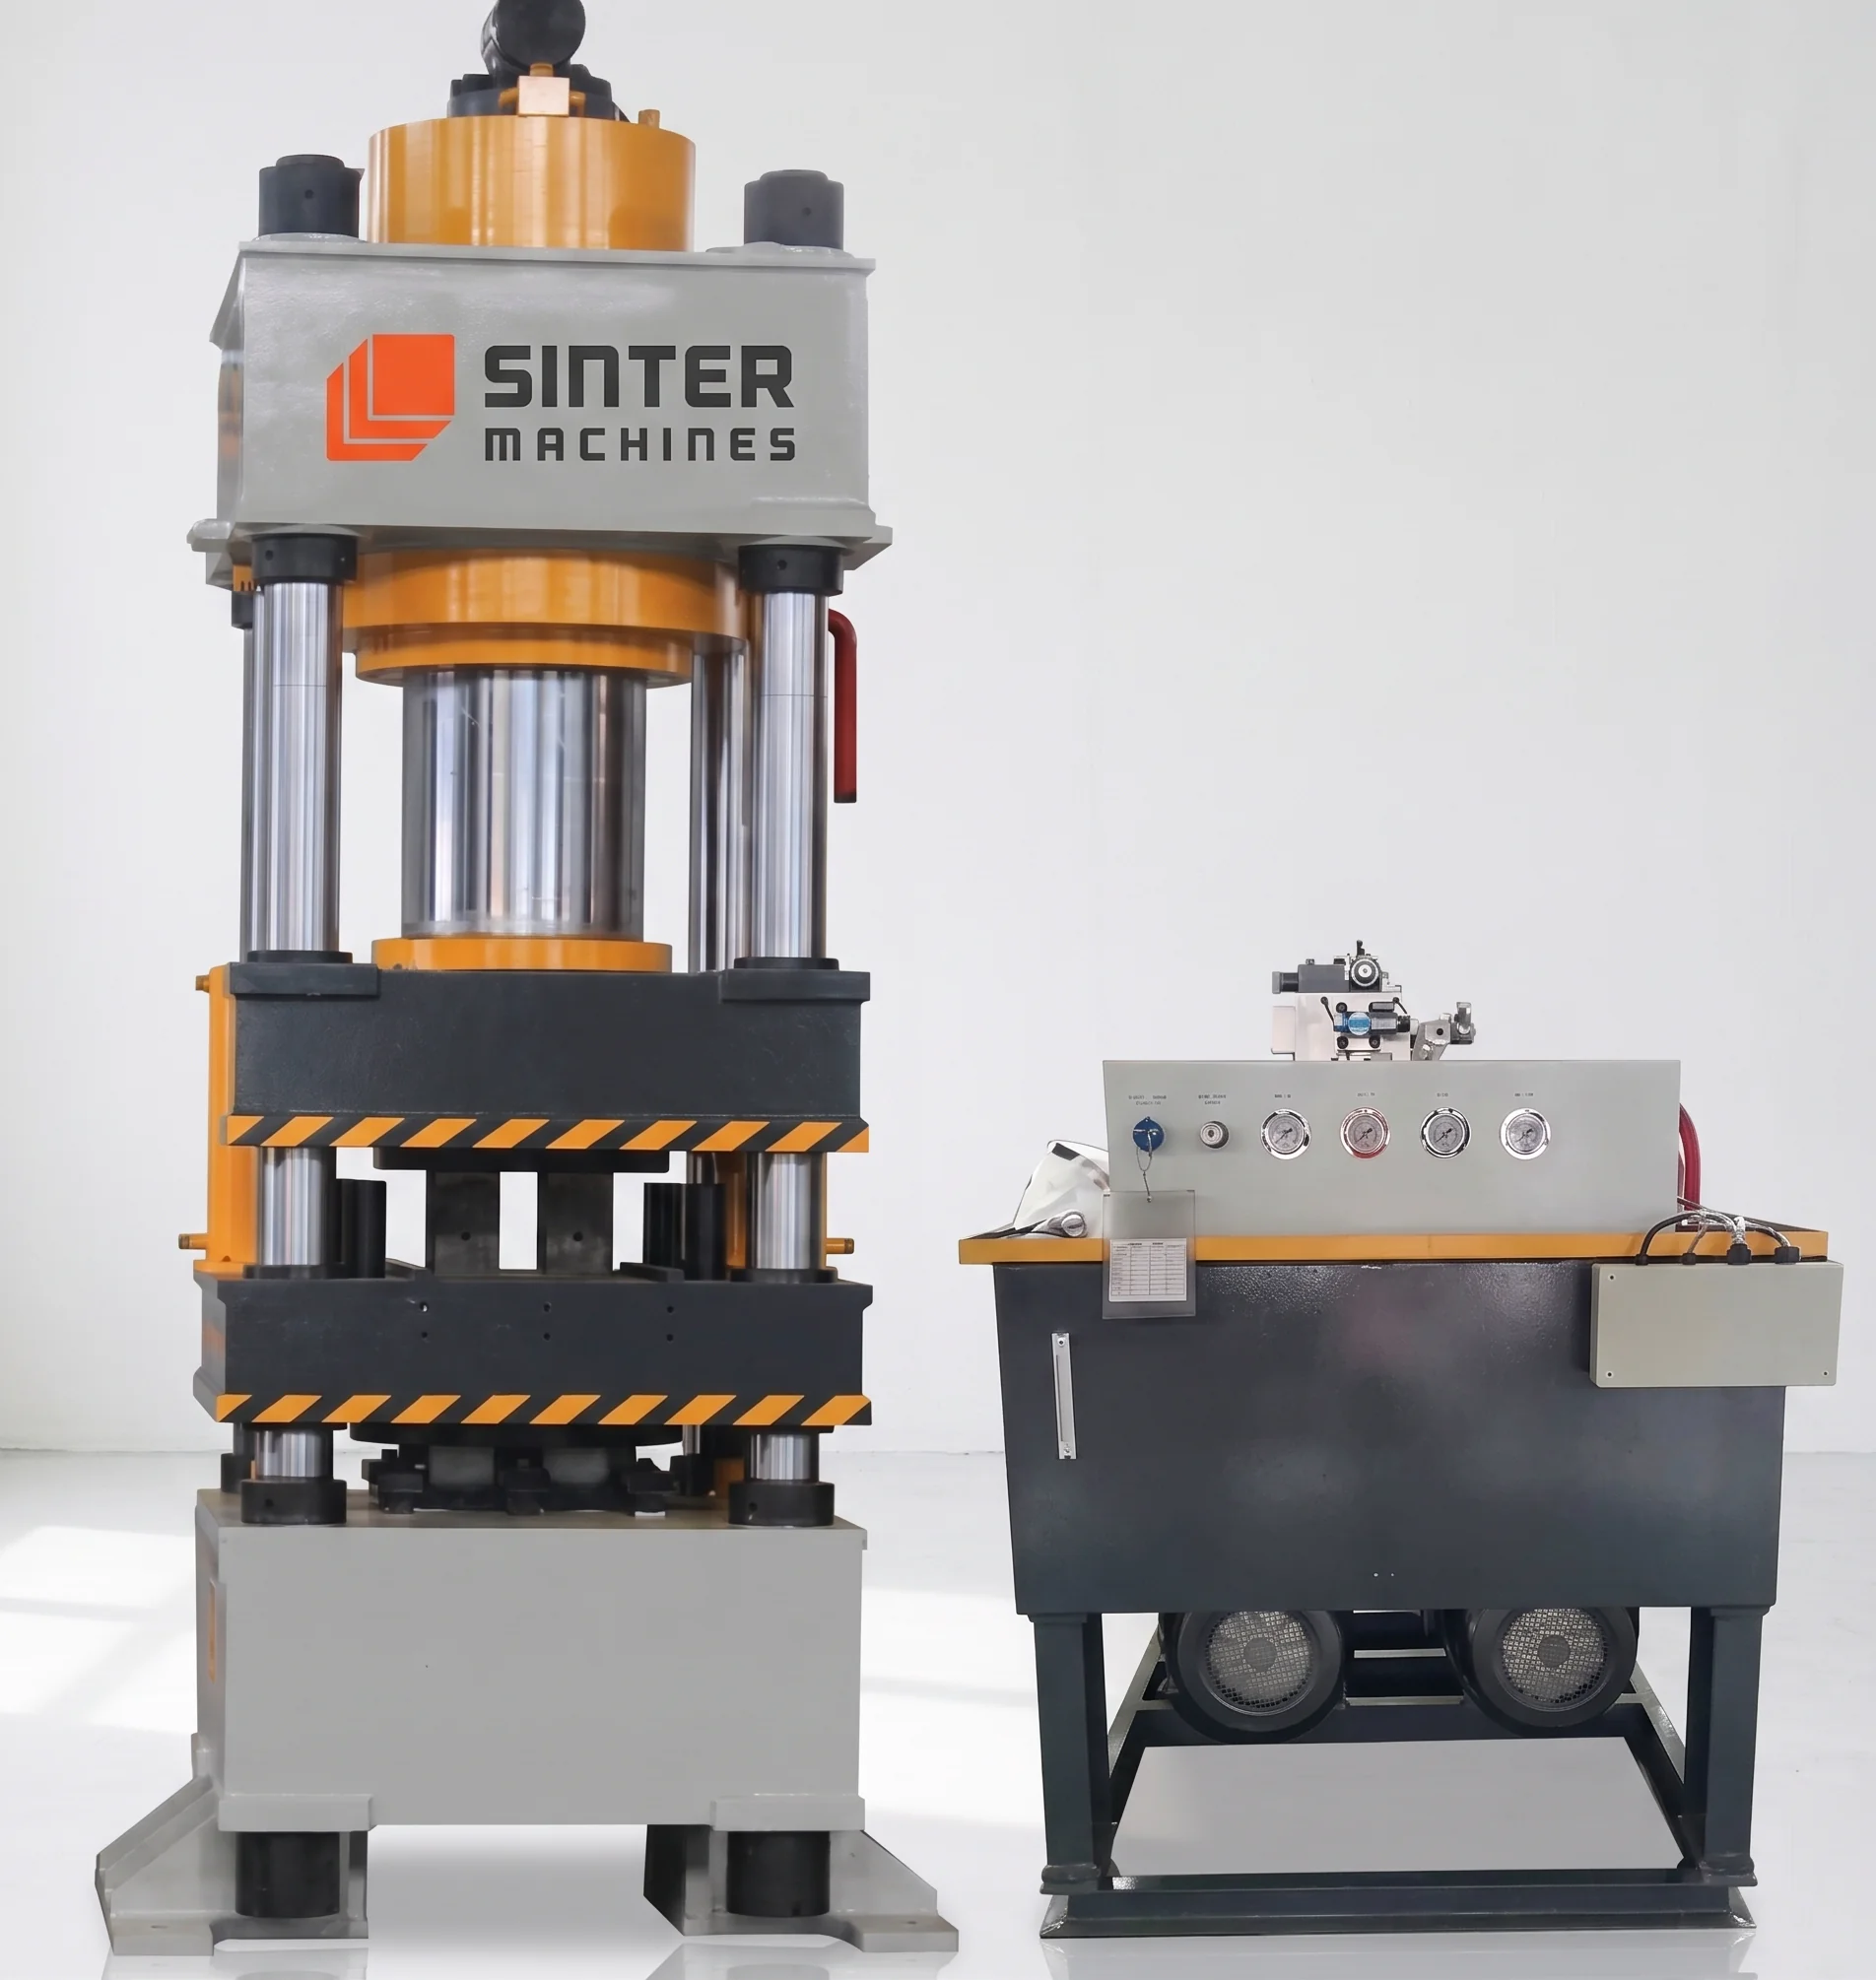
1250 Ton Four Column Hydraulic Press Machine
The 1250-ton five-station four-pillar hydraulic press provides a high-performance, automated cold-forging platform engineered for heavy-duty sleeve drivers used across industrial and automotive sectors. This advanced multi-station system enables high-volume manufacturing with exceptional geometric accuracy, extended tooling life, and minimal post-process machining.
Use Case
Sleeve drivers serve as critical force-transmitting components required to install bearings, bushings, and seals precisely without causing surface damage or misalignment. The 1250-ton press uses progressive room-temperature extrusion to consolidate the material structure, ensuring high concentricity, uniform wall thickness, and elevated fatigue resistance.
Core Applications
- Multi-station progressive cold extrusion, forward-backward extrusion, and upsetting of heavy-duty driver sleeves
- High-tonnage sizing and calibration of thick-walled hollow cylindrical installation tools
- High-volume automated production of near-net-shape rotating and load-bearing drive sleeves
Material
- Premium cold-heading carbon steels and high-tensile alloy case-hardening forging steels
- Chromium-molybdenum structural steels optimized for high-pressure material consolidation
- High-strength alloy wire rods and pre-cut solid billets for extreme load-bearing applications
Typical Products Processed
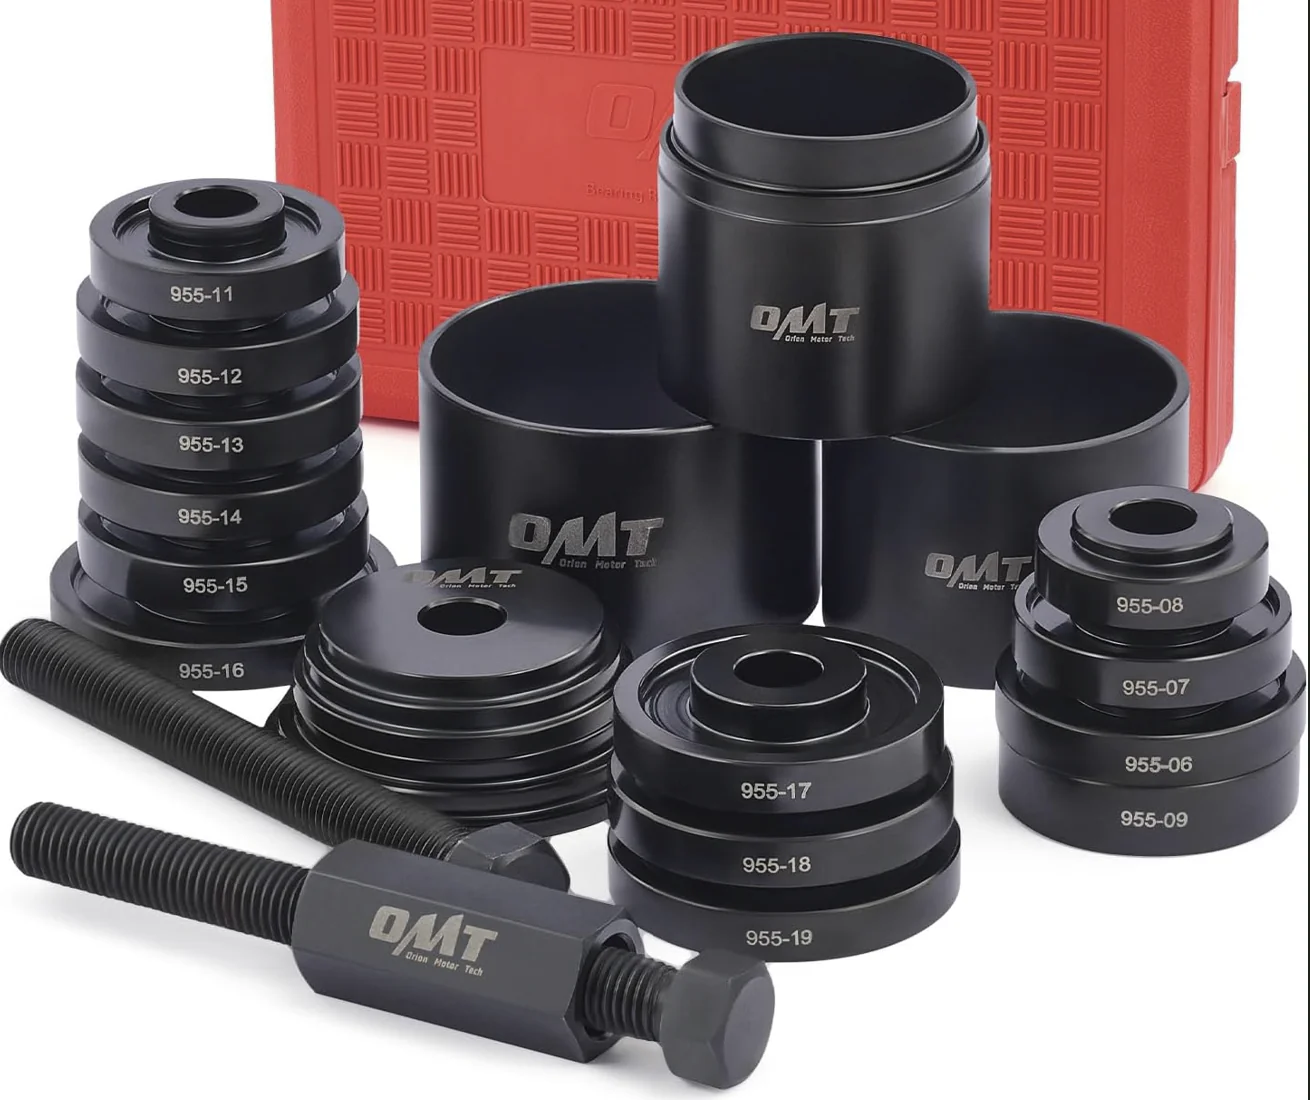
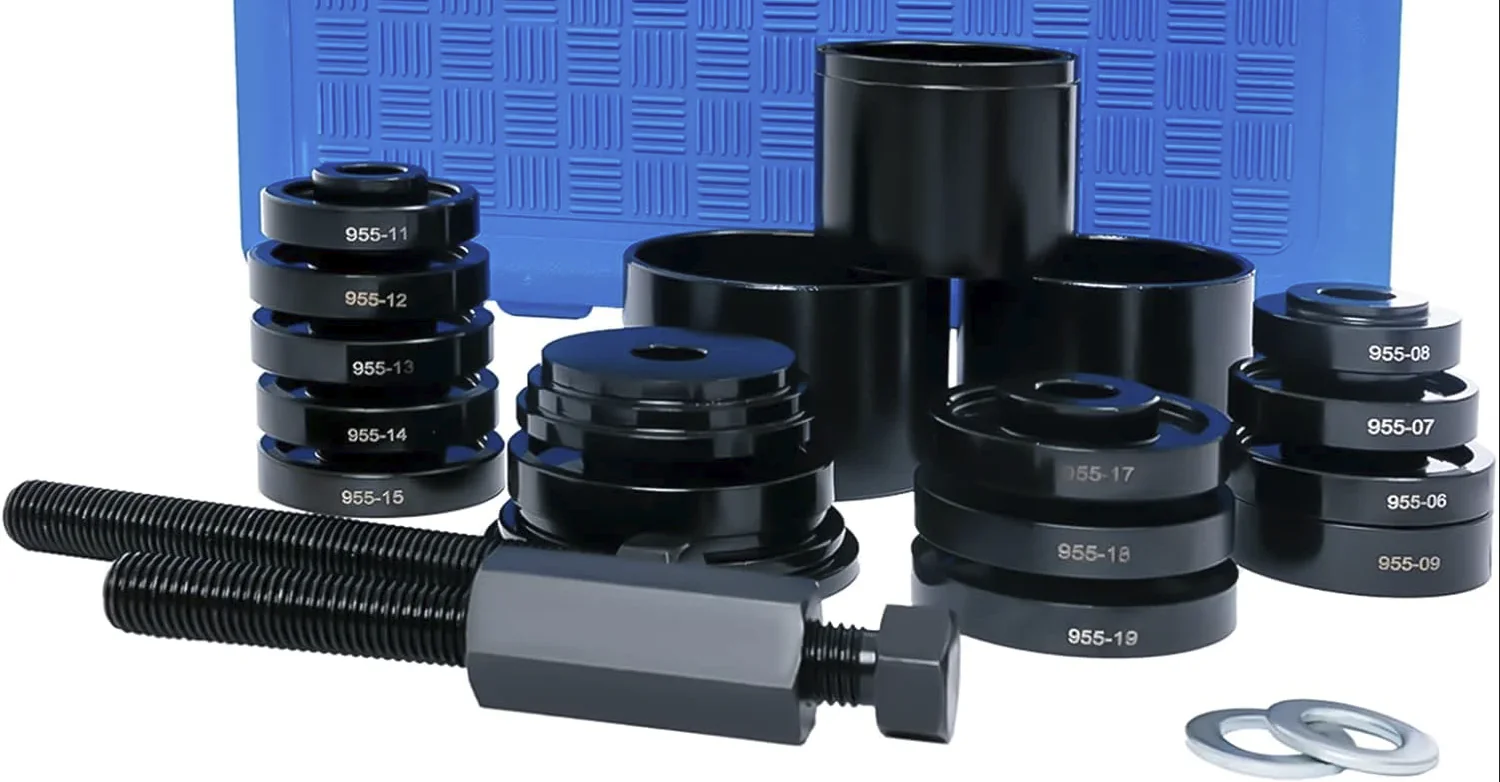
- Automotive bearing and seal installation sleeve drivers
- Heavy-equipment drive sleeves, splined couplings, and transmission adapters
- Industrial machinery shaft driver sleeves, spacer rings, and alignment collars
- Precision multi-stepped hollow driver shells and load-transfer socket sleeves
Key Functions
- Multi-station progressive transfer handling for continuous, multi-step forming sequences
- Variable velocity stroke profiling to manage material displacement and avoid internal stress cracks
- Integrated multi-stage hydraulic bottom ejection system for synchronized part stripping across all stations
- Digital position transducers and continuous tonnage monitoring for absolute batch-to-batch repeatability
Why 1250 Ton Hydraulic Press?
- Delivers massive forming tonnage across five progressive stations to cold-forge heavy, thick-walled steel sleeves in a single continuous line
- Four-column pre-stressed frame architecture absorbs extreme off-center loading during progressive extrusion, maintaining strict die alignment and wall concentricity
02 — Technical Specifications
SM 1250 HP – HYDRAULIC PRESS MACHINE COMPLETE TECHNICAL DATA
The SM 1250 HP hydraulic press delivers high-tonnage compression forces and micro-precise multi-station alignment tracking optimized for cold forging heavy sleeve drivers. Its rigid four-column structural framework and responsive fluid circuits ensure continuous high-volume output with strict geometric concentricity.
Capacity
- Maximum continuous cold forging compression force capacity of 12500 kN
- Dedicated high speed multi station hydraulic ejector stripping force capacity of 800 kN
Structural Design
- High fatigue resistant pre stressed four column configuration built for heavy continuous industrial production
- Finite element analysis structural simulation frame designed to absorb extreme off center multi station forming stresses
Frame Type
- Precision aligned solid induction hardened pillar frame guide structure
- Stress relieved heavy welded steel plate bolster and upper moving slide assembly
Hydraulic System
- High output variable displacement axial piston pump fluid power assembly
- Multi stage high capacity offline oil filtration loop with integrated oil coolers
Main Ram Stroke
- Maximum vertical slide forming travel distance capability of 500 mm
- Electronic stroke length limitation positioning resolution accurate within 0.005 mm
Working Hydraulic Pressure
- Maximum continuous operating main hydraulic system fluid pressure of 280 bar
- Peak shock safety valve pressure relief calibration threshold limit of 310 bar
Daylight Gap
- Maximum open vertical daylight window working clearance of 1000 mm
- Minimum closed shut die height tool workspace space of 450 mm
Approach Speed
- Accelerated downward advance slide rapid travel speed of 350 mm/Sec
- Controlled raw material tool engagement deceleration velocity of 8 mm/Sec
Pressing / Drawing Speed
- Dynamic high pressure cold forging extrusion speed of 2 to 22 mm/Sec
- Maximum resistance continuous metal displacement squeezing velocity of 30 mm/Sec
Return Speed
- High speed upward ram extraction retraction travel speed of 320 mm/Sec
- Ultra fast automated hydraulic pre return system decompression cycle timing
Bed / Platen Size Platen
- Total clear bolster bed width left to right of 1400 mm
- Total clear bolster bed depth front to back of 1100 mm
Columns
- Ultra high tensile forged alloy steel pillar diameter of 250 mm
- Heavy duty wear resistant bronze guide bushings with automatic grease lubrication
Working Envelope
- Total horizontal internal clear workspace area of 1400 by 1100 mm
- Maximum permissible upper die tool assembly mass weight of 6000 kg
Control System
- Industrial programmable logic controller linked with a graphical touchscreen station
- Dual redundant non contact linear transducer position tracking systems accurate within 0.002 mm
Main Motor Power
- High efficiency primary hydraulic pump electric drive motor power of 110 kW
- Dedicated auxiliary cooling and continuous oil filtration motor power of 7.5 kW
Valves & Hydraulics
- High dynamic response proportional servo flow control cartridge manifold block
- Integrated fast acting overhead gravity pre fill oil valve unit assembly
Automation
- Integrated five station automatic mechanical transfer arm linkage system
- Digital interface connection ports for synchronized industrial automatic feeder loops
Safety Features
- Dual channel infrared light curtain barriers guarding operator workspace zones
- Automated heavy duty dual fail safe mechanical anti drop ram safety locking blocks
SM 1250 HP — Model Specifications
- Nominal Force: 16000 KN
- Maximum Hydraulic Pressure: 25 MPa
- Max Opening Height of the Slider: 1500 mm
- Max Stroke of the Slider: 900 mm
- Effective Bed Size: 1600 × 1600 mm
- Slider Down Speed: 180 mm/s
- Slider Pressing Speed: 6–15 mm/s
- Slider Return Speed: 200 mm/s
- Ejector Cylinder Nominal Force: 600 KN
- Stroke of the Ejection Cylinder: 300 mm
03 — Die / Mold System
Precision Cold Forged Precision Sleeve Drivers Die Mold Engineering
This multi-station progressive tooling system utilizes heavy-duty tungsten carbide matrix inserts housed inside pre-stressed alloy steel containment rings to withstand massive radial extrusion forces. The rigid tool construction restricts dynamic deflection during room-temperature forming, guaranteeing strict wall concentricity and bore geometry.
Technical Specifications (Tooling)
Die Type
- High precision five station progressive closed die cold heading and multi stage extrusion tool set assembly
- Heavy duty industrial grade cold forming tooling layout engineered for high volume sleeve driver and installation tool manufacturing
Die Materials
- Premium submicron grain tungsten carbide cobalt matrix inserts providing extreme compressive yield strength and abrasive wear resistance
- Ultra high strength chromium molybdenum vanadium hot work tool steel utilized for external pre stressed compression casings
Tool Configuration & Construction
- Multi layer interference fit shrink fitted container ring design engineered to counteract massive internal radial splitting stresses
- Modular quick change five station cassette layout optimized to minimize production line changeover times and maximize press bed utility
Key Tooling Features
- Synchronized multi station hydraulic knockout pin assembly designed for rapid automatic part ejection across all stations
- Precision machined internal relief air venting channels engineered to prevent oil entrapment and avoid pneumatic pressure locks
Alignment Accuracy
- Upper punch and lower die axis concentricity deviation kept strictly under a limit of 0.015 mm
- Moving slide guiding parallelism variance across the active workspace restricted within a tolerance of 0.008 mm
Process Materials
- Premium cold heading carbon steels high tensile alloy case hardening forging stocks and chromium molybdenum structural steels
- High strength alloy wire rods and pre cut solid alloy steel billets matching strict mechanical sleeve performance standards
Surface Finish
- Active mirror polished tungsten carbide forming cavities diamond lapped down to an roughness of Ra 0.04 microns
- Advanced physical vapor deposition titanium aluminum nitride wear protective surface layer applied to a thickness of 0.003 mm
Tool Life
- Expected production span of 35000 cycles per station before requiring mandatory cavity inspection and micro polishing procedures
- Total structural tooling lifespan capacity reaching 350000 production cycles before complete carbide insert replacement
Precision Cold Forged Precision Sleeve Drivers Die Mold
04 — Product Application
Where Precision Cold Forged Precision Sleeve Drivers Are Used
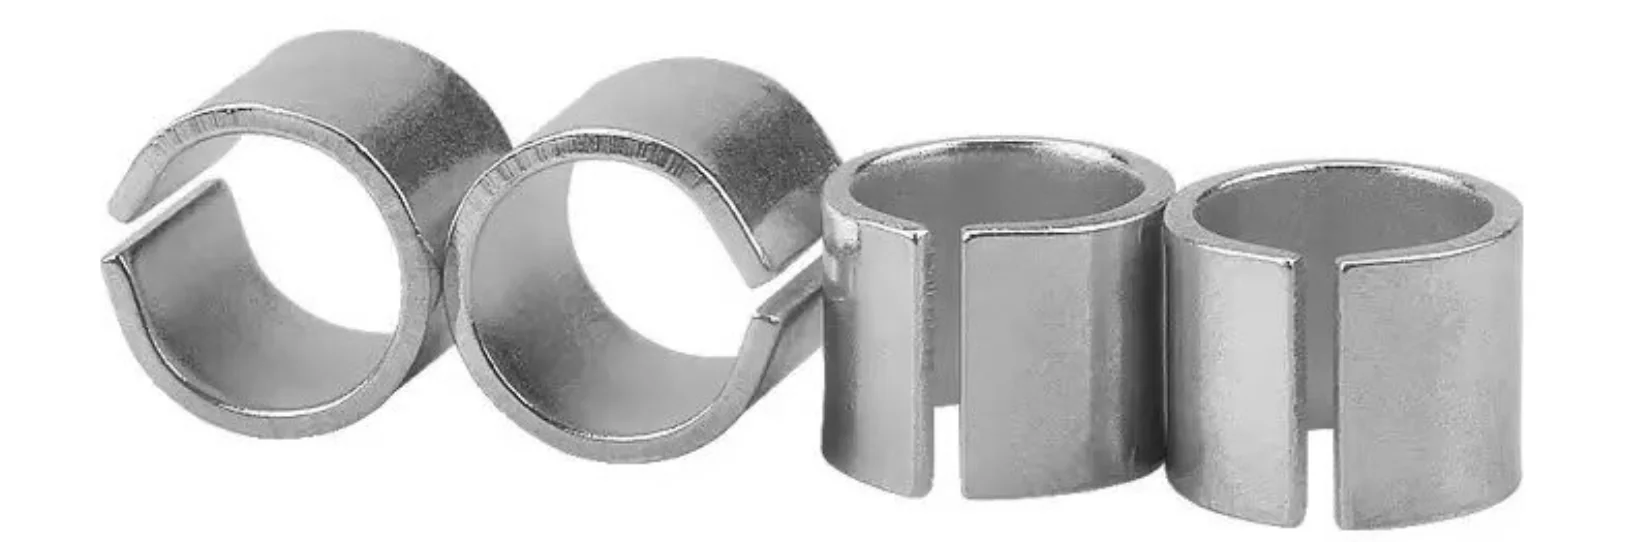
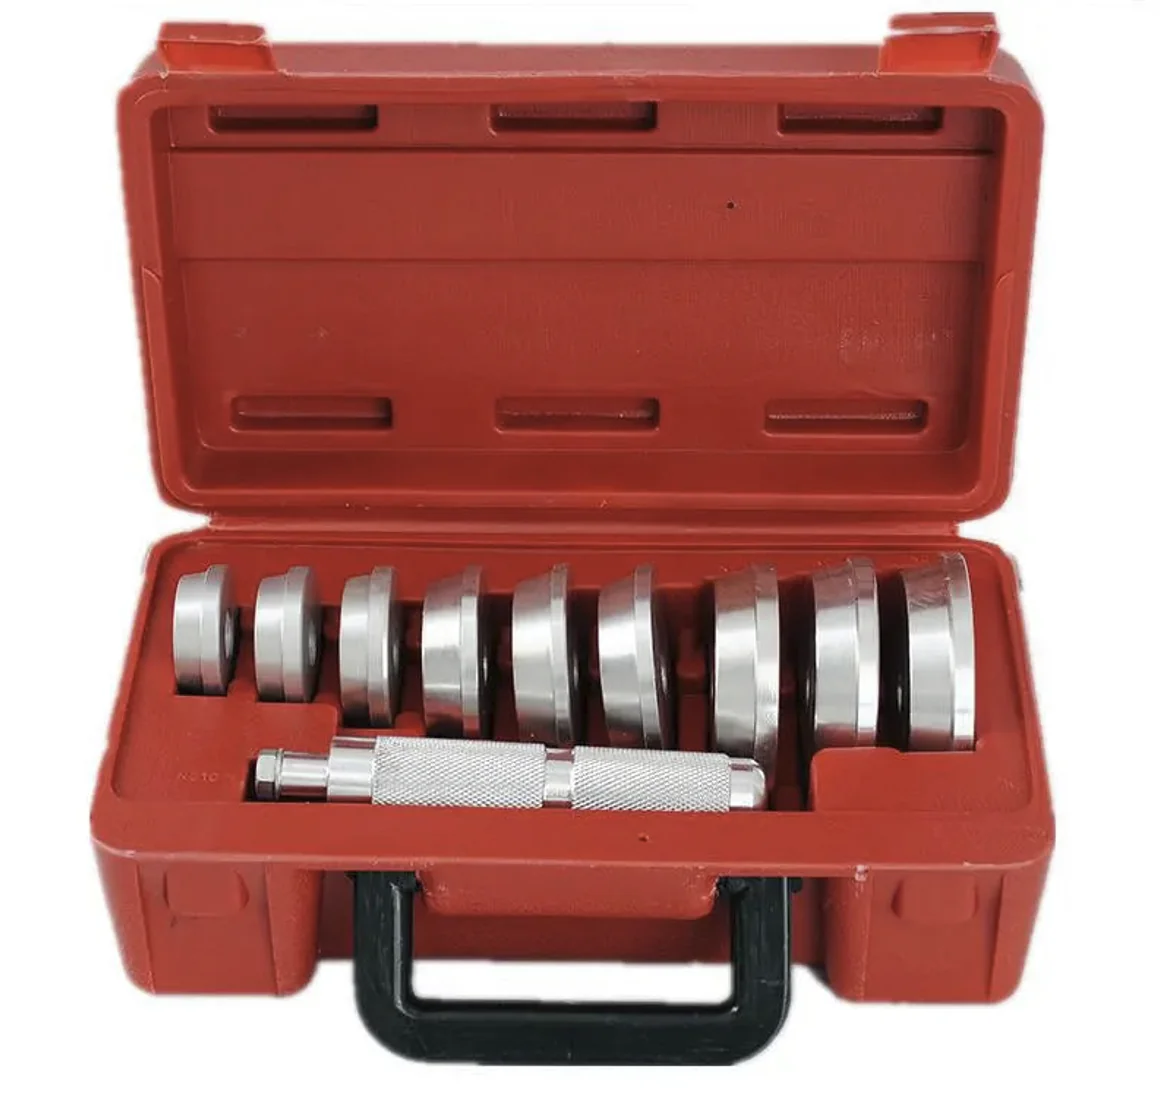
Precision cold-forged sleeve drivers act as specialized force-transmitting adapters used to install bearings, bushings, and oil seals without damaging sensitive mating faces. These high-density steel components deliver extreme concentricity, high wear resistance, and flawless alignment under heavy axial impact loading during press-fit operations.
Industry Applications
Precision sleeve drivers are extensively utilized across automotive assembly lines, heavy equipment manufacturing, electric motor production, and aerospace maintenance facilities. Their work-hardened material density, low surface roughness, and high concentricity allow Tier-1 component manufacturers and OEMs to achieve zero-defect press-fitting, reduce tool turnover costs, and protect critical assembly interfaces during high-speed production.
Automotive Drivetrain and Assembly Lines
Used in high-speed automated production cells to press bearings, needle rollers, and seals accurately into transmission housings and wheel hubs. The dense, cold-forged steel structure absorbs repeated high-tonnage impacts without cracking, maintaining precise seating depth and preventing seal distortion.
Heavy Earthmoving and Construction Equipment Manufacturing
Deployed to drive thick-walled pivot bushings, kingpin sleeves, and track linkage collars into heavy structural chassis frames. Superior surface hardness prevents scoring or deformation under massive axial mounting pressures, ensuring long-term bearing alignment in severe field environments.
Industrial Machinery and Electric Motor Production
Utilized in automated press cells for installing precision armature shaft bearings, sleeve bearings, and alignment collars. Exceptional dimensional accuracy ensures absolute concentricity during insertion, eliminating rotational runout and premature mechanical wear in motor assemblies.
Aerospace and Precision Energy Equipment Maintenance
Applied in maintenance, repair, and overhaul facilities for installing tight-tolerance turbine shaft sleeves and high-pressure fluid valve seals. Near-net-shape manufacturing provides flawless working face parallelism, guaranteeing uniform pressure distribution and preventing damage to expensive mating components.
Finished Product Gallery
05 — Key Advantages
Why Choose the 1250-Ton Sinter Hydraulic Press
The 1250-Ton Sinter Hydraulic Press provides the high-tonnage stability and multi-station precision needed to manufacture heavy-duty sleeve drivers. Its rigid four-column architecture and automated transfer capabilities enable seamless multi-stage progressive cold forging, maximizing output while maintaining strict wall thickness concentricity.
Technical & Commercial Benefits
High Tonnage Output Engineered for Heavy Wall Cold Extrusion
The robust fluid power delivery generates the intense pressure needed to deform thick-walled steel billets at room temperature. Inducing deep, uniform material flow consolidates the internal grain matrix to achieve extreme axial load capacity in finished components.
Heavy-Duty Four-Column Structure Resisting Multi-Station Load Deflection
The pre-stressed pillar configuration effectively counteracts heavy off-center loading generated across progressive multi-die stations. Eliminating frame flex protects expensive carbide tooling modules from uneven wear and maintains absolute bore-to-outer-diameter concentricity.
Integrated 5-Station Automated Transfer Integration for High Output
The synchronized mechanical transfer linkage rapidly advances components through progressive forming steps within a single continuous press cycle. Combining multiple cold heading, forward extrusion, and sizing operations into one line drastically reduces labor costs and cycle times.
Multi-Stage Speed and Pressure Profiling Eliminating Metal Fracture
Proportional hydraulic control allows precise throttling of material displacement velocities down to single millimeters per second. Regulating the deformation rate prevents internal shear cracking, reduces tool friction, and preserves high surface integrity across working faces.
Synchronized Hydraulic Ejector System Ensuring Clean Part Removal
A dedicated multi-station bottom knockout system exerts up to 800 kN of stripping force to instantly release tightly formed sleeves from deep die cavities. Immediate part removal prevents process stalling and enables seamless, high-speed automated line throughput.
Near-Net-Shape Process Yielding Substantial Raw Material Cost Savings
Forming heavy steel sleeves to near-final dimensions eliminates the heavy material loss typical of traditional lathe turning and deep boring. Maximizing raw stock utilization drives major cost efficiency when processing high-grade structural and alloy steels.