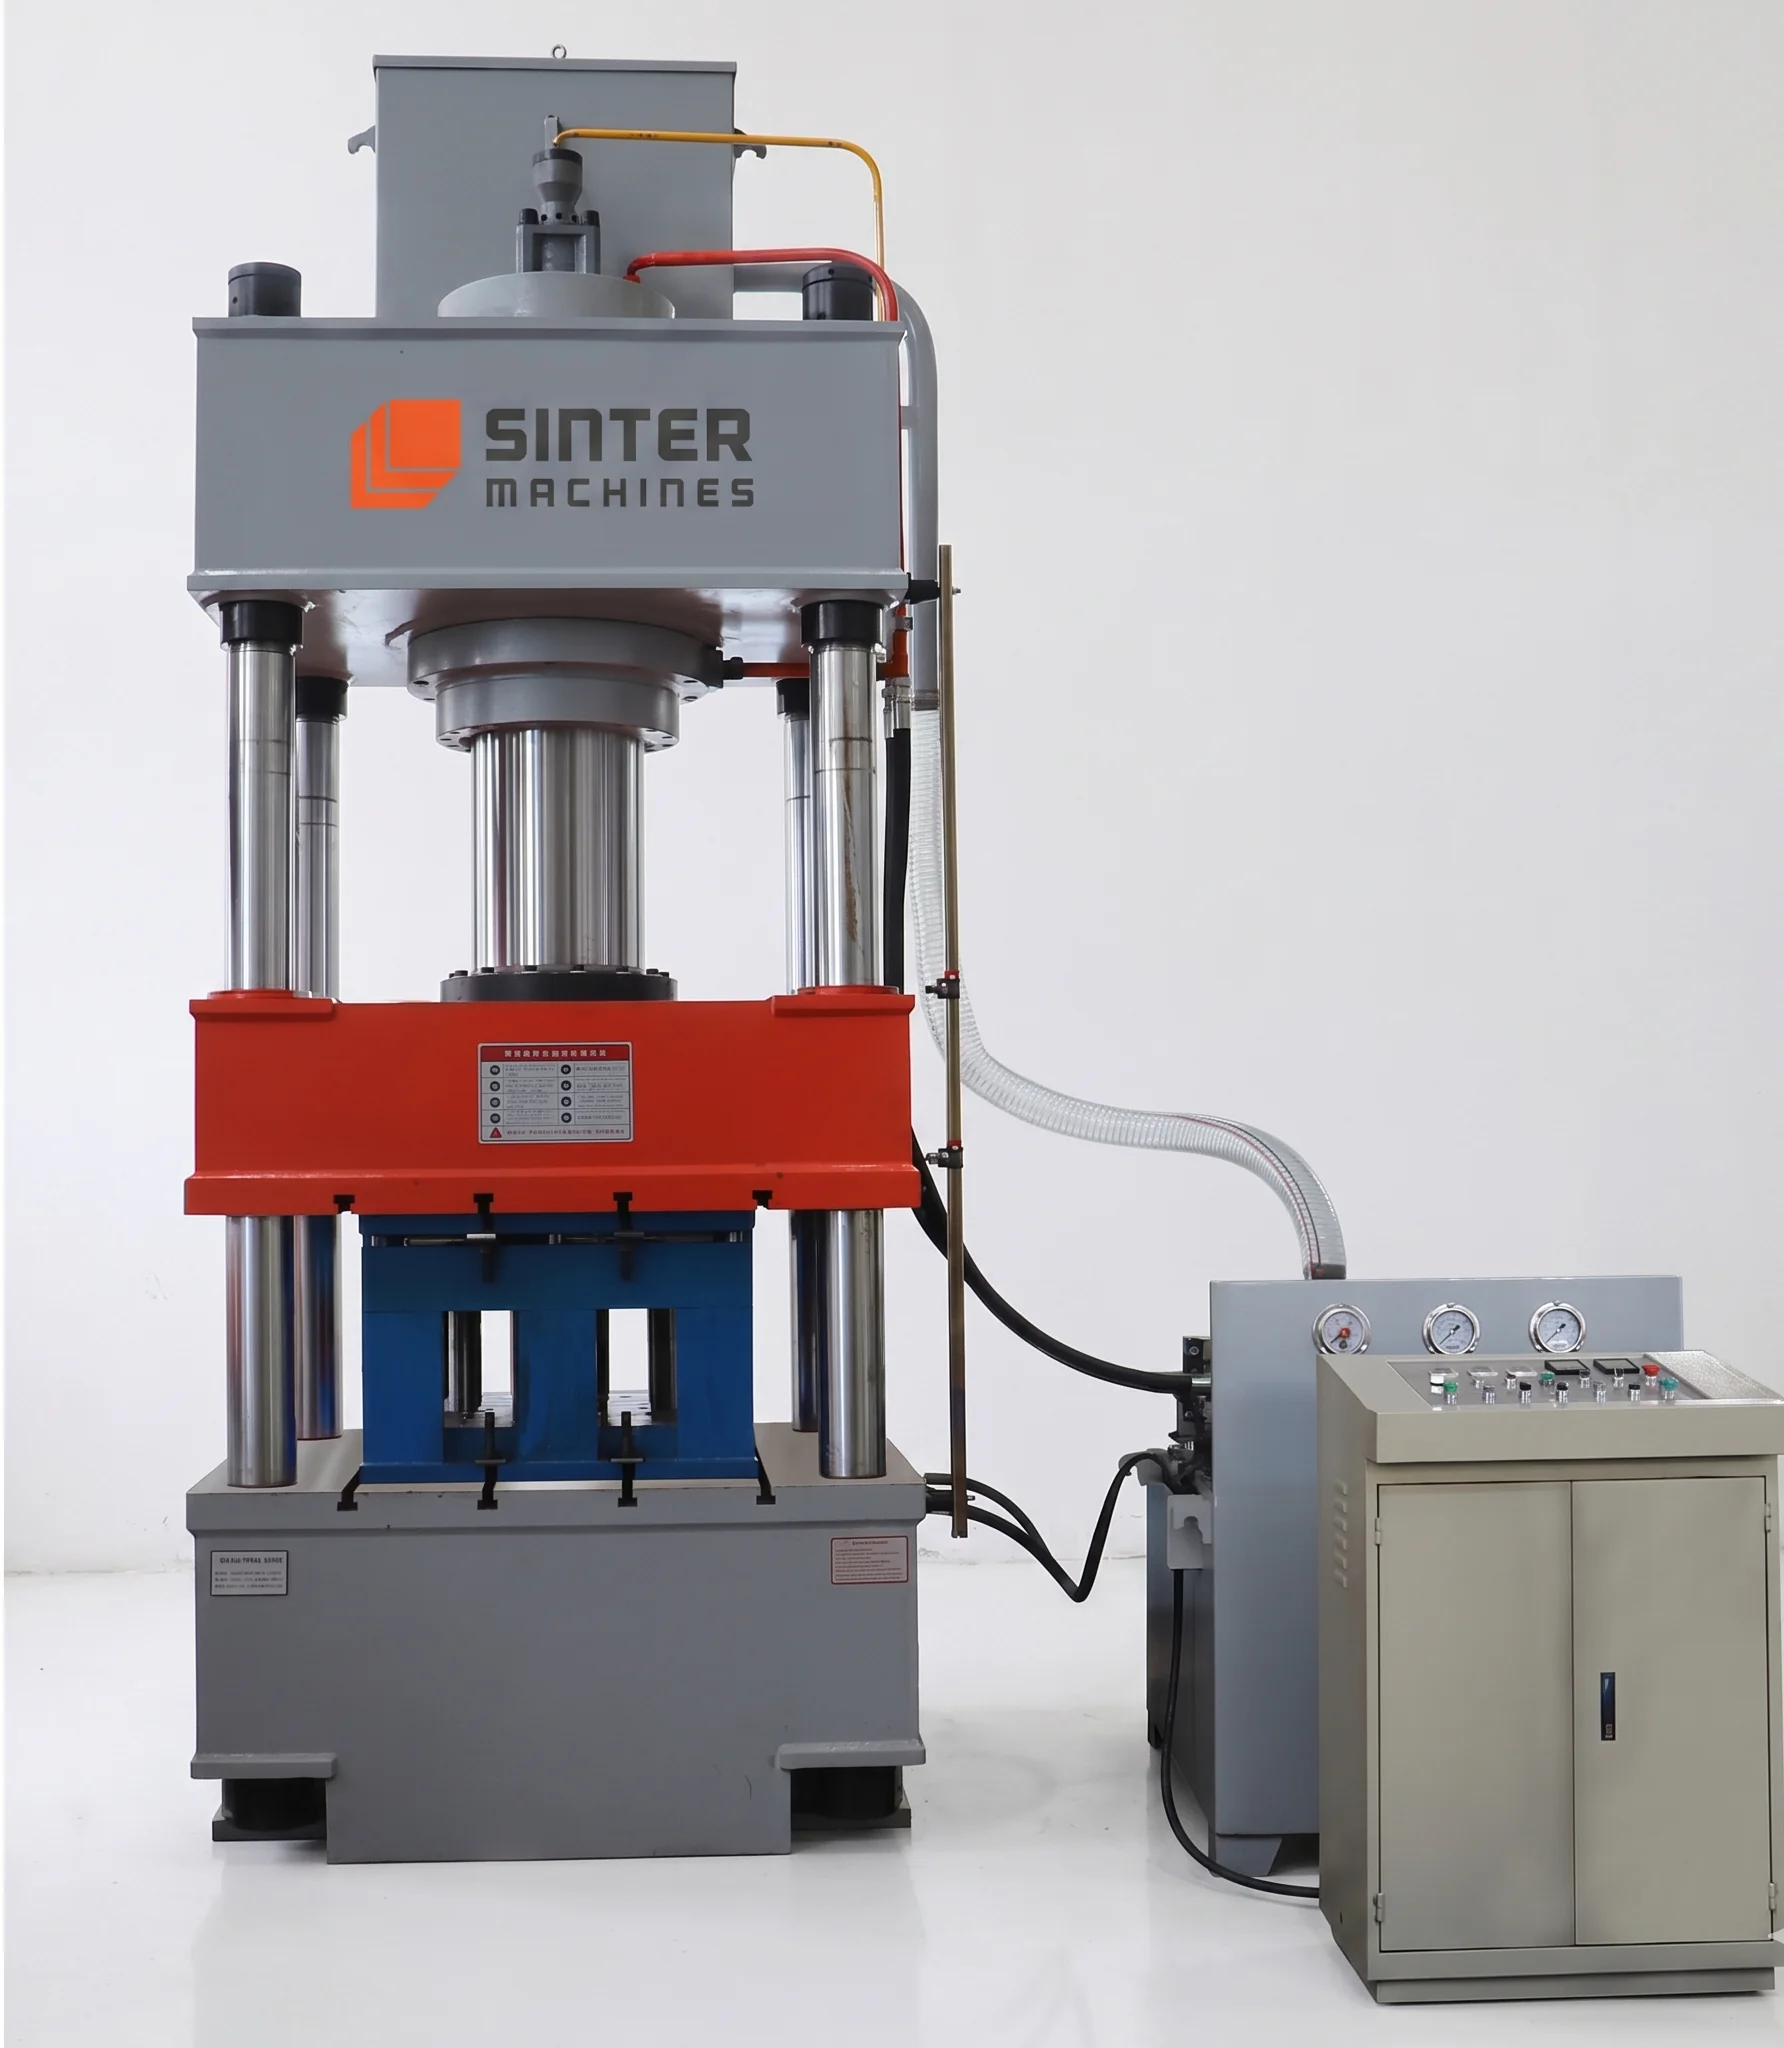
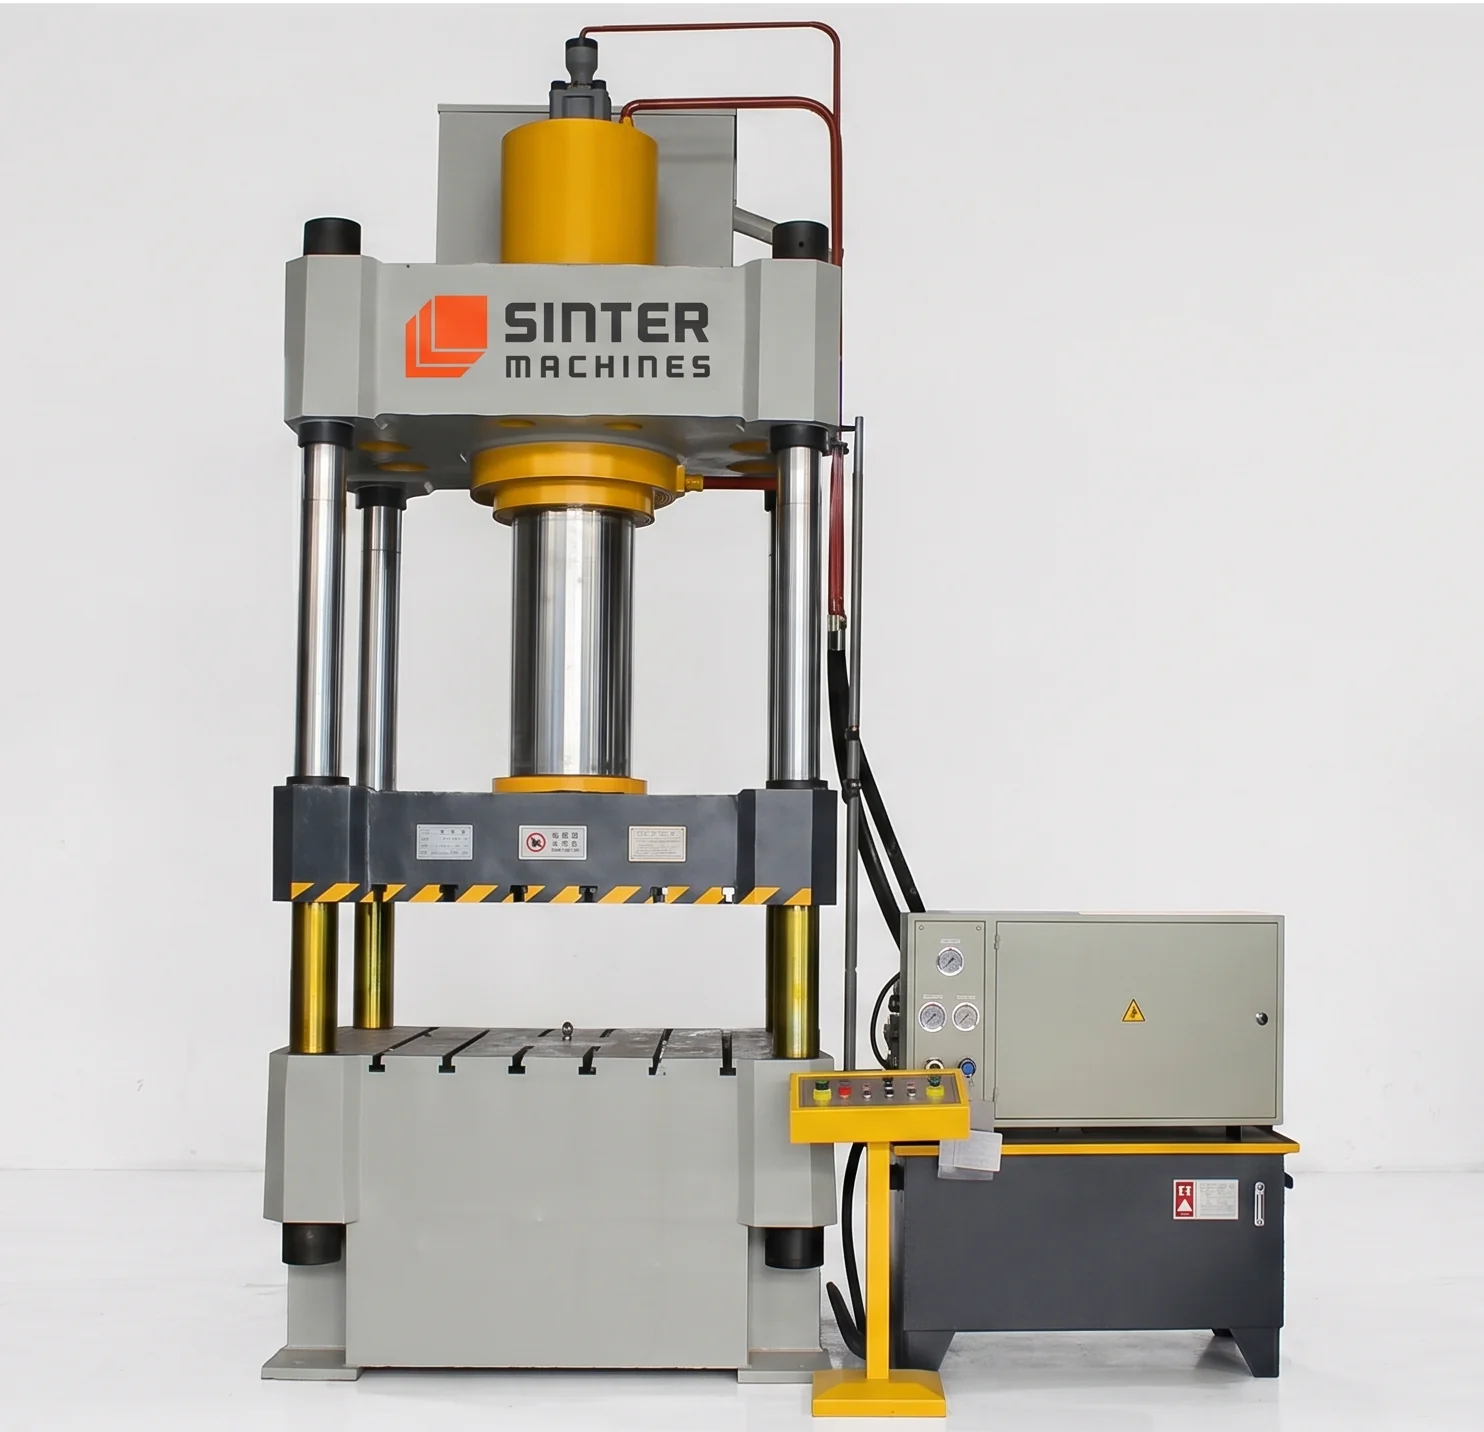
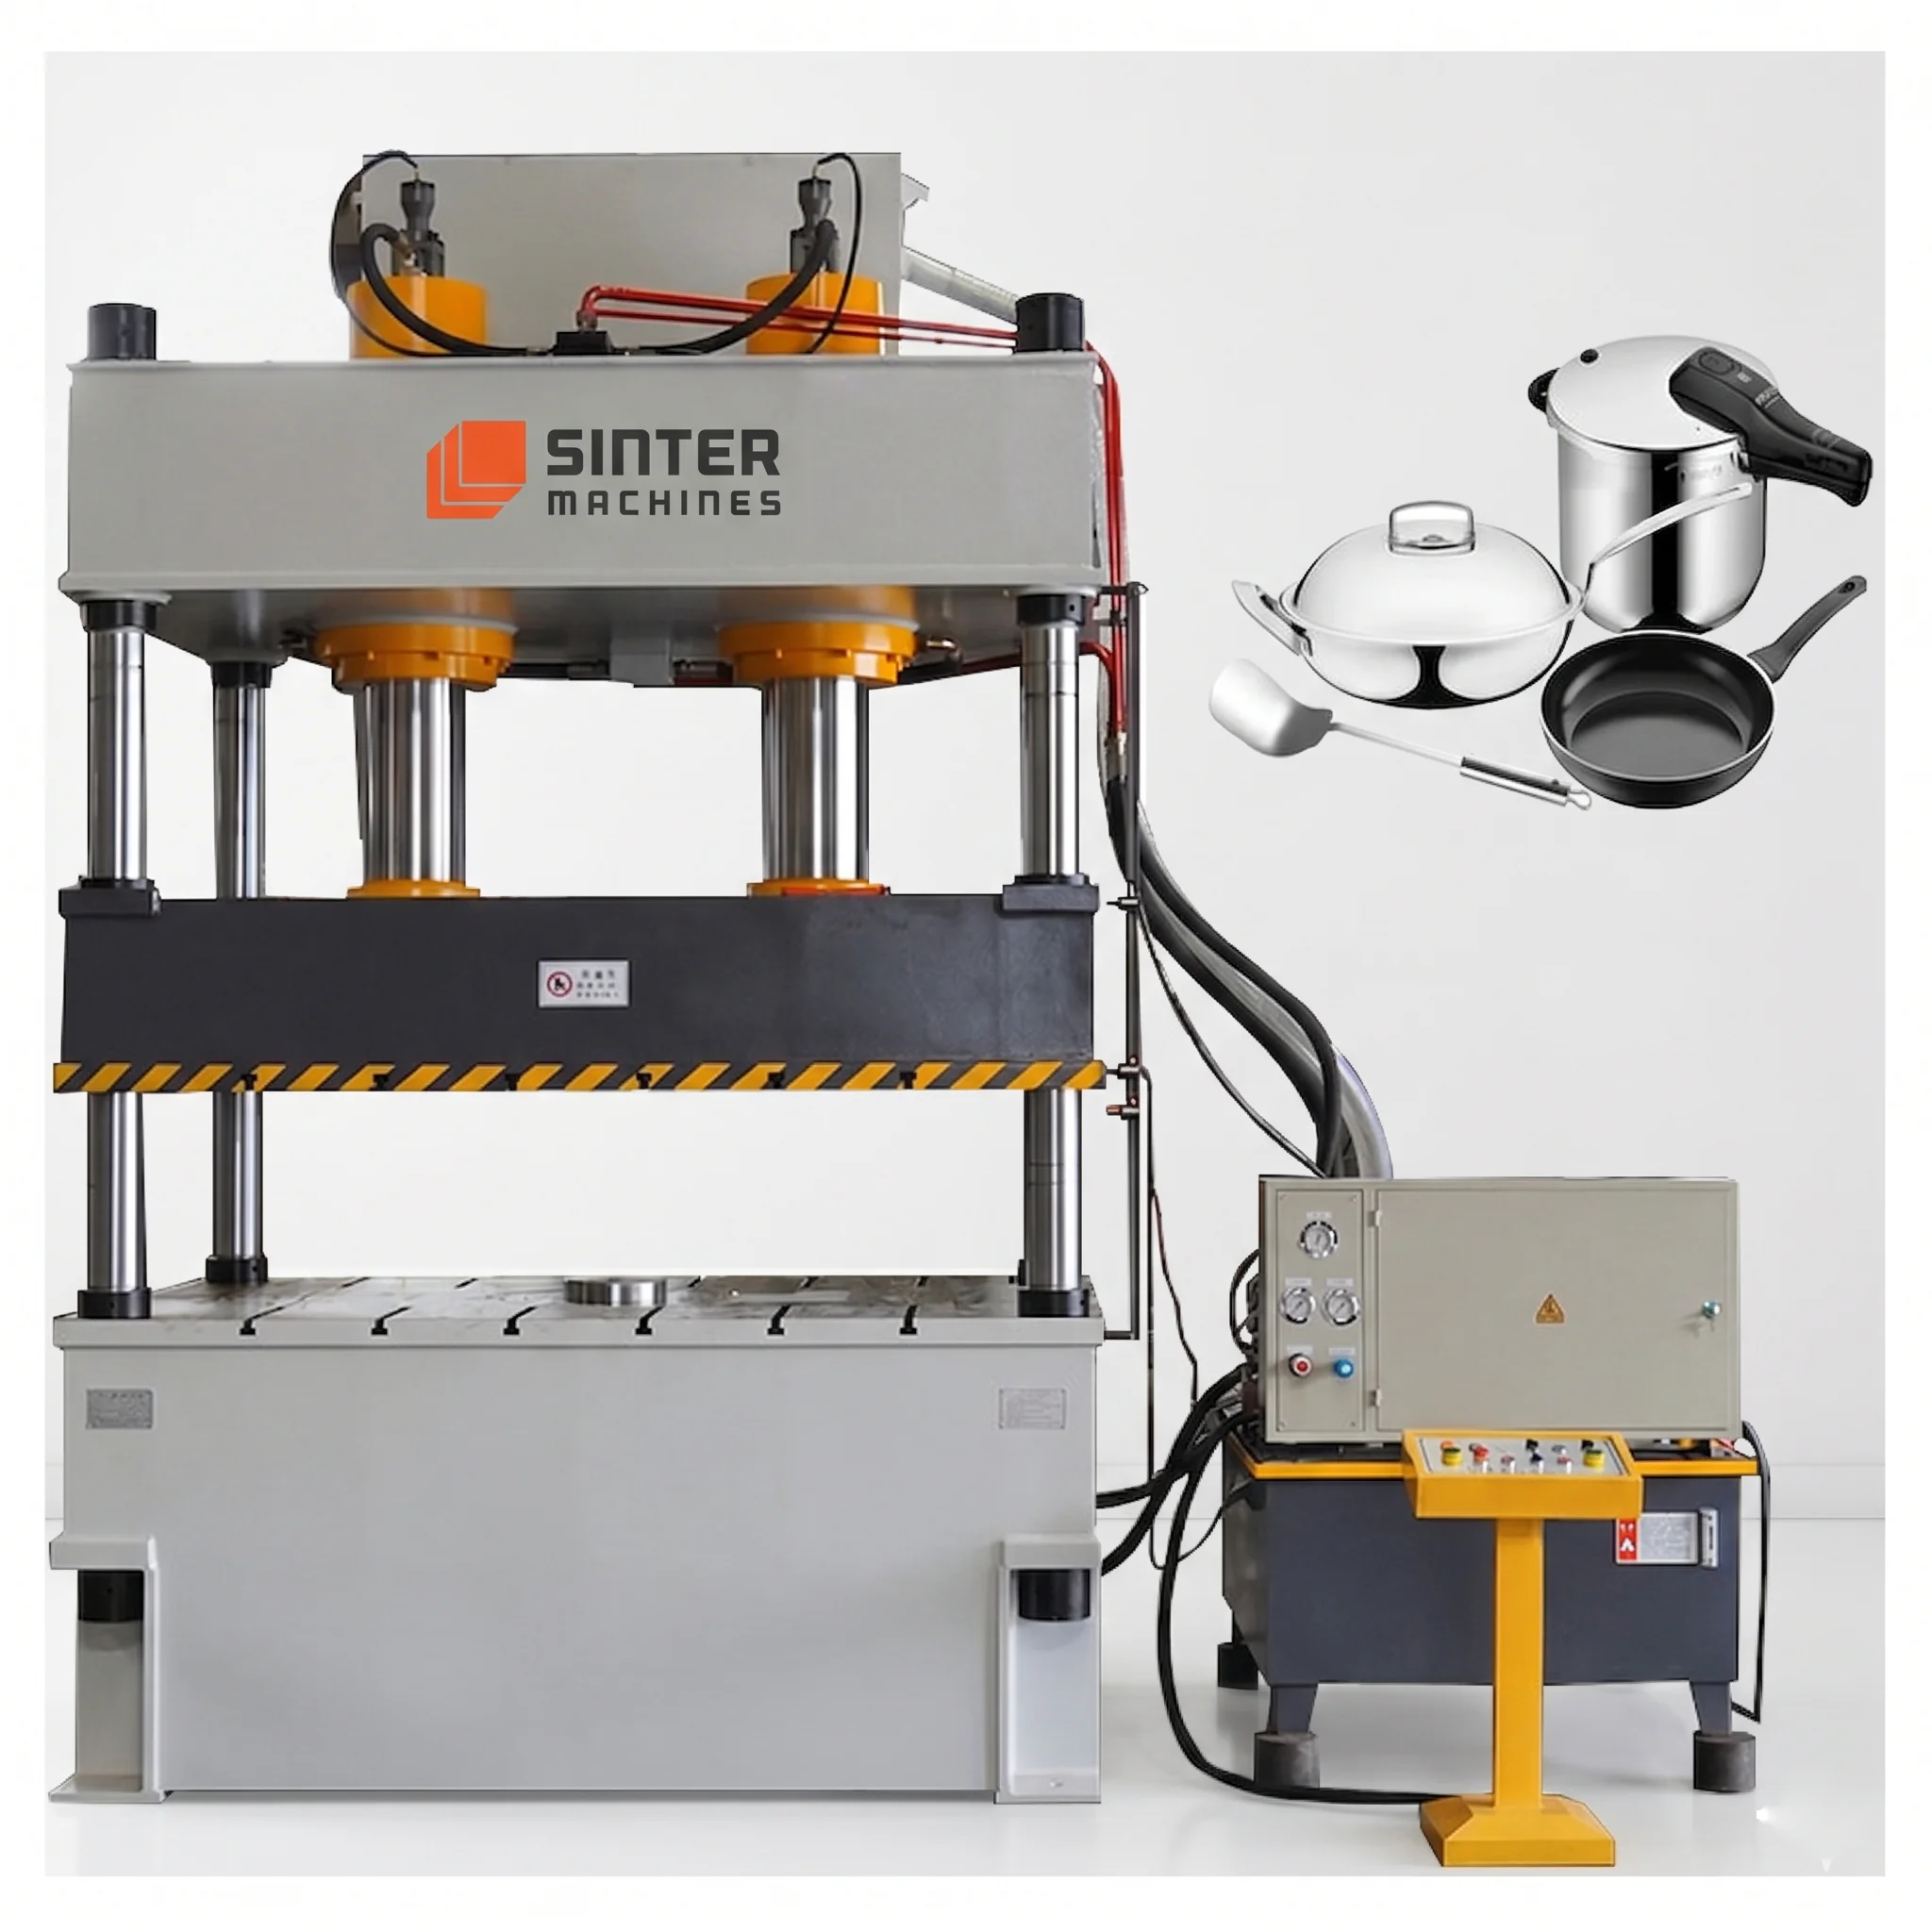
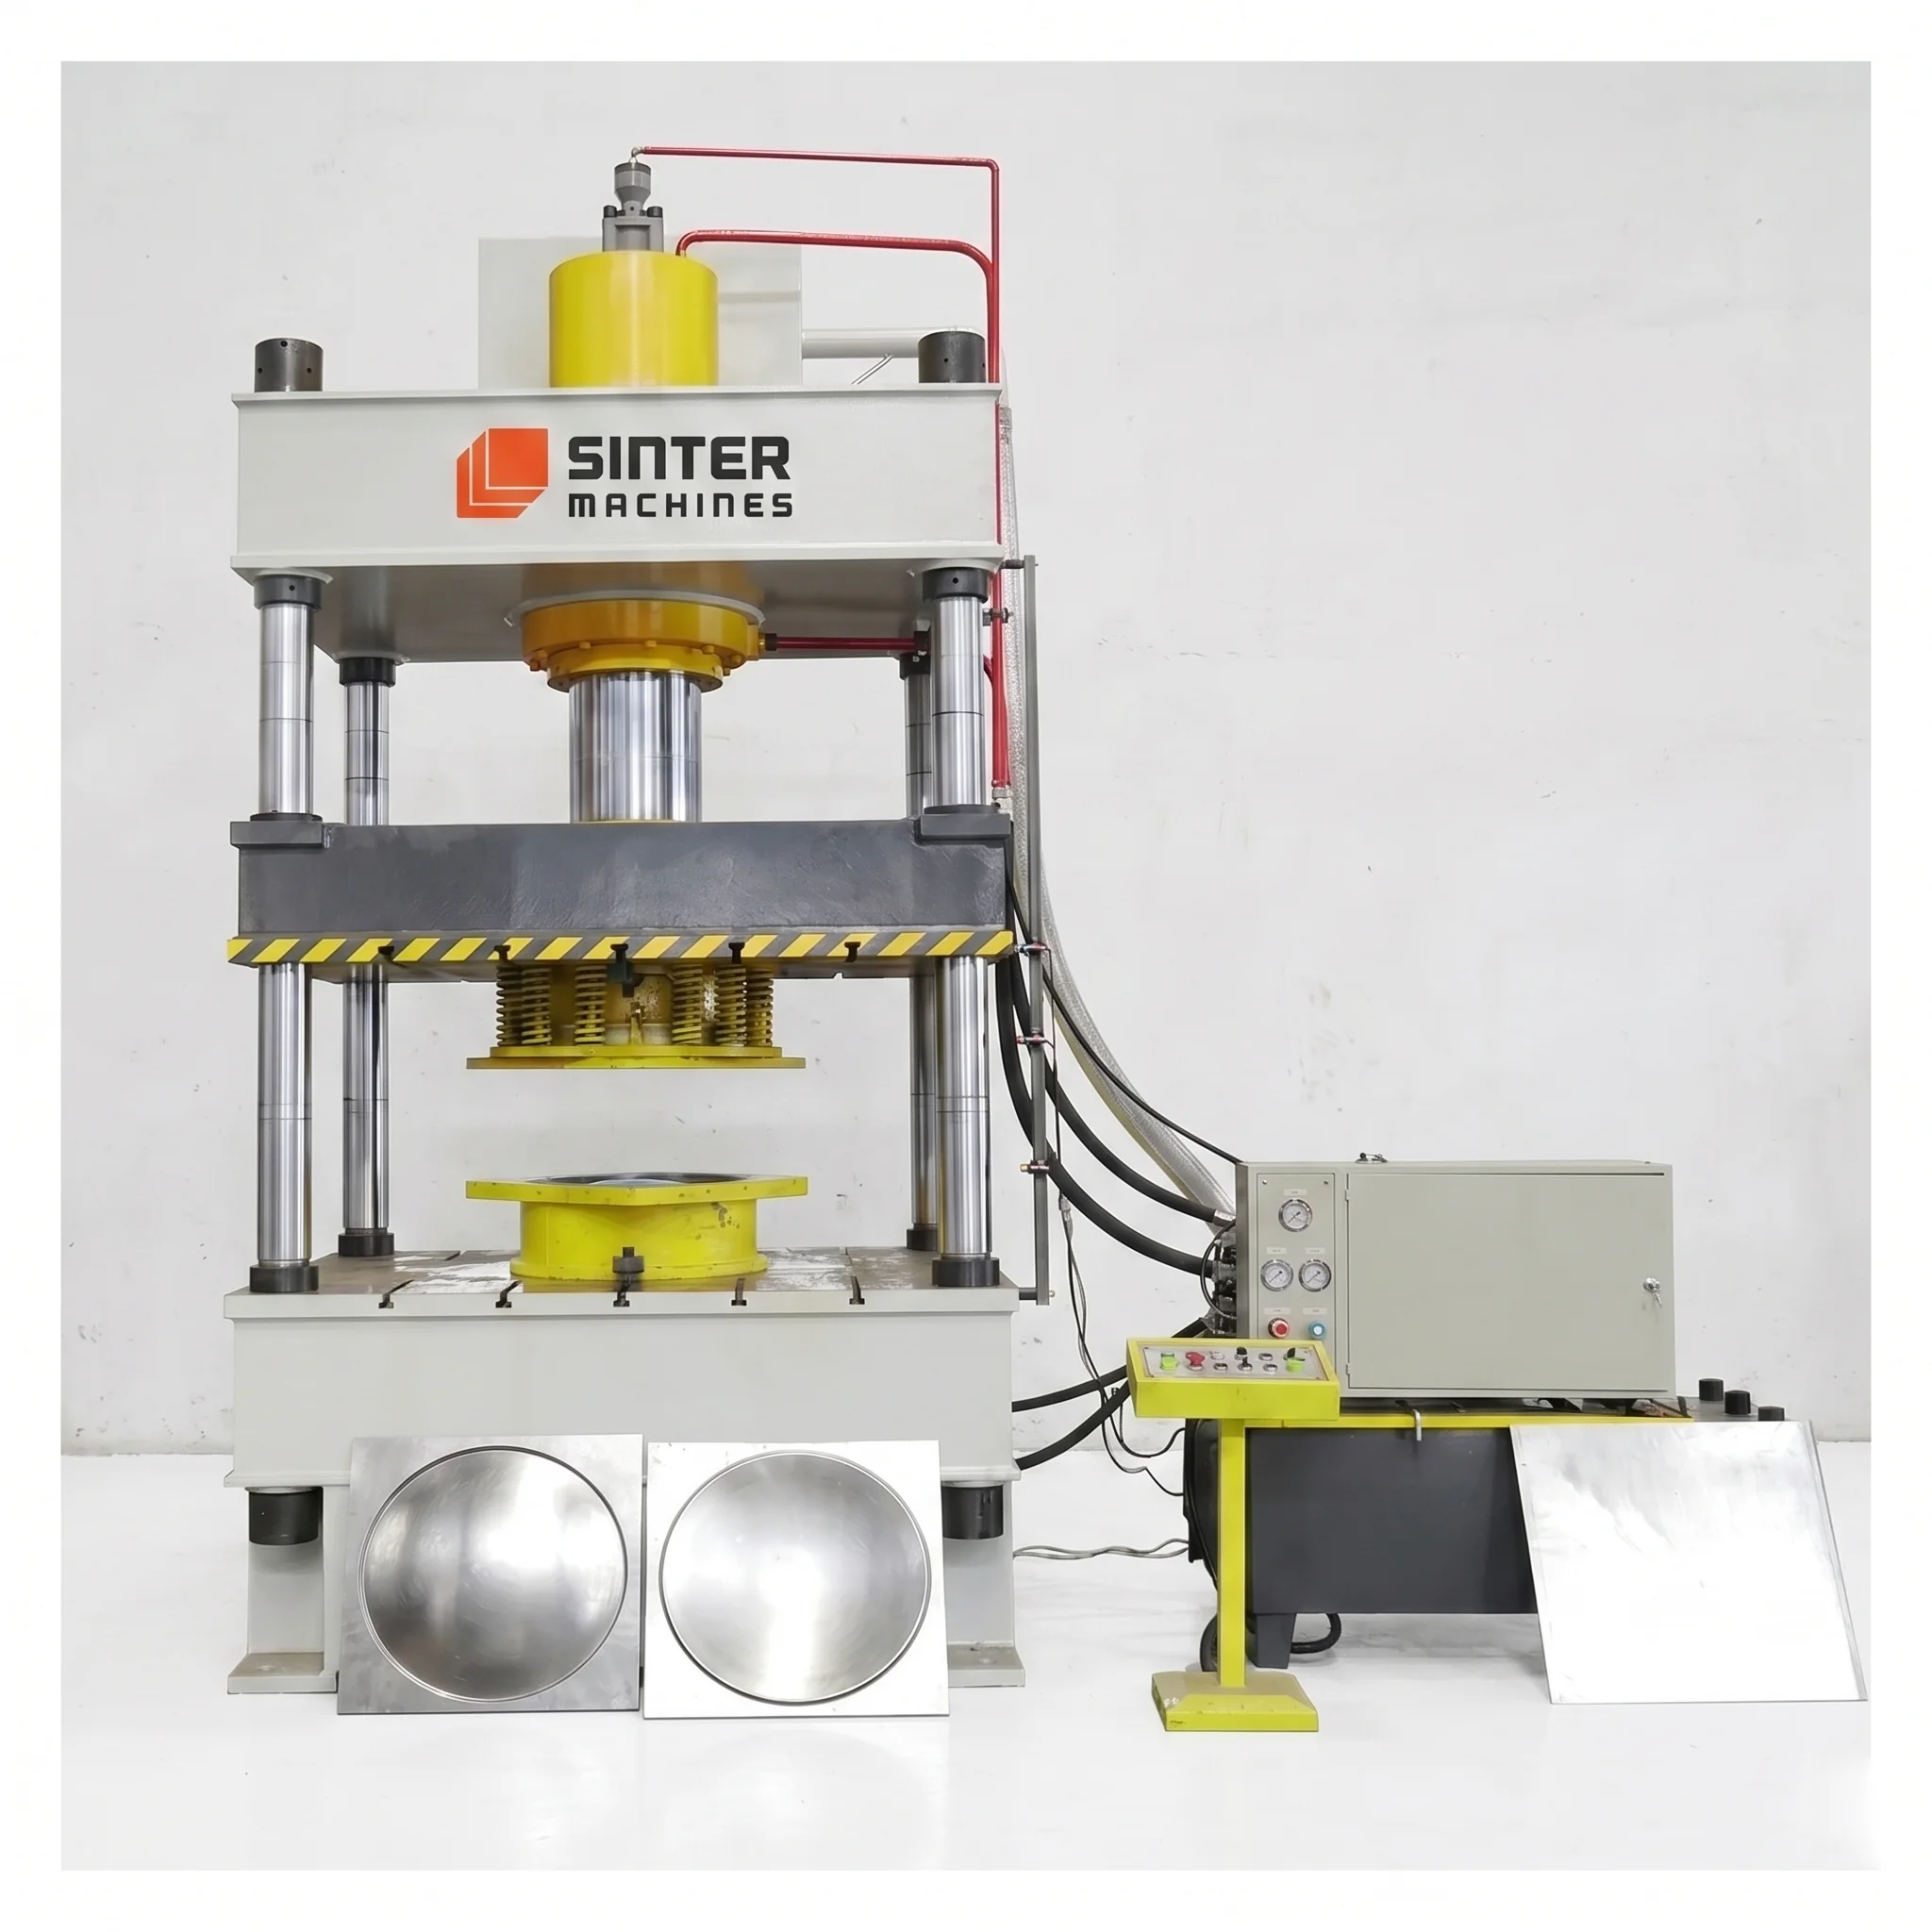
315T Pressing Cookware Pots & Pans Press press view 1
Pressing cookware pots & pans · Hydraulic Press Machine

315 Ton Four Pillar Hydraulic Press for Pressing & Punching Cookware Pots & Pans

315T Rated Capacity
100 mm/s Slider Down Speed
7–12 mm/s Slider Pressing Speed
90 mm/s Slider Return Speed

01 — Press System

315 Ton Four Pillar Hydraulic Press Machine

The 315-ton four-pillar hydraulic press is an ideal solution designed for deep drawing, pressing, and punching cookware pots, pans, and lids. This robust configuration is widely adopted by high-volume cookware OEMs and export-oriented kitchenware plants to secure long tooling life and scalable operations.

Use Case

Cookware production requires uniform material deformation and clean hole clipping to maintain cosmetic appeal and reliable thermal performance. This press combines smooth, multi-stage pressure application with precise bed alignment to form deep vessels and punch attachment slots without scratching or tearing the metal.

Core Applications

  • Deep draw forming of deep-bodied cooking pots, frying pans, and saucepans from flat metal blanks
  • Precision edge trimming, handle mounting hole punching, and lid steam vent slotting

Material

  • High-grade food-safe stainless steel sheets such as AISI 304 and AISI 430 variants
  • Lightweight, highly conductive aluminum blanks, clad multi-metal layers, and brass sheets

Typical Products Processed

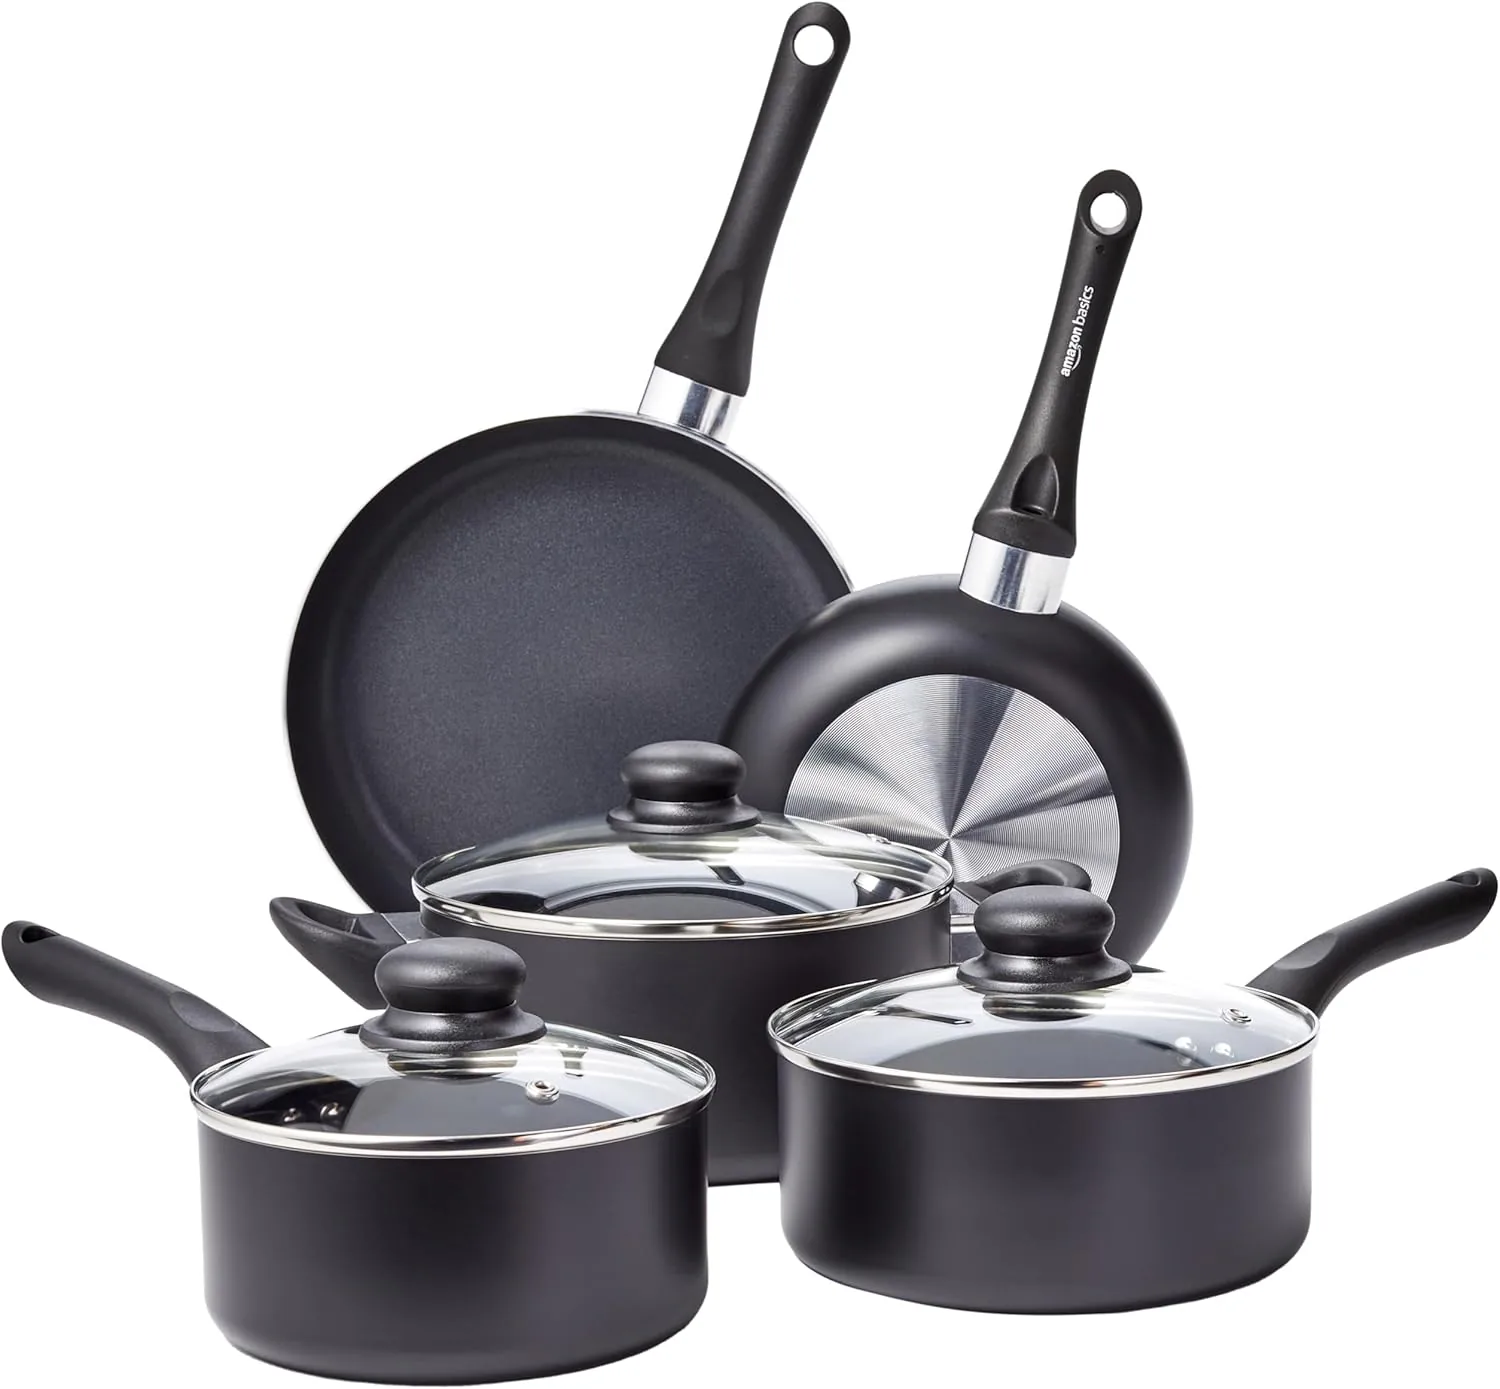
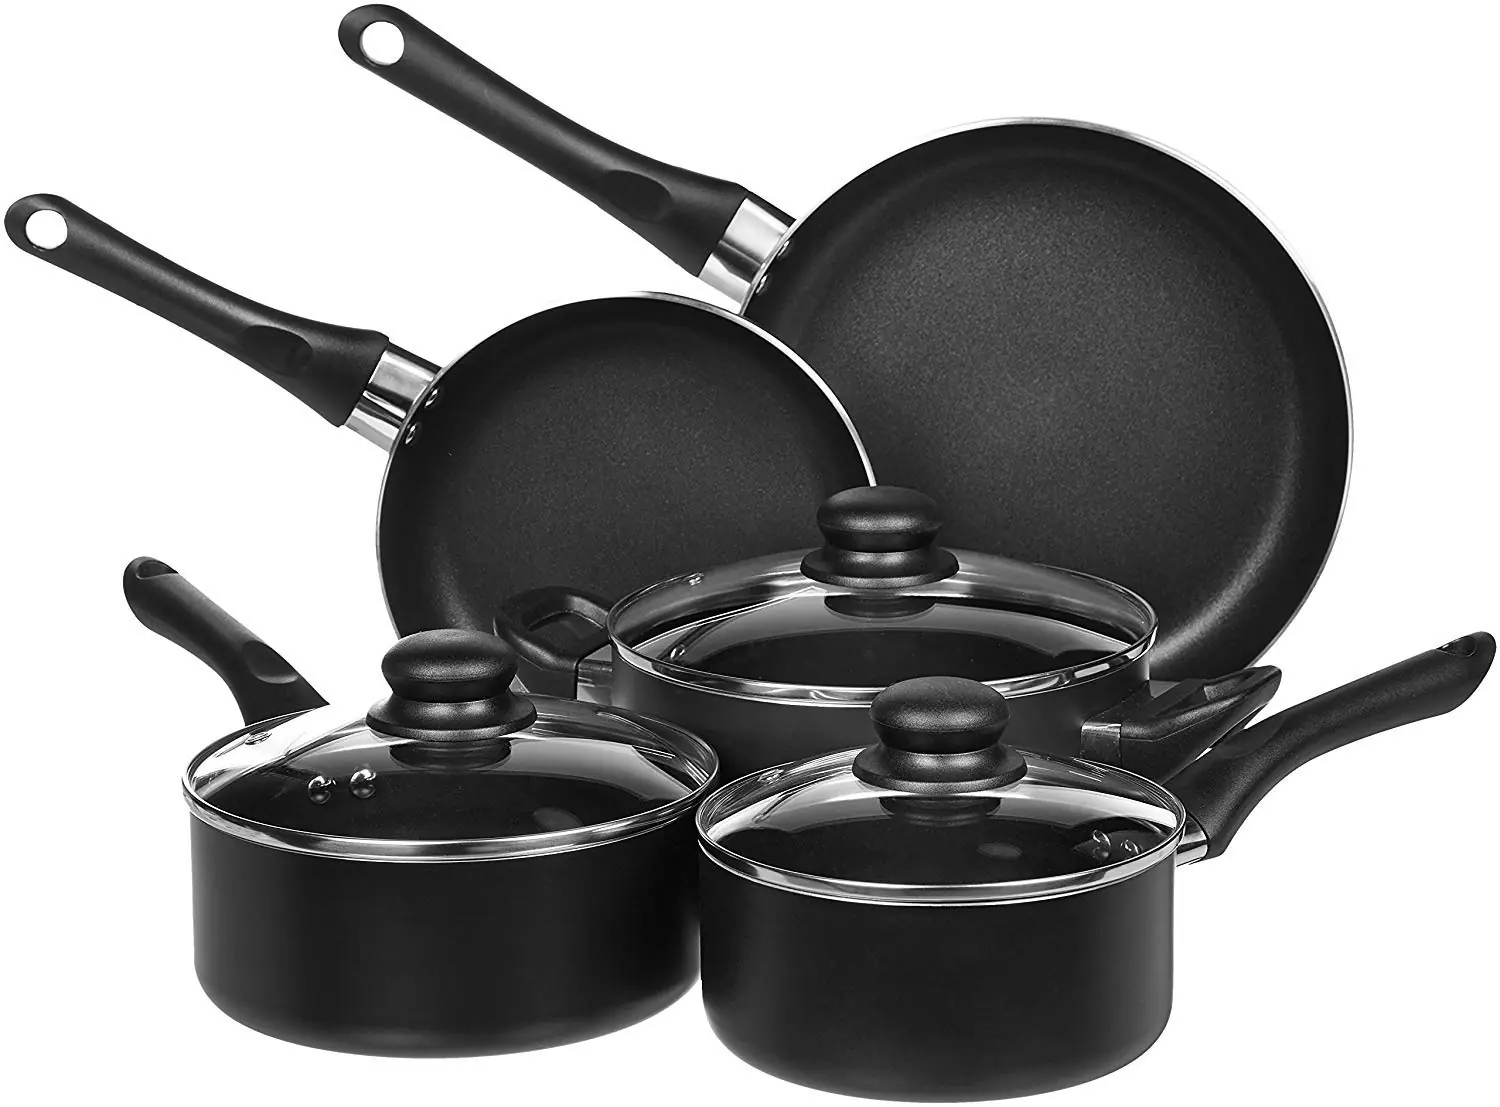
  • Domestic and commercial cooking pots, stockpots, frying pans, wok pans, and pressure cooker bodies
  • Universal matching lids, multi-ply thermal base disks, saucepans, and serving utensils

Key Functions

  • Integrated hydraulic cushion system to control blank-holding pressure dynamically during deep drawing stages
  • Variable stroke and speed adjustment parameters to prevent wrinkling or tearing on thin sheet blanks

Why 315-Ton Hydraulic Press?

  • Provides the optimal balance of high tonnage and compact bed space needed for medium-to-large consumer kitchenware sizes
  • Rigid four-pillar design prevents platen tilting, keeping punch clearances uniform to eliminate scrap flash defects

02 — Technical Specifications

SM 315 HP – HYDRAULIC PRESS MACHINE COMPLETE TECHNICAL DATA

The SM 315 HP hydraulic press delivers highly controlled tonnage and uniform pressure distribution for demanding deep drawing and punching operations. Its robust four-column architecture ensures perfect platen parallelism to produce scratch-free, export-quality cookware consistently.

Capacity

  • Maximum pressing force capacity of 3150 kN
  • Integrated hydraulic cushion clamping force of 1200 kN

Structural Design

  • Four pillar monolithic heavy steel plate construction
  • Finite element analysis engineered for low stress deflection under load

Frame Type

  • High rigidity pre stressed column frame layout
  • Heavy duty solid welded steel bolster bed and top crown structure

Hydraulic System

  • Variable displacement axial piston pump power delivery assembly
  • Continuous oil filtration and multi pass cooling loop system

Main Ram Stroke

  • Maximum slide vertical travel stroke length of 600 mm
  • Adjustable depth control accuracy maintained down to 0.1 mm

Working Hydraulic Pressure

  • Maximum continuous operating system pressure of 240 bar
  • Peak transient hydraulic safety relief pressure of 270 bar

Daylight Gap

  • Maximum open vertical daylight window area of 900 mm
  • Minimum closed shut die height space of 300 mm

Approach Speed

  • Fast downward advance slide rapid travel speed of 200 mm/Sec
  • Soft touch pre contact decelerating tool entry speed of 12 mm/Sec

Pressing / Drawing Speed

  • Controlled high pressure deep drawing speed of 8 to 22 mm/Sec
  • Precision secondary blank punching speed capability of 30 mm/Sec

Return Speed

  • Rapid upward ram ascent extraction return speed of 160 mm/Sec
  • Automated pre return pressure decompression cycle timing

Bed / Platen Size Platen

  • Total clear bolster bed width left to right of 1200 mm
  • Total clear bolster bed depth front to back of 1000 mm

Columns

  • Induction hardened hard chrome plated solid steel pillar diameter of 160 mm
  • Extended length guide bushings with automatic centralized lubrication loops

Working Envelope

  • Total internal clear workspace area of 1200 by 1000 mm
  • Maximum allowable upper die tooling mass weight of 4500 kg

Control System

  • Central programmable logic controller with digital color touchscreen interface
  • Real time pressure monitoring and digital stroke position tracking setups

Main Motor Power

  • Primary high efficiency electrical drive motor capacity of 37 kW
  • Secondary auxiliary die cushion control pump motor capacity of 7 kW

Valves & Hydraulics

  • High response logic element cartridge valve block assembly
  • Integrated main cylinder fast gravity pre fill valve system

Automation

  • Digital interface connections for automatic sheet feeder mechanisms
  • Dual palm button control station with integrated batch counters

Safety Features

  • Dual side infrared safety light curtains covering working areas
  • Fail safe mechanical anti drop lock safety block on main ram

SM 315 HP — Model Specifications

  • Nominal Force: 3150 KN
  • Maximum Hydraulic Pressure: 25 MPa
  • Max Opening Height of the Slider: 1000 mm
  • Max Stroke of the Slider: 600 mm
  • Effective Bed Size: 800 × 800 mm
  • Slider Down Speed: 100 mm/s
  • Slider Pressing Speed: 7–12 mm/s
  • Slider Return Speed: 90 mm/s
  • Ejector Cylinder Nominal Force: 300 KN
  • Stroke of the Ejection Cylinder: 300 mm
Production Case Study

Pressing & Punching Cookware Pots & Pans Production Line

0.6 – 3.0 mmSheet Thickness
SS 304/AluMaterial Used
8–12 SecCycle time
360 to 500 PartsOutput/Hour
Wall tearing prevented entirely
Surface scratching eliminated completely
Thickness uniformity maintained perfectly
Hourly output increased significantly
Rejection rates dropped sharply
Edge trimming executed cleanly
Deep drawing optimized fully
03 — Die / Mold System

Precision Pressing & Punching Cookware Pots & Pans Die Mold Engineering

This precision tooling system is engineered to handle deep drawing and clean punching cycles for high-volume commercial kitchenware fabrication. It incorporates uniform metal flow mechanics to ensure scratch-free surfaces and uniform wall transitions across deep vessels.

Use Case

The mold assembly is deployed in cookware stamping lines to draw flat metal circles into deep pots and punch handle holes in a single sequence. It eliminates metal wrinkling and tearing, securing the export-grade cosmetic finish required for consumer markets.

Technical Specifications (Tooling)

Die Type

  • Heavy duty deep drawing and secondary combined punching die assembly
  • Multi stage modular kitchenware production drawing tool setup

Die Materials

  • Premium shock resistant cold work alloy tool steel matrix
  • Ultra hard tungsten carbide draw ring inserts in high friction sectors

Tool Configuration & Construction

  • Interchangeable draw ring matrix layout featuring rapid changeover capability
  • Hardened base plates fitted with heavy duty ball bearing guidance pillars

Key Tooling Features

  • Integrated pneumatic nitrogen gas spring blank holder pressure cushion systems
  • Automated reverse lift mechanical component ejector mechanism configurations

Alignment Accuracy

  • Total punching blade clearance variance maintained within 0.030 mm
  • Guide pillar axis geometric concentricity tolerance held tight at 0.006 mm

Process Materials

  • Food safe austenitic stainless steel sheets including grade 304 and 430
  • High thermal conductivity aluminum alloy sheets and multi layer clad blanks

Surface Finish

  • Active drawing radii mirror polished down to Ra 0.10 microns
  • Advanced physical vapor deposition low friction chrome coating at 0.005 mm thickness

Tool Life

  • Expected production span of 150000 cycles before mandatory ring polishing
  • Total structural service capacity reaching 2500000 production cycles
Case Study (Die Performance)

Precision Pressing & Punching Cookware Pots & Pans Die Mold

High-carbon high-chromiumDie Material
58-60 HRCHardness
Vacuum HardenedHeat Treatment
Galling defects stopped completely
Material wrinkling prevented entirely
Draw rings preserved perfectly
Production uptime extended significantly
Cosmetic rejects reduced drastically
Clean edge cuts achieved
Scrap rates minimized fully

04 — Product Application

Where Precision Pressing & Punching Cookware Pots & Pans Are Used

Precision-pressed and punched pots, pans, and lids form the foundational hardware used daily across residential, commercial, and institutional food preparation environments globally. These high-quality vessels provide the necessary structural resilience, even heat distribution, and clean handle integration required for intense culinary operations.

Industry Applications

These meticulously formed cookware products are indispensable across retail consumer goods markets, global hospitality supply chains, corporate catering sectors, and home appliance manufacturing ecosystems. Their exact material execution satisfies strict international food-safety sanitation standards while ensuring maximum thermal efficiency for energy-conscious consumers.

Domestic Kitchen Collections

Standard everyday frying pans, deep stockpots, and matching ventilation lids populate consumer households and residential kitchens worldwide. These consumer products combine high aesthetic mirror finishes with robust everyday durability to withstand frequent thermal cycling and washing.

Commercial Culinary Establishments

Heavy-duty stainless steel braising pans, large-capacity woks, and saucepans handle the punishing workloads of busy restaurants and hotel kitchens. The uniform wall thickness prevents localized food scorching, while deep-drawn bodies ensure long-term structural integrity under high-volume daily use.

Institutional Catering Operations

Massive industrial boilers, oversized stockpots, and specialized food service insert pans feed military bases, schools, and corporate cafeterias. These ultra-thick vessels resist heavy impacts from industrial stirring gear and maintain tight geometric tolerances for high-stack storage configurations.

Automated Appliance Integration

Specialized deep-drawn cooking liners and pressure vessels serve as the internal heating bowls for electric multi-cookers and smart appliances. The precision-punched rims and strict dimensional accuracy guarantee airtight pressure sealing and seamless assembly inside automated appliance housings.

Finished Product Gallery

05 — Key Advantages

Why Choose the 315-Ton Sinter Hydraulic Press

The 315-Ton Sinter Hydraulic Press features an integrated blank-holder cushion that delivers flawless, wrinkle-free material flow across complex deep-drawn profiles. It maintains strict wall-thickness uniformity and a pristine surface cosmetic finish, maximizing product yield while lowering production costs.

Technical & Commercial Benefits

01

Integrated Dynamic Cushion Pressure Control

The advanced hydraulic die cushion exerts uniform, real-time holding force to manage metal flow precisely during deep drawing stages. This active management prevents material tearing on thin stainless steel blanks, completely avoiding structural stretching defects.

02

Rigid Four-Column Platen Alignment Stability

Heavy-duty hard-chrome pillars eliminate structural frame tilting during off-center drawing or sudden hole-punching impacts. Maintaining perfect parallelism ensures uniform punch clearance, eliminating flash burrs and ensuring clean handle-mount holes.

03

Complete Elimination of Cosmetic Scratches

Ultra-smooth hydraulic stroke deceleration gently guides raw metal into the die cavity without generating aggressive scoring marks. Bypassing manual surface buffing or intensive post-process finishing directly reduces manufacturing labor hours.

04

Rapid Changeover for Flexible Batch Sizes

The large, open daylight workspace accommodates quick-die-change systems to swap molds rapidly between different pot sizes and lid styles. Minimizing machine downtime accelerates production agility and lowers inventory overhead for diverse product catalogs.

05

Extended Tooling and Die Lifespan

Integrated hydraulic shock absorbers safely dissipate sharp breakthrough forces usually generated during perimeter edge trimming and ventilation slotting. Lowering structural vibration prevents micro-chipping on tool steel dies, extending operating intervals between blade sharpenings.

06

High-Speed Output with Energy Optimization

Smart variable-displacement fluid pumps deliver rapid ram approach and retraction speeds to maximize hourly components processed. Drawing maximum power only during peak drawing load limits factory electrical consumption while boosting net output margins.