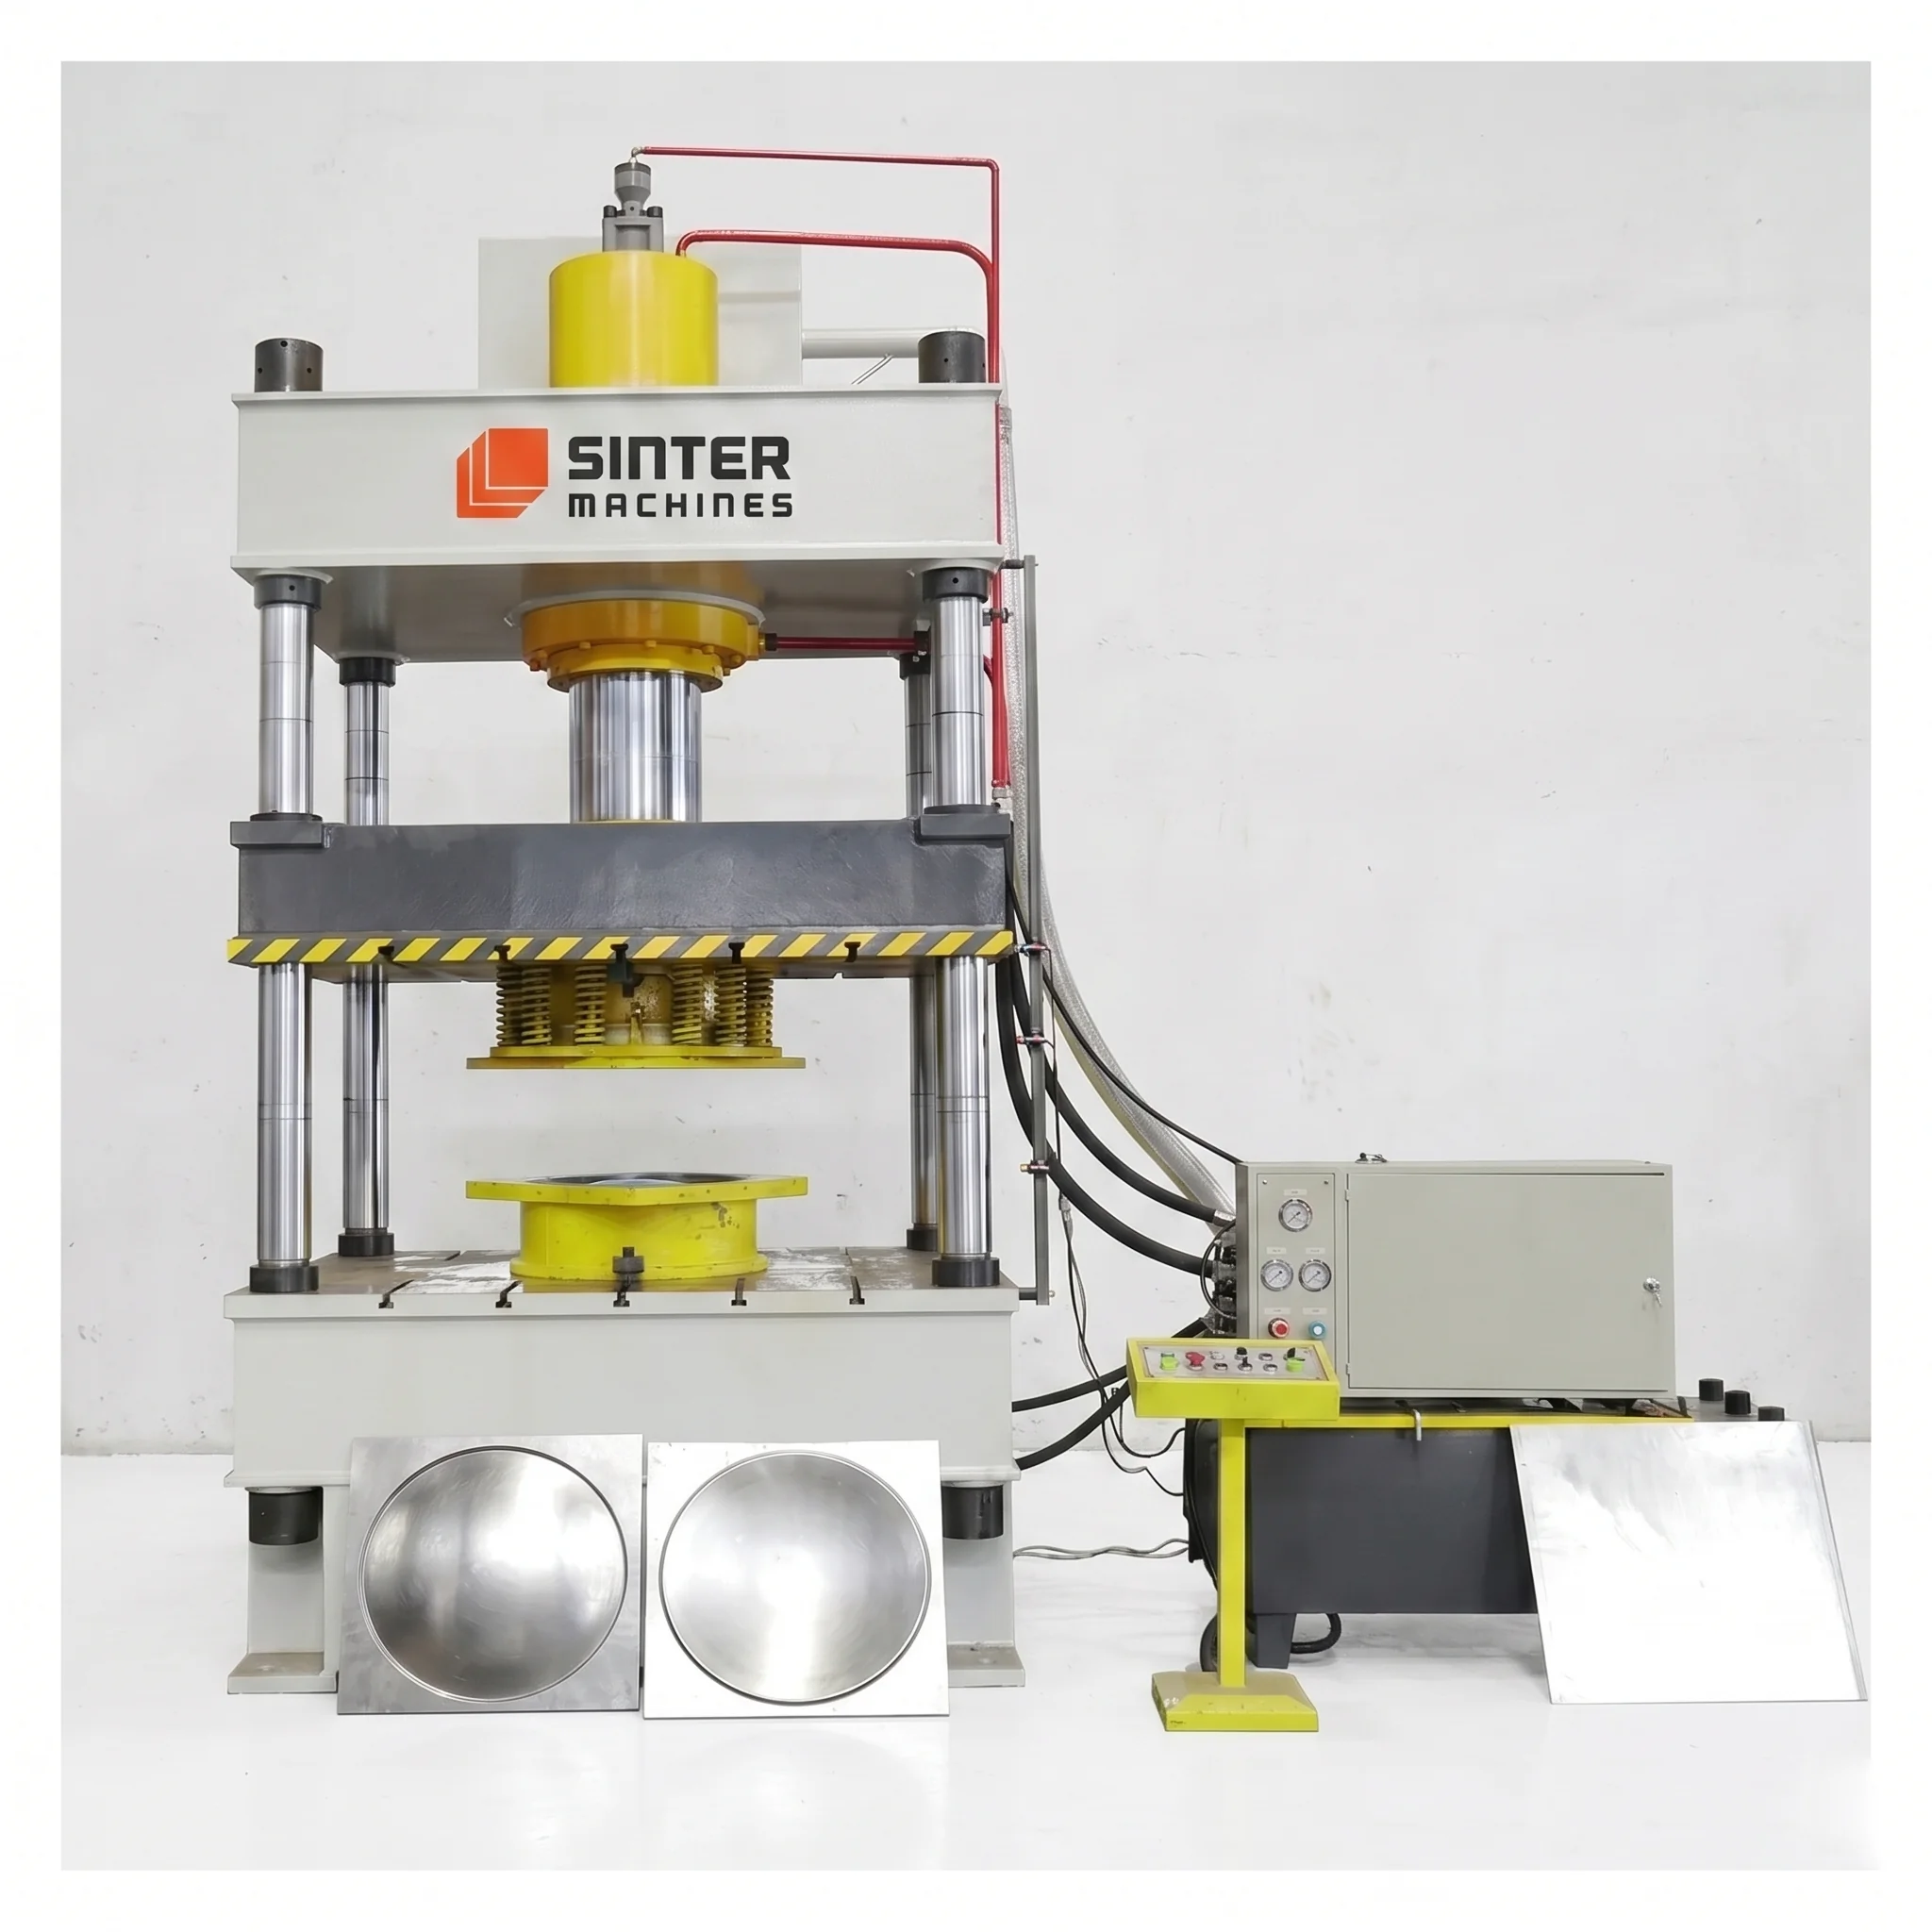
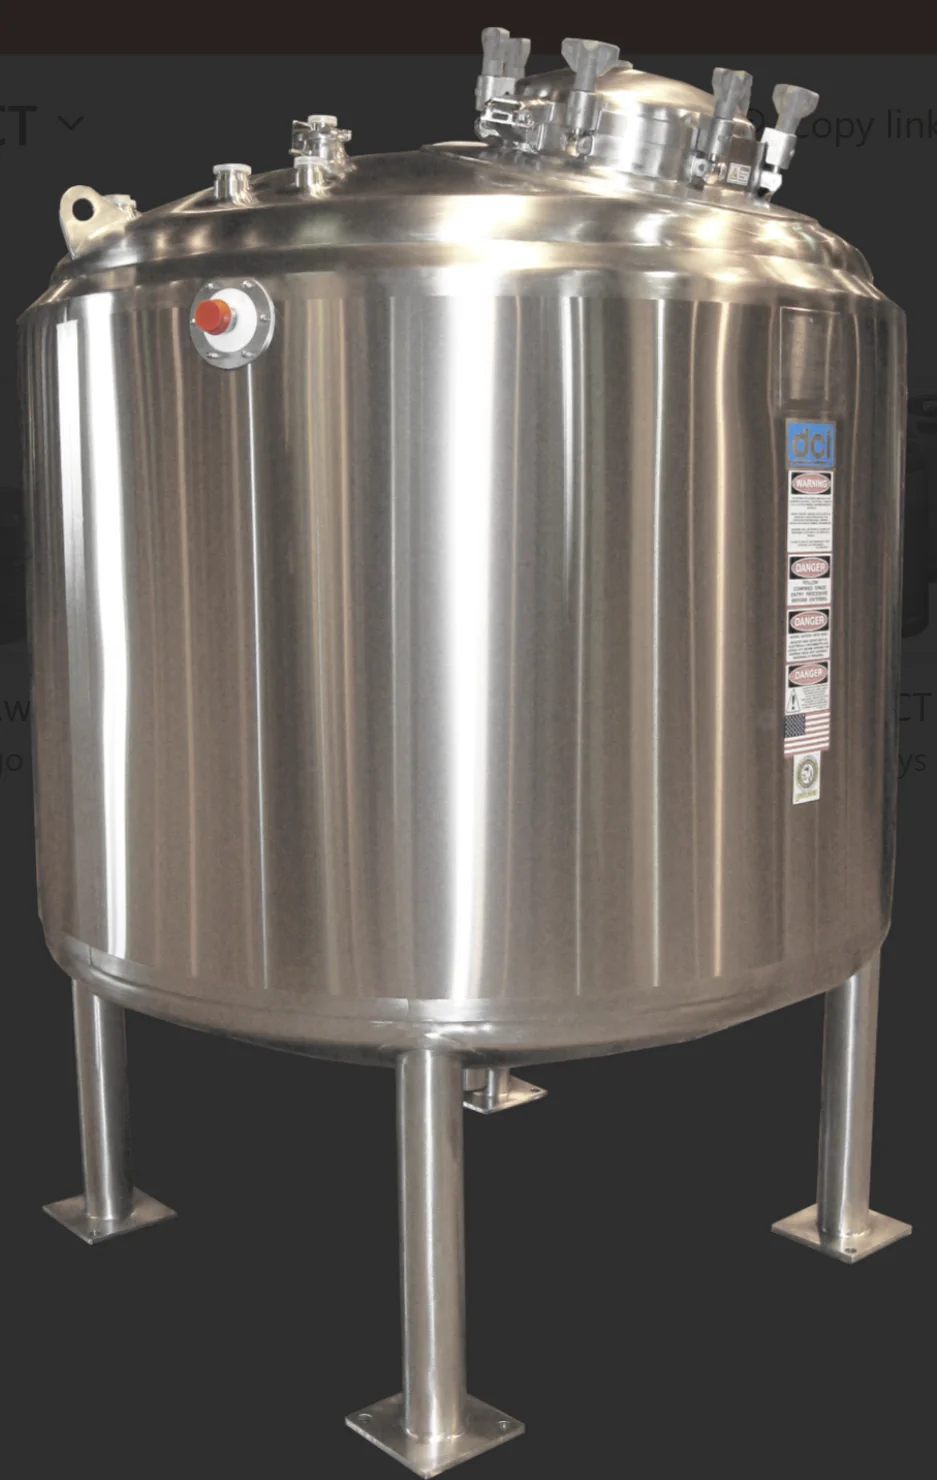
500T SS Food Containers Press press view 1
SS Food Containers · Hydraulic Press Machine

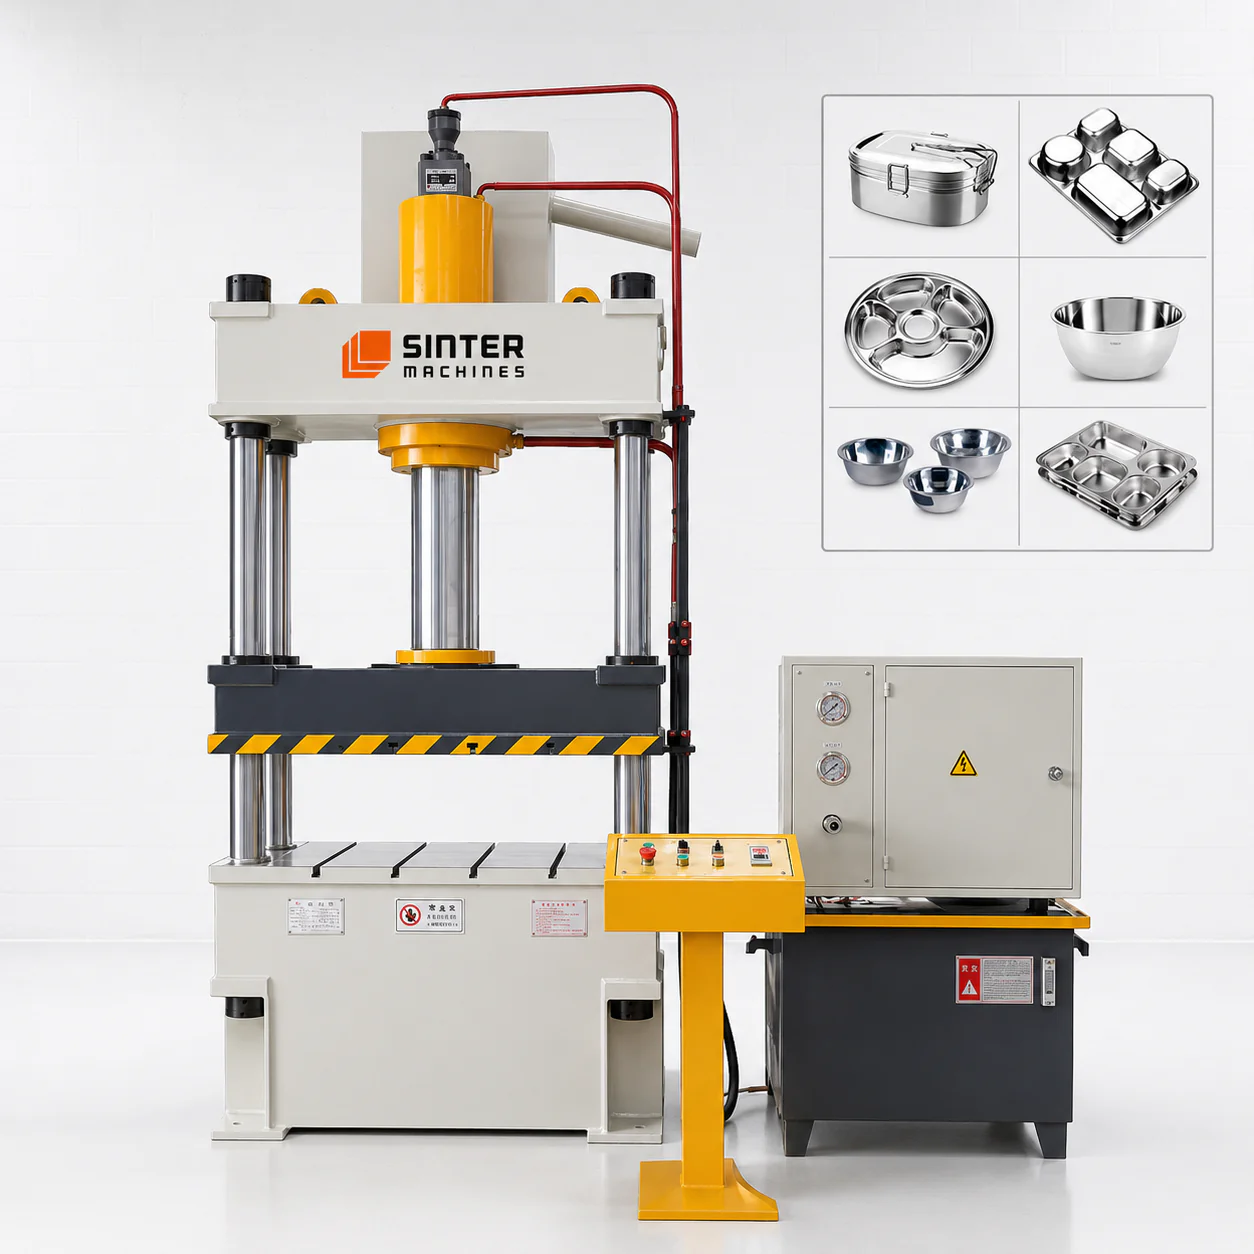
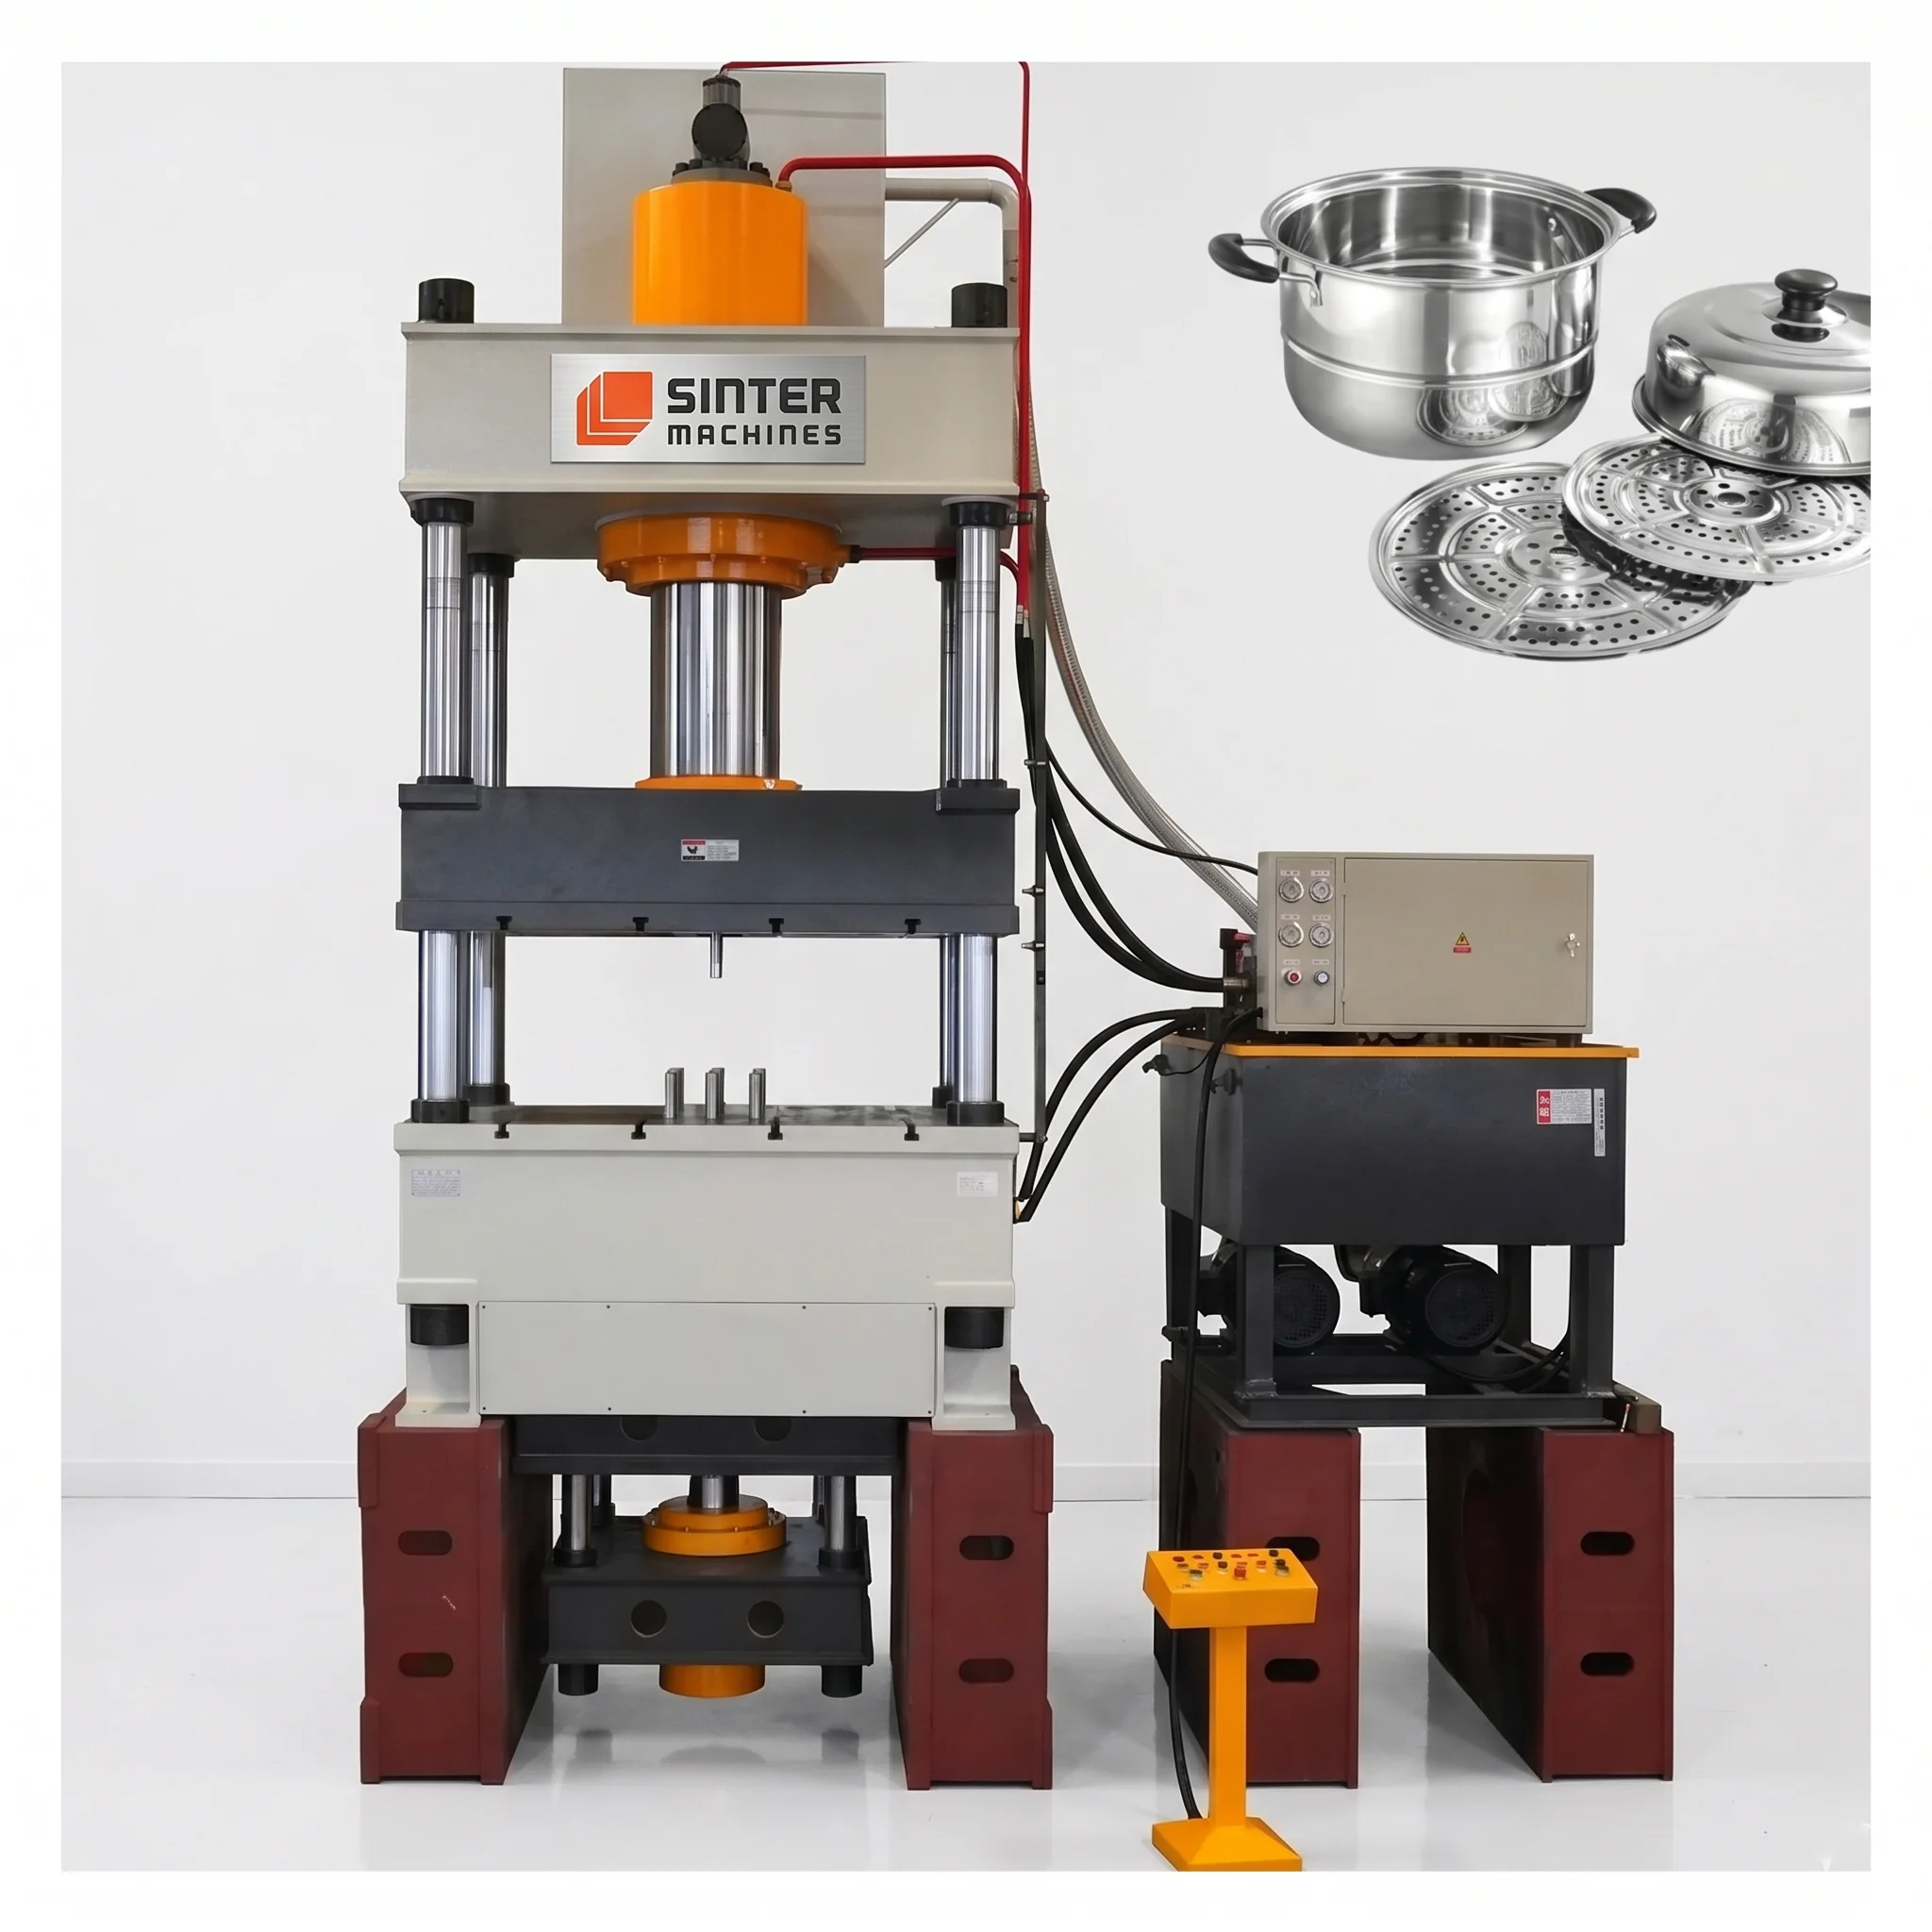
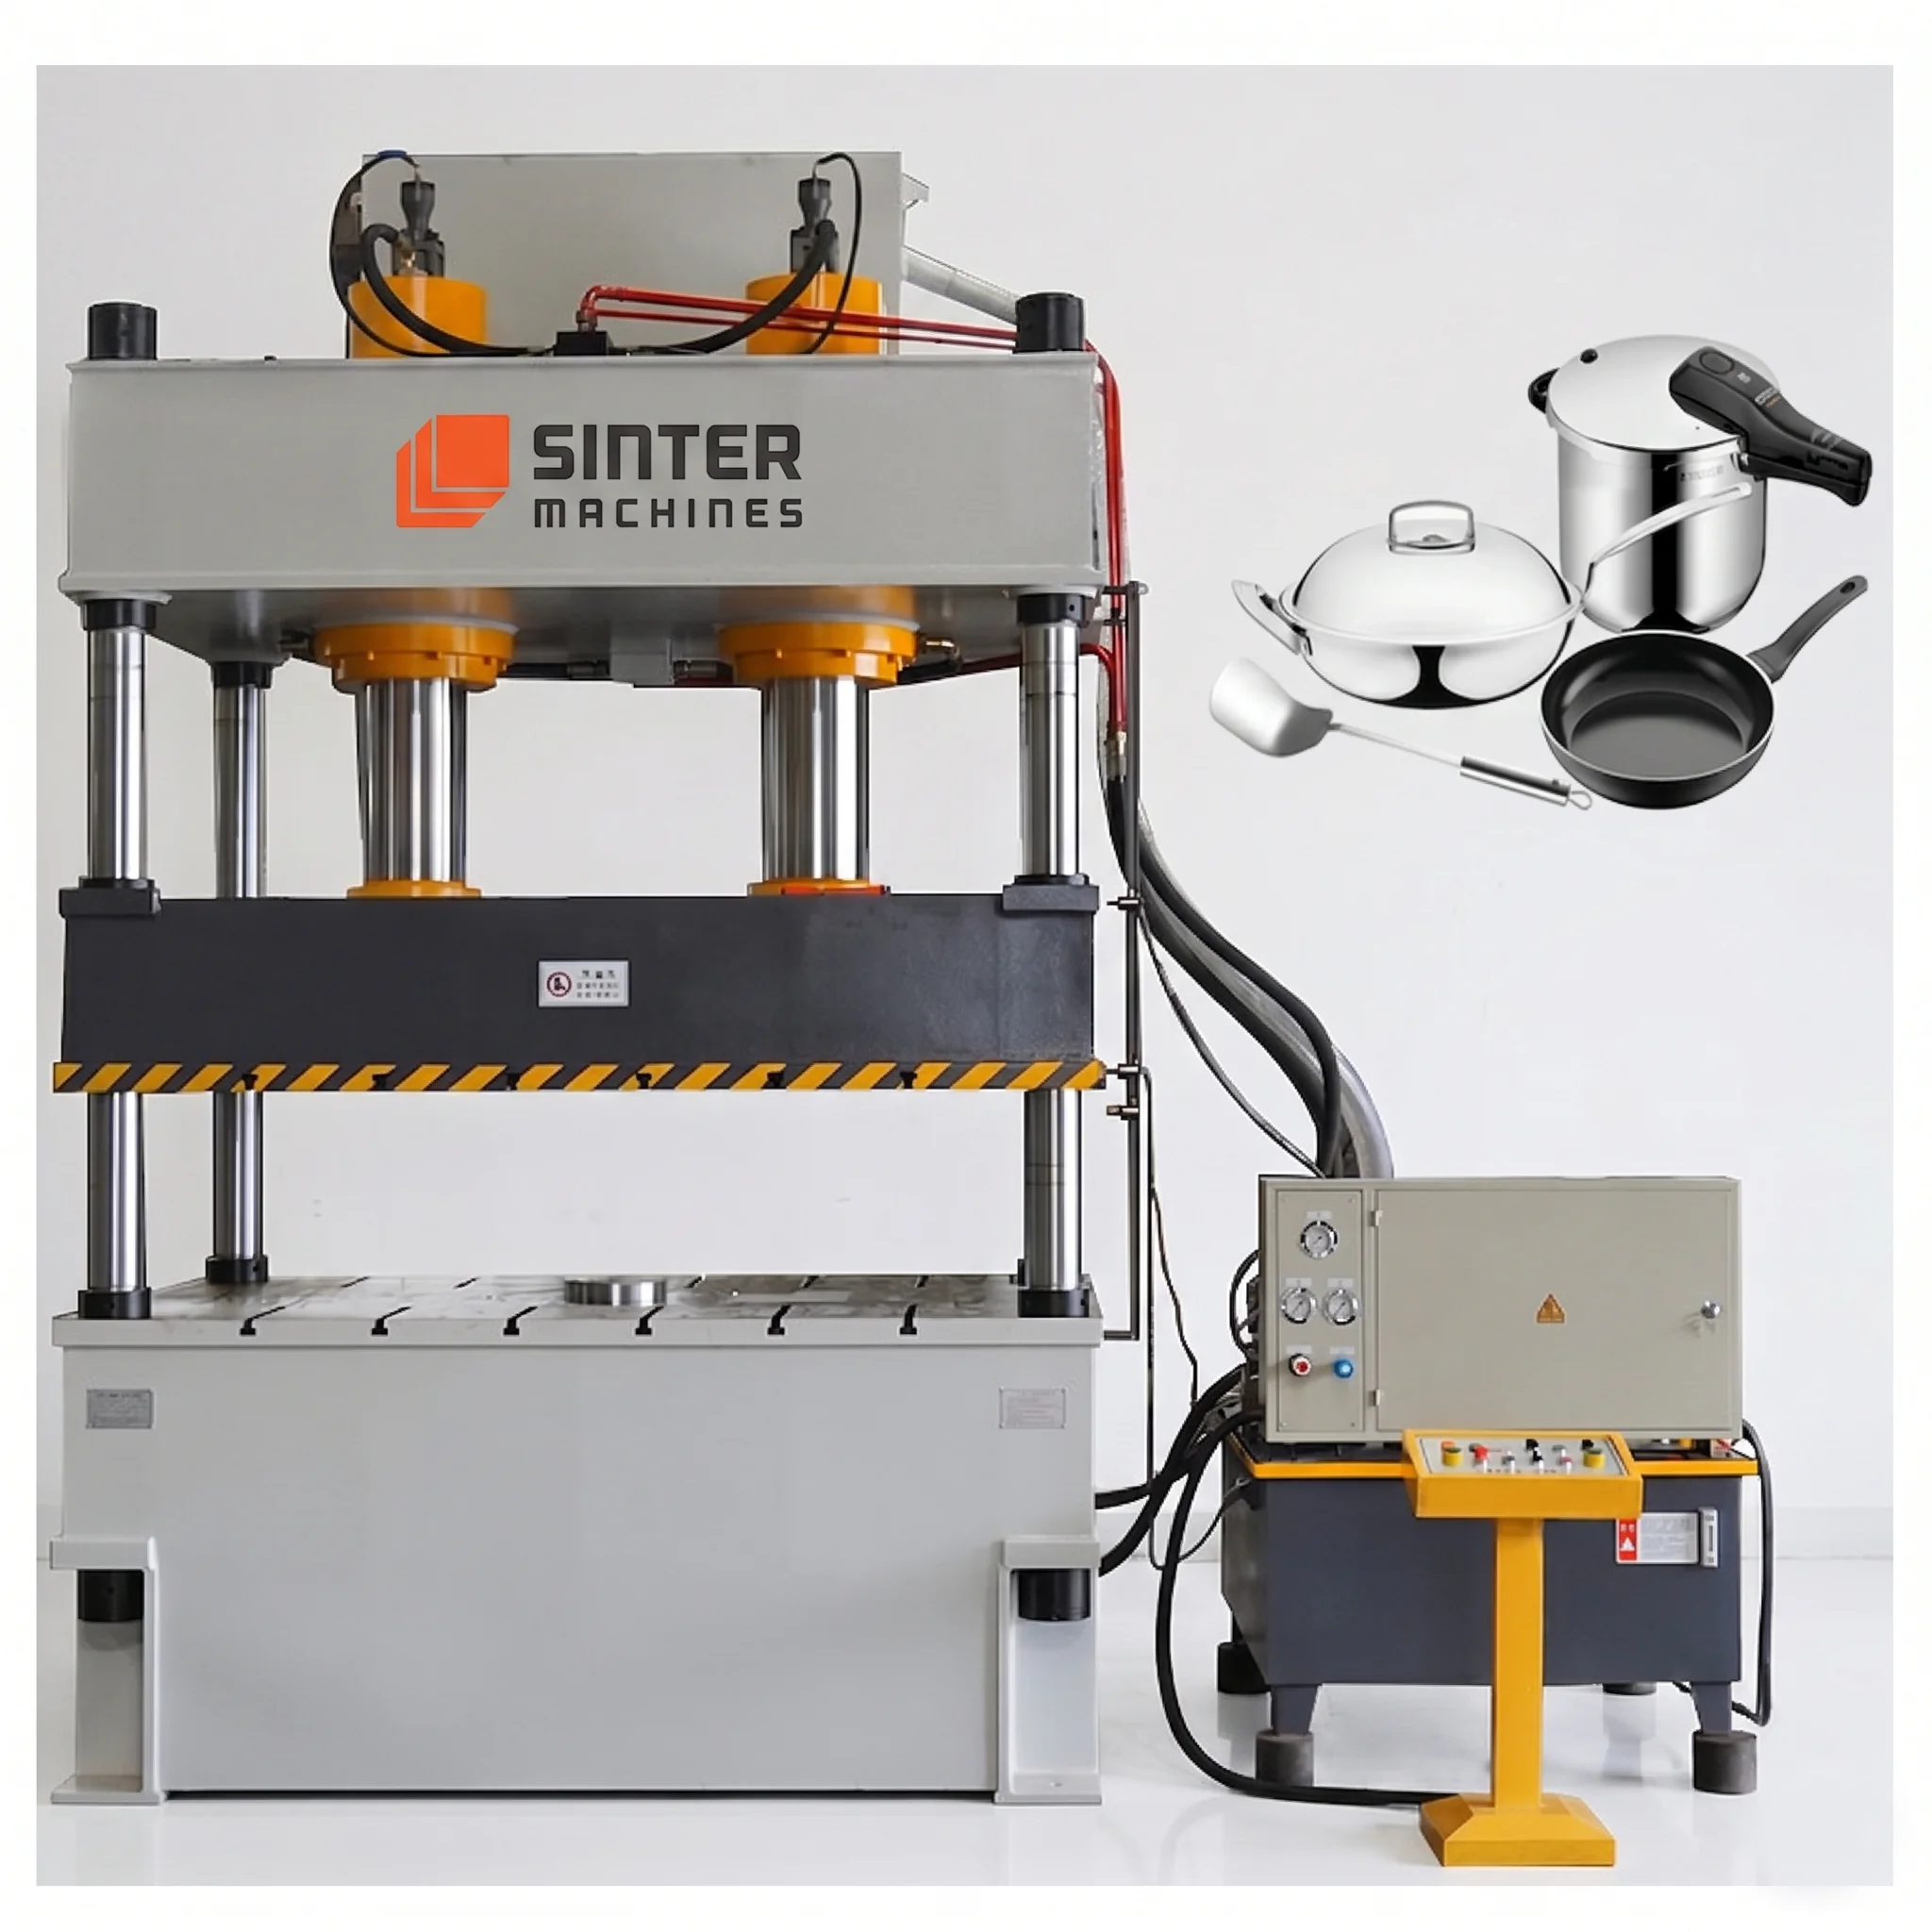
500T Four Column Hydraulic Press for Deep Drawing SS Food Containers

500T Rated Capacity
150 mm/s Slider Down Speed
10–18 mm/s Slider Pressing Speed
180 mm/s Slider Return Speed

01 — Press System

500T Four Column Hydraulic Press Machine

The 500-ton four-pillar hydraulic press provides high force with precise control for defect-free deep drawing of stainless steel components. It delivers high productivity, repeatable quality, and long service life in continuous packaging plants.

Use Case

Engineered to manufacture hygienic, food-grade containers, this system supports multi-stage draw and redraw processes. It ensures uniform wall thickness, crack-free draws, and excellent surface finishes for high-volume beverage and food packaging.

Core Applications

  • Deep Drawing Operations: Severe plastic deformation processing to turn flat stainless steel circular blanks into deep cylindrical shells.
  • Food & Beverage Packaging: High-volume production lines focused on sanitary, pressure-resistant, and structural metal containers.

Material

  • Stainless Steel: Processes austenitic stainless steel grades (such as 304 and 316) known for high work-hardening rates and corrosion resistance.
  • Food-Grade Stocks: Handles specialized mirror-finish or BA (Bright Annealed) sheets without degrading their sanitary properties.

Typical Products Formed

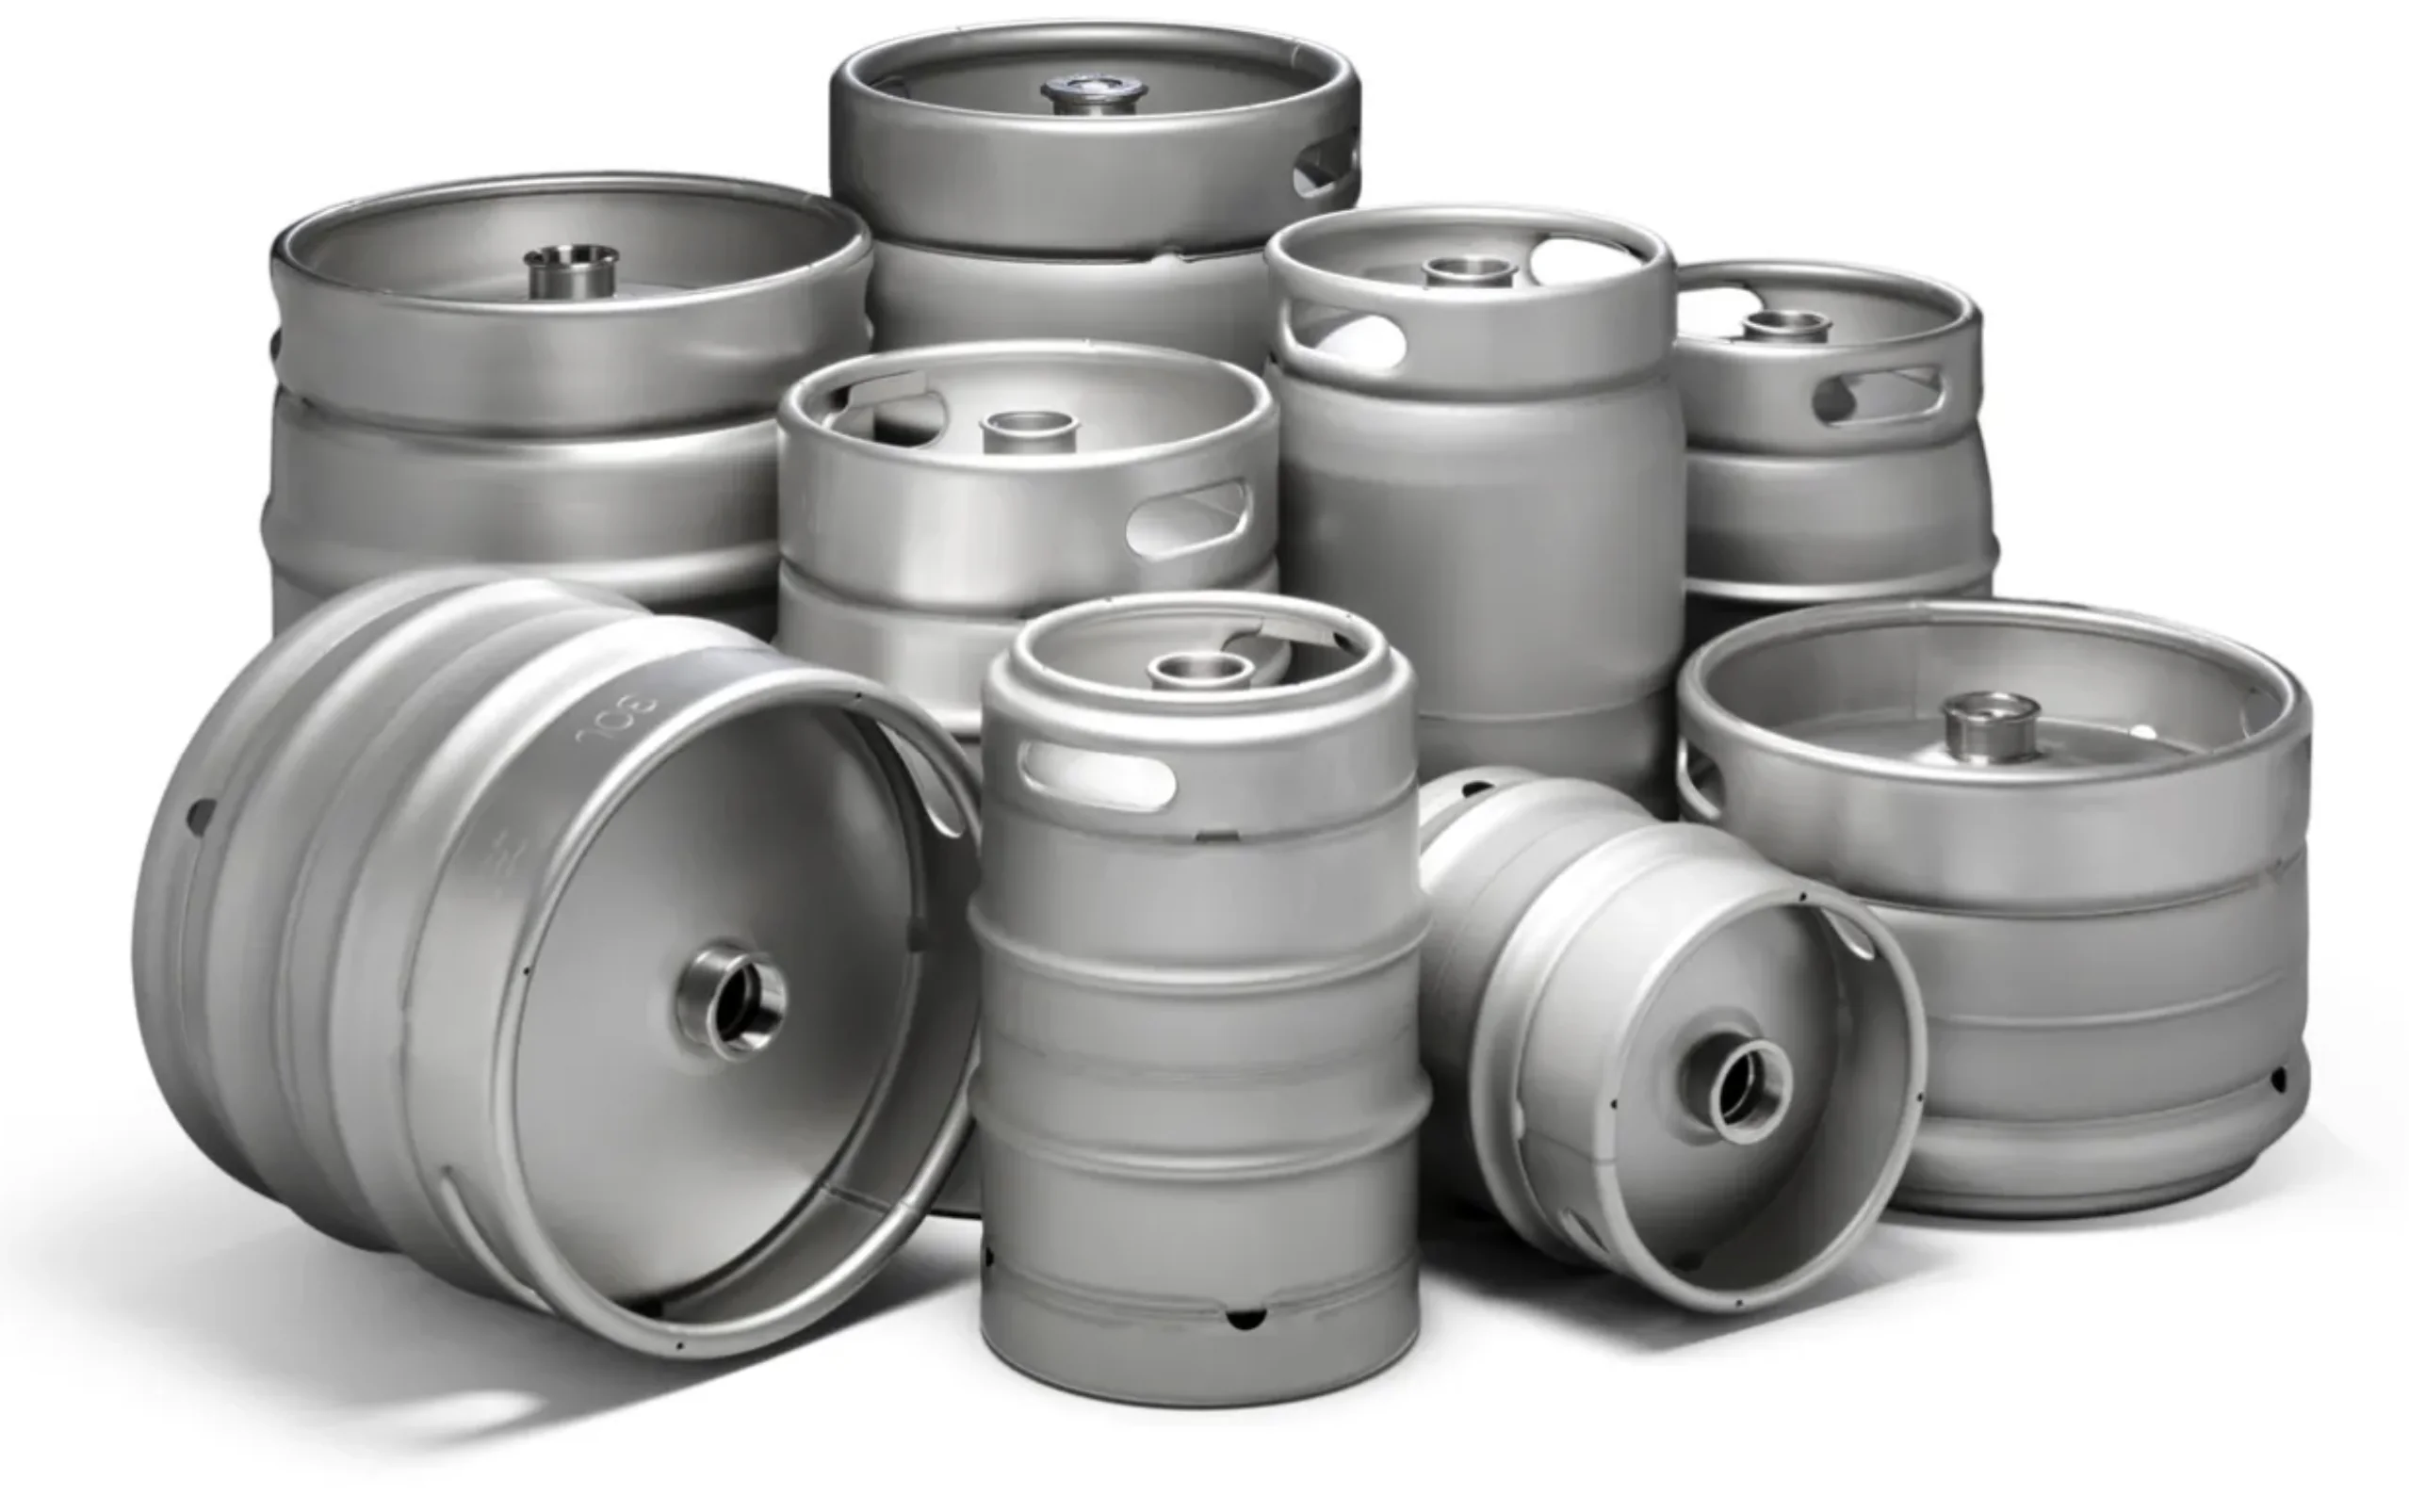
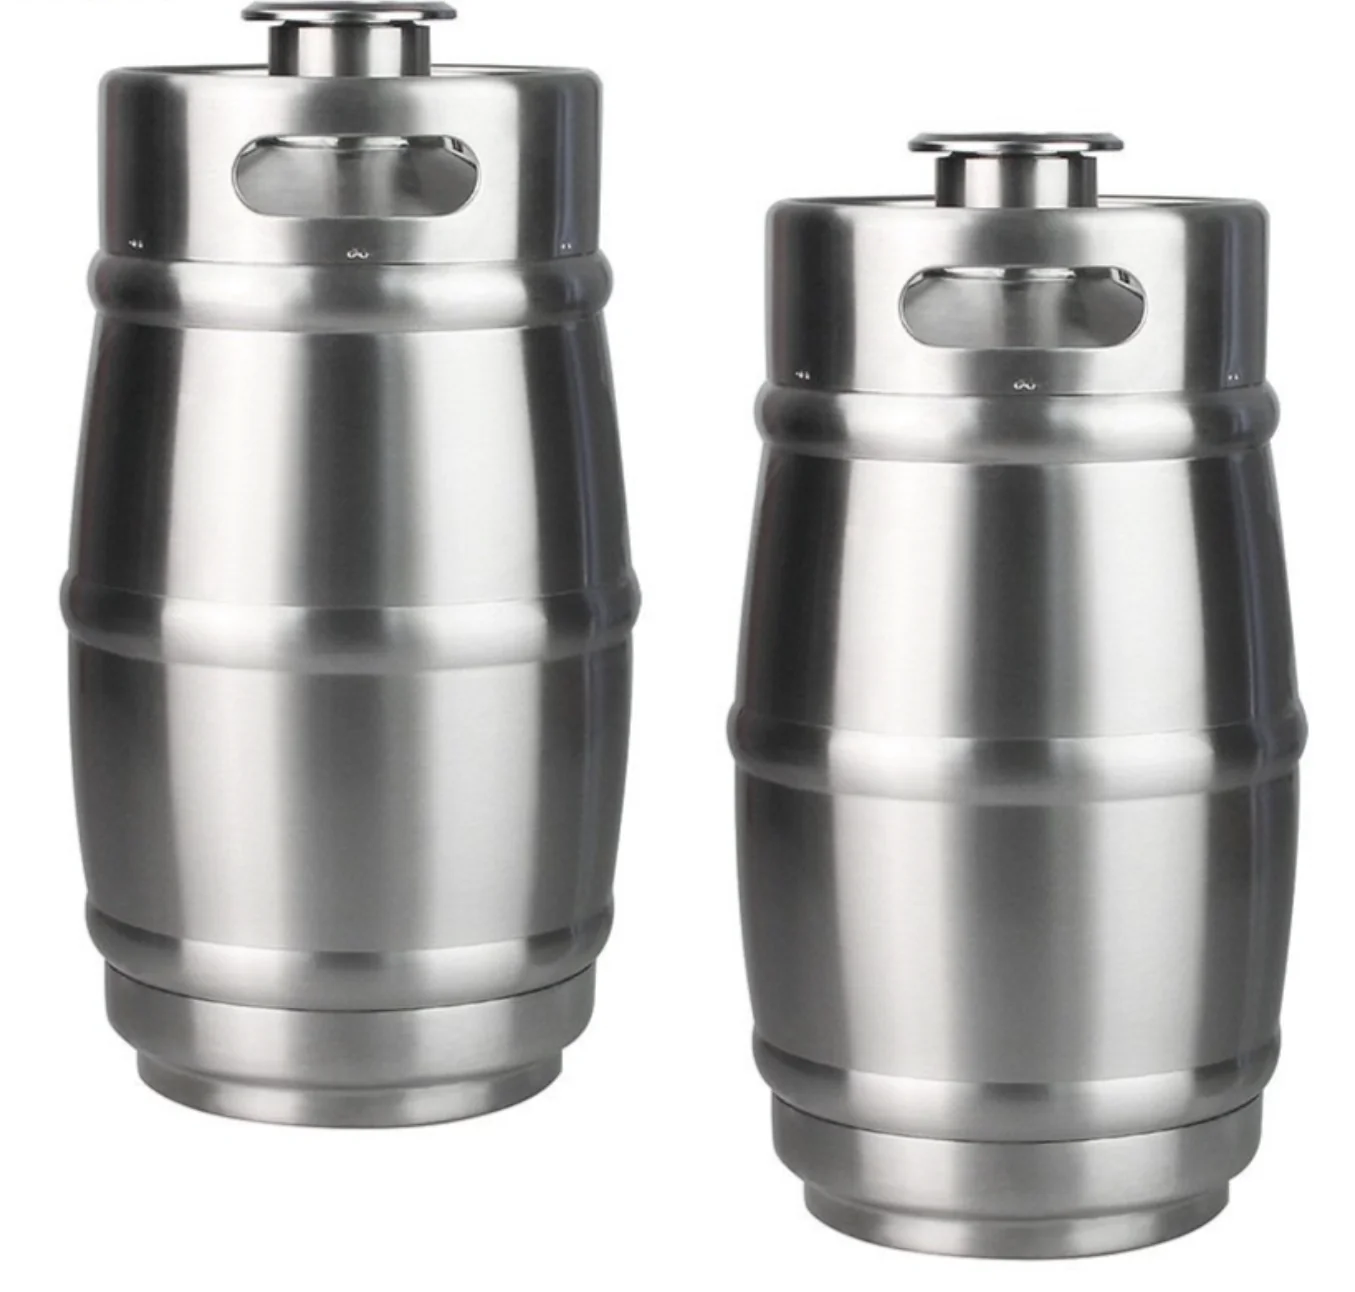
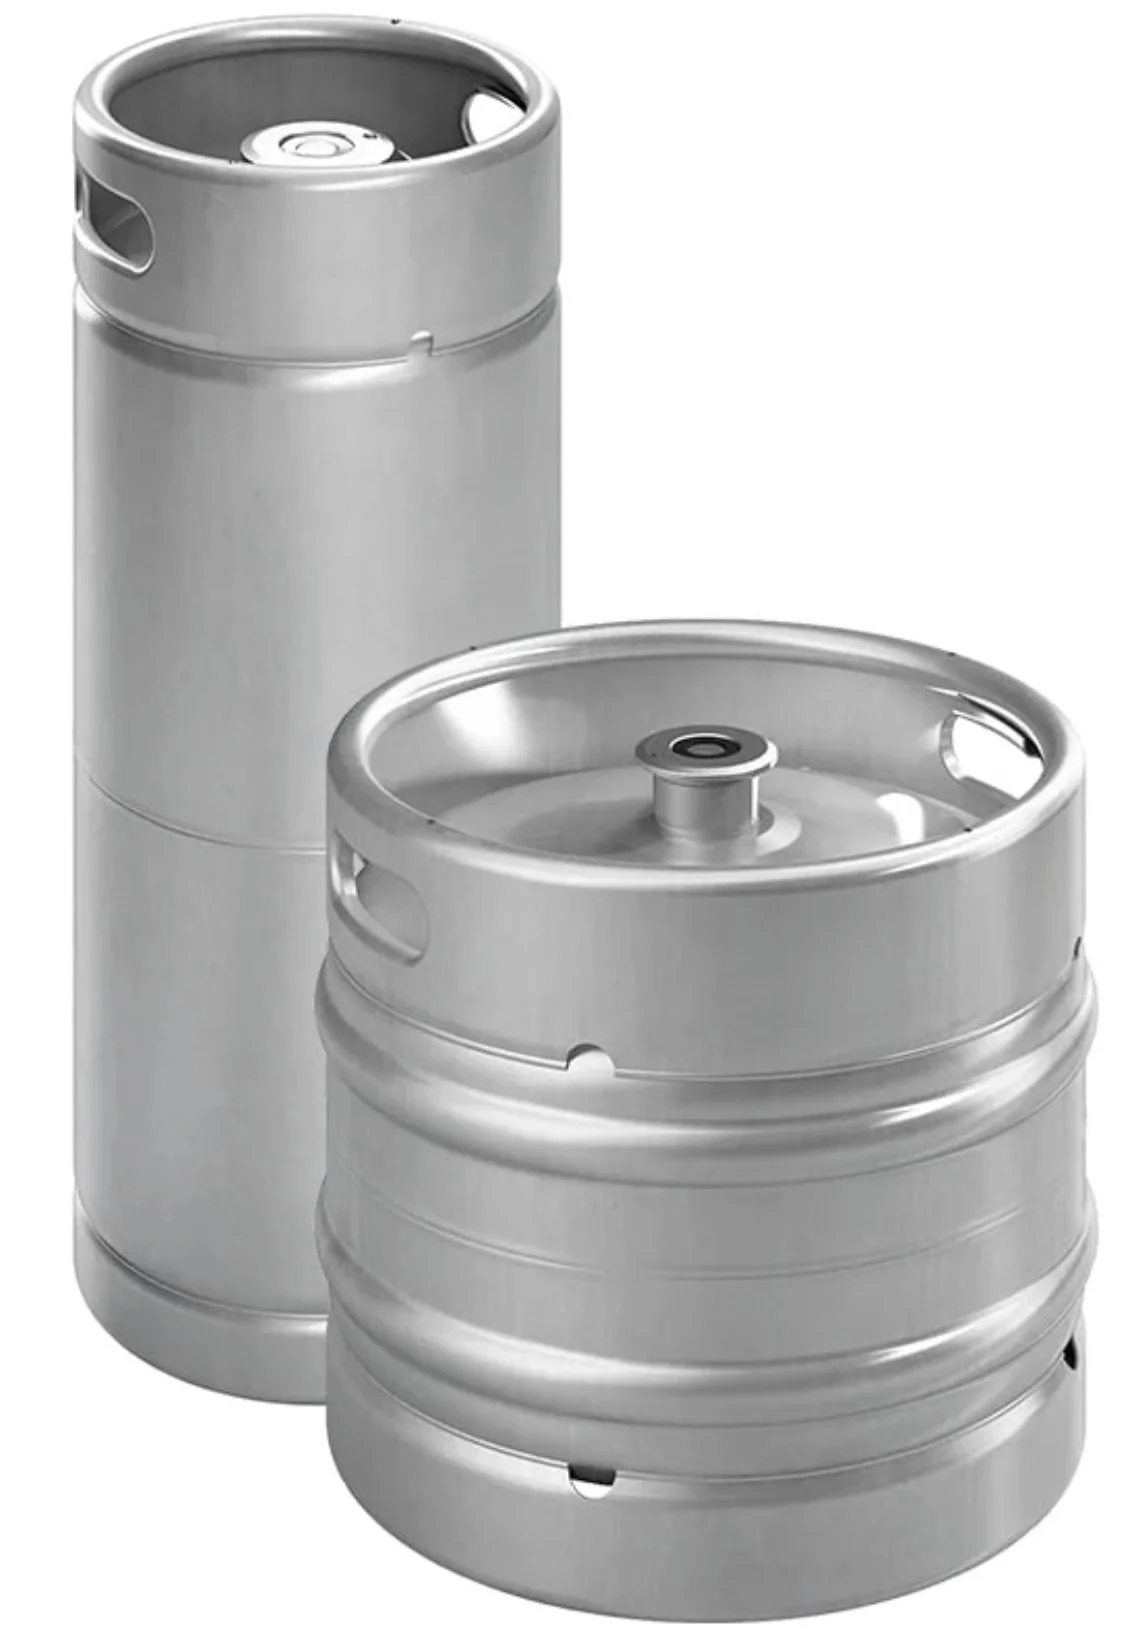
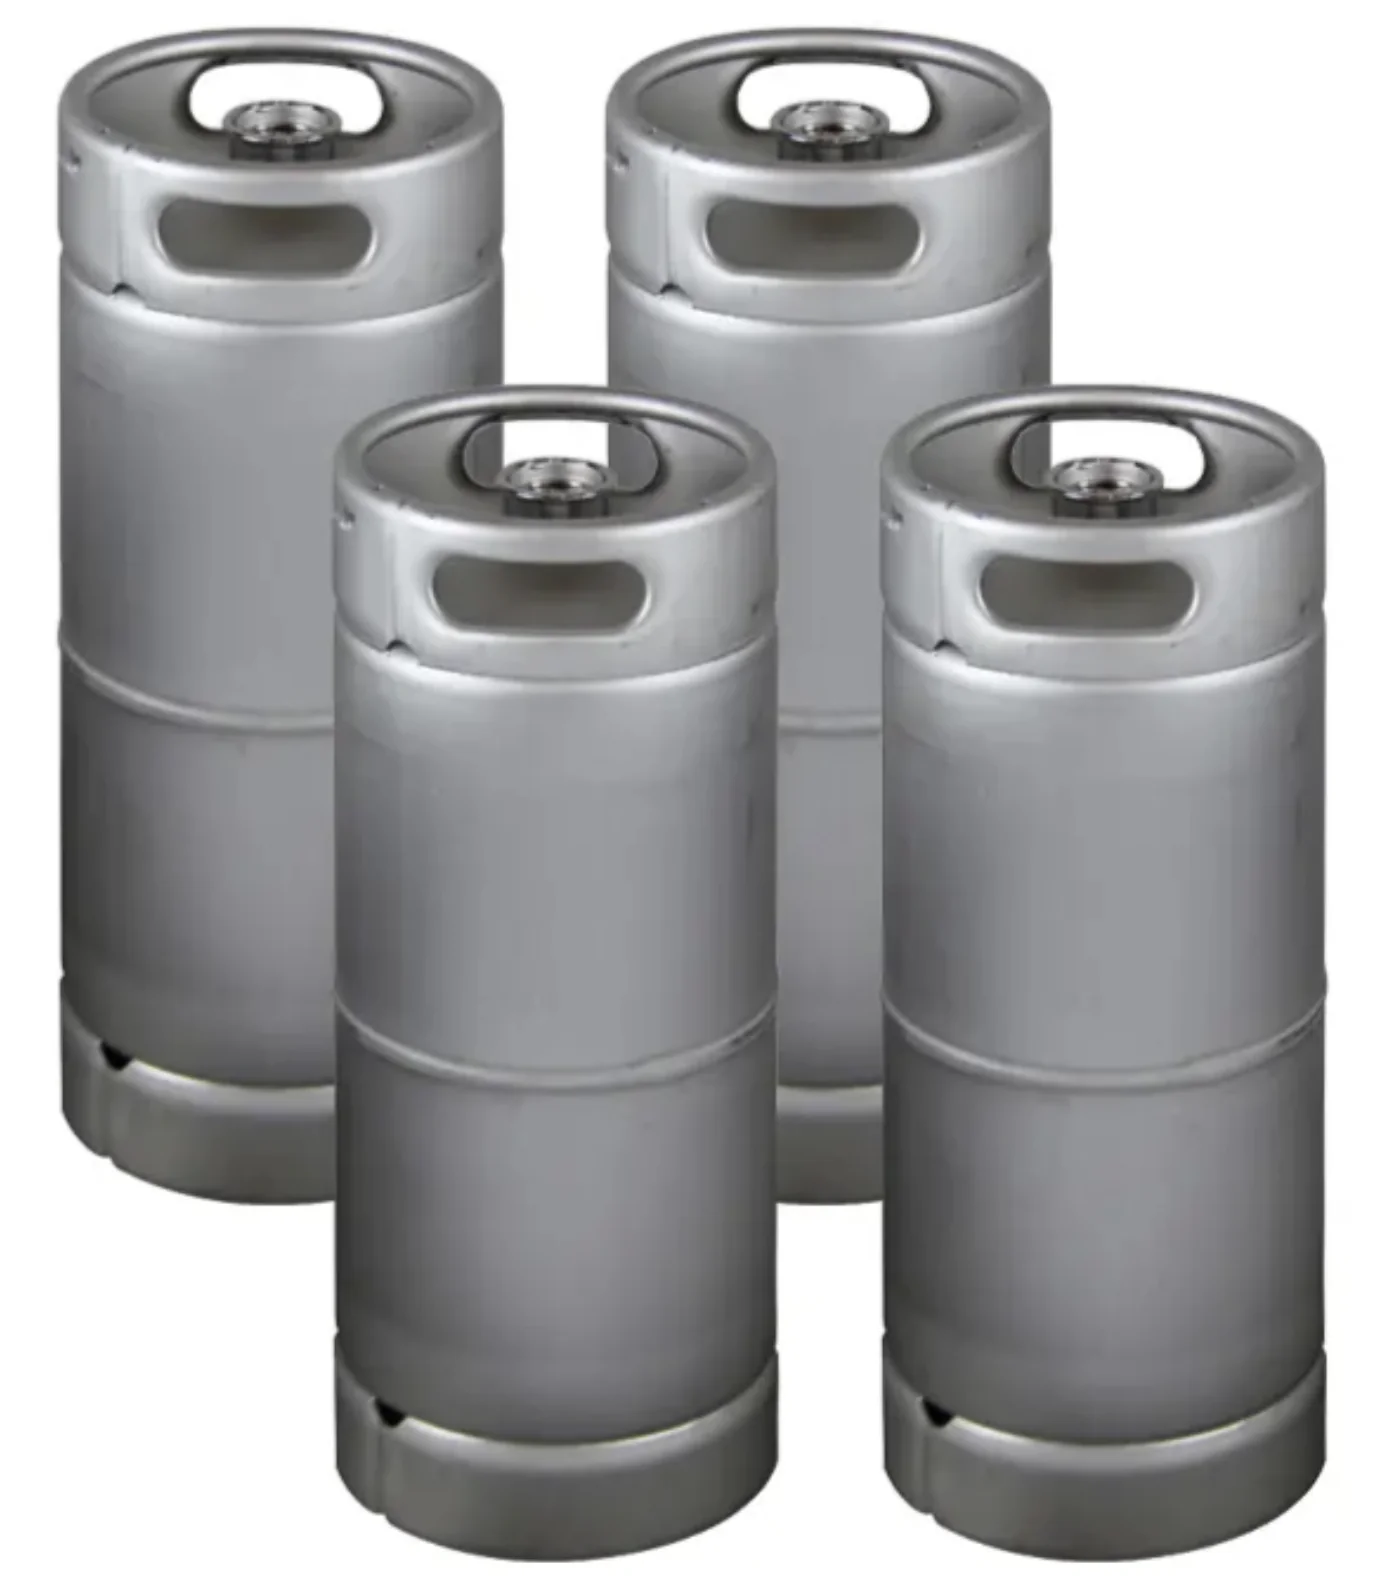
  • Beverage Containers: Beer keg halves, keg domes, chine rings, and high-pressure commercial beverage canisters.
  • Food Processing Hardware: Deep-drawn food cans, institutional storage containers, lids, caps, and industrial pot preforms.

Key Functions

  • Controlled Blank Holding: Employs an active hydraulic cushion to apply precise blank holder pressure, preventing wrinkles during the draw.
  • Multi-Stage Redrawing: Executes subsequent drawing, reduction, and ironing phases to achieve high depth-to-diameter ratios.

Why 500-Ton Hydraulic Press?

  • High Force Capacity: Overcomes the significant flow stress and work-hardening traits inherent to stainless steel during deep draws.
  • Rigid Four-Pillar Guidance: Guarantees absolute concentricity between the punch and die, preventing uneven wall thinning or side-wall tearing.

02 — Technical Specifications

SM 500 HP – HYDRAULIC PRESS MACHINE COMPLETE TECHNICAL DATA

This heavy-duty 500-ton hydraulic press is engineered with a high-rigidity four-pillar structure optimized for severe stainless steel deep drawing. It incorporates an advanced hydraulic cushion and precise speed profiles to deliver defect-free, food-grade containers with uniform wall thickness.

Complete Technical Data

Capacity

  • Nominal Force: 500 Tons (5000kN) of primary downward ram force to overcome the high tensile strength and work-hardening of stainless steel.
  • Hydraulic Cushion Force: 200–250 Tons of adjustable blank-holder force to precisely regulate material flow and prevent wrinkling during deep draws.

Structural Design

  • Heavy-Duty Four-Pillar Architecture: Utilizes four ultra-rigid, precision-ground columns to maintain perfect parallelism between the upper punch and lower die.
  • Extended Guide Bushings: Long, self-lubricating slider guides counteract severe off-center forces generated during asymmetrical drawing phases.

Frame Type

  • Four-Column Open Style: Provides unrestricted 360-degree visual and physical access to the die workspace, streamlining manual setups and robotic automation.
  • Finite Element Analysis (FEA) Optimized Frame: Heavy steel plates are welded, stress-relieved, and machined to ensure negligible structural deflection under full tonnage.

Hydraulic System

  • High-Pressure Servo-Driven Hydraulics: Integrates high-efficiency variable displacement pumps paired with servo motors for energy savings and highly responsive pressure adjustments.
  • Dedicated Cushion Circuit: Separate independent hydraulic loop controls the blank holder cushion to maintain stable pressure profiles throughout the entire stroke.

Main Ram Stroke

  • Maximum Travel: Long stroke capability (typically 800mm–1000mm) designed specifically to accommodate tall cylindrical containers and deep-drawn keg preforms.
  • Digital Stroke Control: Employs high-resolution linear scales providing 0.05 mm position tracking for precise bottom dead center (BDC) repeatability.

Working Hydraulic Pressure

  • Max Operating Pressure: Rated at a robust 25–31.5 MPa (250-315 bar) to generate massive forming forces within a compact cylinder footprint.
  • Closed-Loop Pressure Regulation: Proportional pressure transducers continuously adjust system pressure via the main PLC controller.

Daylight Gap

  • Maximum Open Height: Large vertical clearance (typically 1200mm–1500mm) providing the required space for deep drawing punches, blank holders, and deep part extraction.
  • Minimum Shut Height: Configured to match standard multi-stage deep drawing and ironing mold dimensions.

Approach Speed

  • Fast Downward Velocity: Rapid approach speed up to 150–200 mm/s to dramatically minimize non-productive open cycle times.
  • Proportional Deceleration: Smooth, automated deceleration curves right before punch-to-blank contact to eliminate material impact shock.

Pressing / Drawing Speed

  • Multi-Stage Drawing Velocity: Micro-adjustable range (typically 4–12 mm/s) engineered to match the plastic flow limits of stainless steel.
  • Constant Variable Flow Control: Maintains steady tonnage delivery at precise speeds to prevent localized thinning, tearing, or necking.

Return Speed

  • Fast Retraction Velocity: High-speed upward stroke (up to 120–160 mm/s) to quickly clear the working envelope for part extraction.
  • Pre-Return Decompression: Programmable decompression control dampens the release of high-pressure oil, protecting valves and pipes from hydraulic shock.

Bed / Platen Size

  • Bolster Dimensions: Large working table area (e.g., $1400\text{mm} \times 1200\text{mm}$) sized perfectly for multi-stage progressive drawing or concentric circular dies.
  • Machined Concentric Rings & T-Slots: Features precise T-slots and center bore options for seamless integration and alignment of lower cushion pins.

Columns

  • Pillar Construction: High-alloy forged steel columns, induction-hardened and coated with hard chrome for a wear-resistant, low-friction surface.
  • Threaded Locking Nuts: Heavy-duty tie-rod style pre-stressed locking nuts ensure the frame remains geometrically square over decades of continuous operation.

Working Envelope

  • Clearance Dimensions: Maximized spacing between pillars to easily accommodate automated pick-and-place blank feeders and finished container extractors.
  • Optimized Ergonomics: Lower bolster height configured for smooth conveyor-line integration, allowing clean inline parts transport.

Control System

  • Advanced PLC Integration: Industrial-grade central processing unit (e.g., Siemens S7-1500) executing real-time logic control for all hydraulic actions.
  • Intelligent HMI Display: Multi-touch screen interface featuring pressure/stroke curve graphing, storage for hundreds of die recipes, and advanced fault diagnostics.

Main Motor Power

  • High-Capacity Power Pack: Driven by high-efficiency dual or triple motor setups (typically totaling 45kW–75kW) optimized for heavy continuous operation.
  • Energy-Saving Servo Setup: Power consumption scales dynamically with the demand of the cycle stage, reducing electricity usage up to 30–50% during idle times.

Valves & Hydraulics

  • Logic Cartridge Block Manifolds: Manifold blocks minimize pipe connections, significantly lowering the risk of oil leaks while ensuring instantaneous valve response.
  • Premium Global Brands: Utilizes top-tier valves (such as Rexroth, Vickers, or Parker) to guarantee long-term component availability and reliable sealing.

Automation

  • Robot & Destacker Ready: Pre-installed Profinet/Ethernet communication interfaces for seamless integration with blank destackers and robotic transfer arms.
  • Pneumatic Part Ejectors: Auxiliary air blast and mechanical stripping control circuits integrated directly into the press cycle logic.

Safety Features

  • Type 4 Safety Light Curtains: Dual-sided light barriers guard the loading area, instantly halting all machine movements if the perimeter is breached.
  • Dual-Channel Interlocking Valves: Redundant hydraulic safety valves prevent unauthorized ram descent in the event of an electrical failure.
  • Anti-Drop Mechanical Lock: Features a robust locking bar or slide safety catcher that mechanically blocks the main slide from descending during maintenance.

SM 500 HP — Model Specifications

  • Nominal Force: 5000 KN
  • Maximum Hydraulic Pressure: 25 MPa
  • Max Opening Height of the Slider: 1500 mm
  • Max Stroke of the Slider: 900 mm
  • Effective Bed Size: 1400 × 1400 mm
  • Slider Down Speed: 150 mm/s
  • Slider Pressing Speed: 10–18 mm/s
  • Slider Return Speed: 180 mm/s
  • Ejector Cylinder Nominal Force: 500 KN
  • Stroke of the Ejection Cylinder: 300 mm
Production Case Study

Deep Drawing SS Food Containers Production Line

200 – 600 mmBlank diameter
0.8mm -2.0mmBlank thickness
15 to 25 SecCycle time
±0.05–0.10 mmForming accuracy
High structural durability
Zero wall cracking
Uniform wall thickness
Flawless surface finish
High production throughput
Low scrap rates
Minimum post-process polishing

03 — Die / Mold System

Precision Deep Drawing SS Food Containers Die Mold Engineering

This high-performance tooling system is engineered for severe plastic deformation of stainless steel blanks into deep-drawn food containers. It utilizes robust, high-wear alloys and active binder controls to deliver structurally sound, crack-free cylindrical forms.

Use Case

Specifically paired with 500-ton hydraulic presses, this mold handles multi-stage draw and redraw sequences for beverage kegs, food cans, and sanitary vessels. It maintains precise material flow to prevent wrinkling and wall-thinning while protecting the mirror-like surface of food-grade alloys.

Technical Specifications (Tooling)

Die Type

  • Multi-Stage Deep Drawing Dies: Set up as single-action draw dies, double-action redraw dies, or progressive deep draw tooling.
  • Integrated Ironing & Sizing Dies: Compresses side walls to uniform thicknesses while sizing final container diameters.

Die Materials

  • Punch and Die Rings: Machined from premium D2, DC53, or tungsten carbide inserts in high-wear zones to combat the abrasive nature of stainless steel.
  • Die Shoes and Bolsters: Made of heavy-duty carbon steel (45 or structural steel) to absorb massive compressive impacts without flexing.

Tool Configuration & Construction

  • High-Pressure Nitrogen Cylinder Plates: Built-in nitrogen gas spring manifolds apply constant, adjustable blank holder pressure.
  • Draw Bead Integration: Custom-profiled draw beads are integrated to precisely retard and manage metal flow into the cavity.

Key Tooling Features

  • Vented Punches: Air escape channels drilled directly through the draw punch to prevent vacuum formation during part stripping.
  • Replaceable Insert Assembly: Allows rapid replacement of draw rings and punch noses without rebuilding the entire mold block.

Alignment Accuracy

  • Ball Guide Post Sets: High-tolerance guide pillars and ball cages guarantee punch-and-die alignment within 0.01mm
  • Concentricity Tolerances: Extreme concentricity limits prevent uneven wall thinning and catastrophic material tearing.

Materials Formed

  • Austenitic Stainless Steel: Specially designed to form high-tensile 304, 304L, 316, and 316L grades.
  • Sheet Thickness Range: Optimized for heavy-duty metal blanks ranging in thickness from 0.8 mm to 2.0 mm.

Surface Finish

  • Mirror-Polished Working Components: Punch noses and draw rings are polished to a mirror finish
  • Advanced Friction Coatings: Enhanced with PVD, CVD, or TD (Thermal Diffusion) treatments to eliminate friction galling and metal pick-up.

Tool Life

  • Regrinding/Polishing Interval: Drawing radii require repolishing every 50,000 to 80,000 cycles to remove localized stainless steel deposits.
  • Total Lifespan: Designed to deliver 800,000 to 1,500,000 total production cycles under standard maintenance and lubrication protocols.
Case Study (Die Performance)

Precision Deep Drawing SS Food Containers Die Mold

D2 / DC53Die Material
HRC 60–64Hardness
TD or PVD (TiAlN)Surface Treatment
Zero side-wall galling
Uniform container thickness
Elimination of cracking
Exceptional surface finish
Extended tooling longevity
Minimal downtime maintenance
Reduced scrap volume

04 — Product Application

Where Precision Deep Drawing SS Food Containers Are Used

These high-precision, deep-drawn containers are engineered to meet strict hygiene, durability, and corrosion-resistance standards. They serve as the primary packaging and storage vessels across demanding food, beverage, and medical industries.

Industry Applications

Beverage Packaging & Kegs

Deep-drawn halves are welded together to produce heavy-duty beer kegs, beverage canisters, and carbonated drink containers. The seamless, uniform walls withstand high internal pressures while preserving the flavor and carbonation of the liquid.

Commercial Kitchenware & Food Processing

Used to manufacture institutional food pans, prep bowls, industrial stock pots, and bulk food storage containers. The smooth, non-porous stainless steel surface prevents bacterial growth and stands up to harsh, high-temperature sanitization cycles.

Canning & Preserved Food Storage

Utilized for high-end, reusable food cans, airtight storage canisters, and specialty metal packaging for premium goods. These containers offer an impermeable barrier to light, oxygen, and moisture, significantly extending product shelf life.

Sanitary & Pharmaceutical Vessels

Applied in the medical and pharmaceutical sectors as sterile laboratory trays, surgical containers, and chemical-grade storage tins. Their high-alloy stainless steel composition ensures no chemical leaching occurs, maintaining strict product purity.

Finished Product Gallery

05 — Key Advantages

Why Choose the 500-Ton Sinter Hydraulic Press

This heavy-duty press combines massive forming power with an active, highly responsive blank-holding hydraulic cushion. It delivers the precise control necessary to deep-draw stainless steel without tearing, work-hardening failures, or surface cosmetic damage.

Technical & Commercial Benefits

01

Massive Power with Low Structural Deflection

The robust 500-ton four-column frame distributes massive tonnage evenly across the tooling setup. This extreme structural rigidity prevents off-center deflection, keeping the punch perfectly concentric to eliminate uneven wall thinning.

02

Active Hydraulic Cushion Force Control

Featuring an independent 200–250 ton programmable hydraulic cushion, the press manages blank holder pressure in real-time. This dynamic pressure regulation allows material to flow smoothly into the die, eliminating wrinkles and tearing.

03

Advanced Servo-Driven Energy Efficiency

The integrated servo-hydraulic pump system automatically scales power output to match the precise demands of each drawing phase. This reduces overall electricity consumption by up to 30–50% during non-pressing and idle cycles.

04

Optimized Multi-Stage Drawing Capabilities

With an extra-large daylight gap and a long ram stroke, this press easily accommodates tall, multi-stage progressive drawing molds. This high-capacity envelope enables operators to execute draw, redraw, and ironing steps in a single workspace.

05

Programmable Speed and Flow Profiles

The closed-loop control system allows operators to program precise micro-adjustments for the fast approach, drawing, and return speeds. This gentle, uniform material drawing speed prevents cracking in high-tensile, work-hardening stainless steel.

06

Sub-Millimeter Stroke and Repeatable Accuracy

Equipped with high-resolution digital linear encoders, the machine maintains highly repeatable stroke limits within $\pm0.05\text{mm}$. This ultra-consistent positioning ensures identical wall heights, uniform thicknesses, and rapid downstream automation integration.